Leave Your Message
Explore our top-tier worm gearboxes engineered specifically for the rigorous demands of modern conveyor systems and bulk material handling applications.
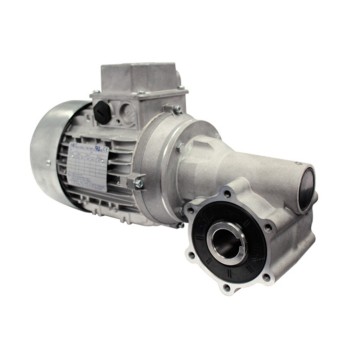
In the rapidly evolving landscape of industrial automation, the efficiency of material handling and conveyor systems dictates the overall productivity of manufacturing plants, distribution centers, and mining operations. At the heart of these intricate networks lies the worm gearbox—a mechanical marvel designed to provide high torque, significant speed reduction, and a compact right-angle configuration. Worm gearbox manufacturers for conveyor systems and material handling are continuously pushing the boundaries of mechanical engineering to deliver power transmission solutions that are not only robust but also highly efficient and exceptionally reliable.
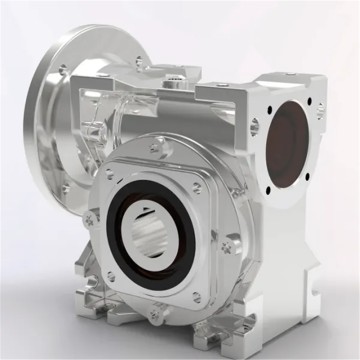
The fundamental design of a worm gearbox—comprising a worm (screw) that meshes with a worm wheel (gear)—offers unique advantages that make it indispensable for conveyor applications. Chief among these is the inherent self-locking capability found in high-ratio worm gears. In inclined conveyor systems or vertical lifting mechanisms, this self-locking feature prevents back-driving when the motor is turned off, acting as a secondary safety mechanism that prevents heavy loads from reversing uncontrollably. Furthermore, the 90-degree alignment of the input and output shafts allows for a highly compact installation footprint, which is crucial in densely packed automated warehouses and intricate assembly lines where space is at a premium.
The global market for material handling equipment is experiencing unprecedented growth, driven primarily by the explosive expansion of e-commerce, the modernization of global supply chains, and the relentless push towards Industry 4.0. As mega-retailers and logistics giants construct massive, highly automated fulfillment centers, the demand for reliable conveyor components has skyrocketed. Consequently, worm gearbox manufacturers are finding themselves at the nexus of a massive industrial boom.
However, this surge in demand brings its own set of commercial challenges and competitive dynamics. Manufacturers are under immense pressure to optimize the Total Cost of Ownership (TCO) for their clients. This means that modern gearboxes must not only be affordable to procure but must also demonstrate exceptional longevity, require minimal maintenance, and operate with high energy efficiency. The industry is witnessing a distinct shift from commoditized, off-the-shelf gearboxes to highly customized, application-specific power transmission solutions. Original Equipment Manufacturers (OEMs) of conveyor systems are increasingly collaborating directly with gearbox manufacturers to co-develop units that perfectly match the torque profiles, environmental conditions, and spatial constraints of their specific material handling systems.
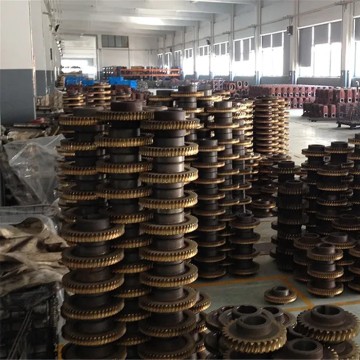
Supply chain resilience has also become a paramount concern in the commercial landscape. Leading worm gearbox manufacturers are vertically integrating their production processes—bringing casting, precision machining, gear grinding, and assembly under one roof. This integration ensures stringent quality control and mitigates the risks associated with global supply chain disruptions, allowing manufacturers to guarantee reliable lead times for critical industrial projects.
The versatility of the worm gearbox allows it to be deployed across a vast array of material handling environments. Understanding the nuanced demands of these specific applications is crucial for both manufacturers and end-users when selecting the appropriate power transmission components.
In modern fulfillment centers, roller conveyors and belt conveyors form a massive, high-speed arterial network that sorts and transports millions of parcels daily. Gearboxes in this environment are subjected to continuous, high-frequency stop-and-go operations. Worm gearboxes are favored here due to their smooth, quiet operation—a critical factor in maintaining a safe and comfortable acoustic environment for warehouse workers. Manufacturers optimize these gearboxes with low-backlash designs and synthetic lubricants to handle the rapid acceleration and deceleration profiles dictated by automated sorting algorithms without suffering premature wear.
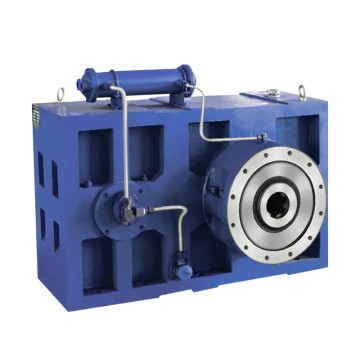
Transporting raw ores, coal, or aggregates requires heavy-duty belt conveyors that span kilometers across unforgiving terrains. The worm gearboxes driving these massive systems must endure extreme operational stresses, including heavy shock loads, pervasive abrasive dust, and wide temperature fluctuations. Manufacturers address these challenges by constructing gearboxes with ruggedized cast-iron housings, oversized bearings, and advanced multi-lip sealing systems that prevent the ingress of contaminants. High thermal capacity is also engineered into these units to dissipate the immense heat generated during continuous, high-torque operation.
Hygiene and cleanliness are the absolute priorities in the food and beverage and pharmaceutical industries. Conveyor systems in these sectors are subjected to rigorous daily washdown regimens using high-pressure water and caustic cleaning chemicals. Worm gearbox manufacturers cater to this specific niche by offering stainless steel gearboxes (such as the SSRV series) that feature smooth, crevice-free housings to prevent bacterial growth. These specialized units are sealed to IP69K standards and are factory-filled with FDA-approved food-grade lubricants, ensuring absolute safety and compliance with global hygiene regulations.
In automotive manufacturing, overhead chain conveyors and heavy-duty skid conveyors move vehicle chassis through various stages of assembly, welding, and painting. The gearboxes driving these systems must offer impeccable reliability, as a single failure can halt the entire production line, costing thousands of dollars per minute. Manufacturers supply highly engineered worm gearboxes equipped with specialized mounting flanges, reinforced output shafts, and integrated torque-limiting clutches to protect the drivetrain from unexpected jams or overloads.
The field of mechanical power transmission is not stagnant; it is undergoing a technological renaissance. Worm gearbox manufacturers for conveyor systems and material handling are aggressively investing in Research and Development to address the modern industrial demands of efficiency, connectivity, and sustainability.
Traditionally purely mechanical devices, worm gearboxes are now being transformed into smart, connected nodes within the Industrial Internet of Things (IIoT) ecosystem. Manufacturers are increasingly integrating intelligent sensor suites directly into the gearbox housing. These sensors continuously monitor critical operational parameters such as vibration signatures, acoustic emissions, operating temperatures, and oil degradation levels. By analyzing this real-time data using machine learning algorithms, plant operators can implement predictive maintenance strategies—identifying potential bearing failures or gear wear long before they result in catastrophic breakdowns and costly conveyor downtime.
The inherent sliding friction between the worm and the worm wheel has historically been the primary source of energy loss in these gearboxes. To combat this, manufacturers are pioneering advancements in metallurgy and tribology. Modern worm wheels are cast from proprietary, high-strength bronze alloys that offer superior wear resistance and lower friction coefficients. Simultaneously, the worms are subjected to advanced surface hardening treatments and precision CNC profile grinding to achieve mirror-like finishes. When paired with next-generation synthetic polyglycol lubricants, these metallurgical improvements significantly reduce operating temperatures and boost the overall mechanical efficiency of the gearbox, directly lowering the energy consumption of the conveyor system.
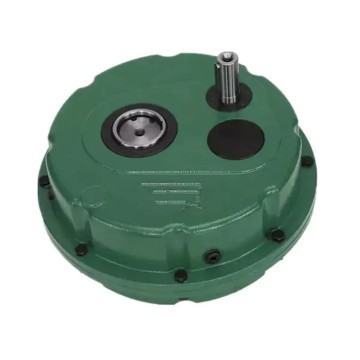
To provide OEMs with maximum flexibility, the industry is moving strongly towards modular design philosophies. Manufacturers now offer universal housings that can accept various input flanges, output shafts, and mounting accessories, allowing a single base unit to be adapted for dozens of different conveyor configurations. Furthermore, there is a growing trend towards hybrid helical-worm gearboxes. By placing a highly efficient helical gear stage ahead of the worm gear stage, manufacturers can achieve the high reduction ratios and right-angle layout of a traditional worm gearbox, but with significantly higher overall energy efficiency and torque capacity.
HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
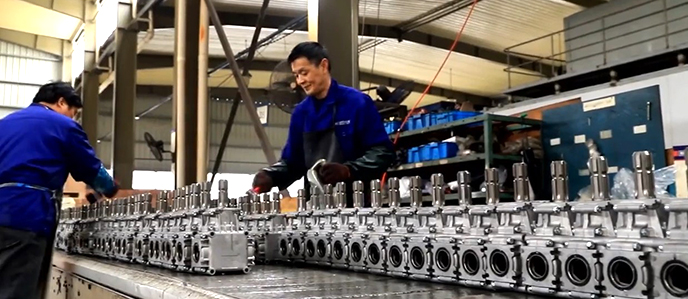
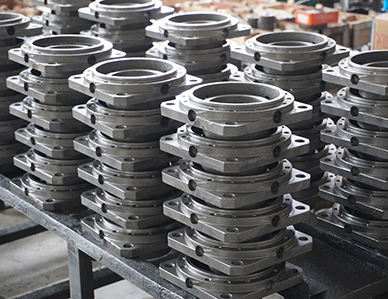
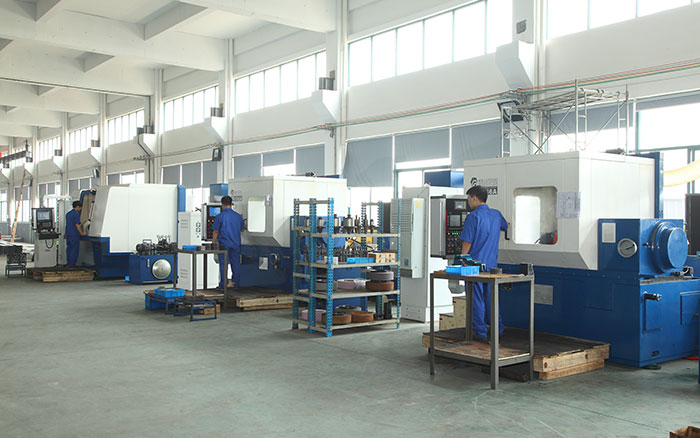
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
R&D Department: Our engineering team, led by veterans with over 15+ years of industry experience, is the core of our innovation. We maintain active "Industry-University-Research" collaborations with leading institutions to pioneer advancements in gear geometry, materials science, and tribology.
Skilled Workforce: Our production floor is staffed by highly trained and experienced technicians, with over 30% holding advanced technical certifications. Their craftsmanship and attention to detail are embedded in every product we build.
Management: Our leadership team brings international expertise and modern management practices, steering the company with a clear vision for sustainable growth and technological leadership.
DISCOVER OUR SUSTAINABILITY PROJECTS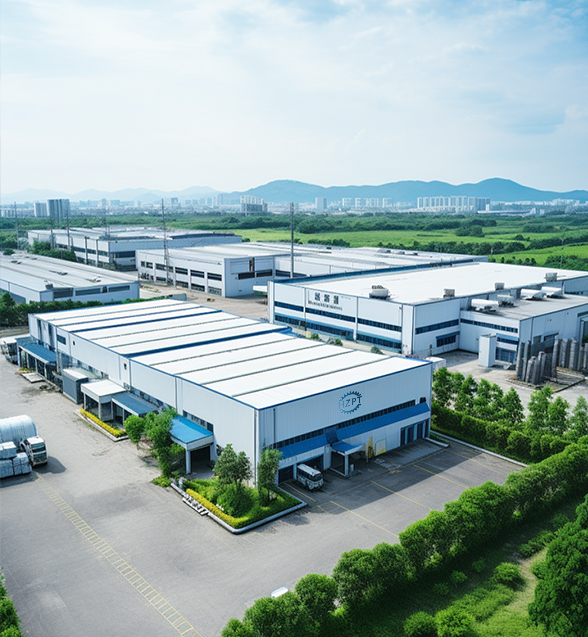
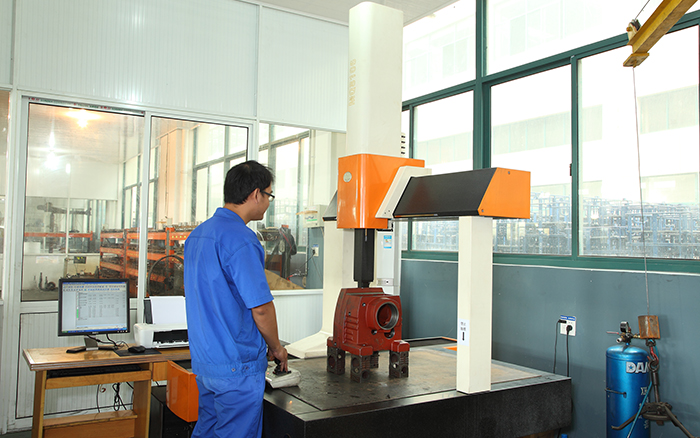
Our commitment to quality and innovation is validated by third-party accreditations and intellectual property. We hold 30+ national patents, including 5 invention patents. These cover key areas like "Modular Housing Design," "High-Efficiency Helical-Herringbone Gear Profiles," "Integrated Cooling Systems," and "Proprietary Surface Treatment Processes."
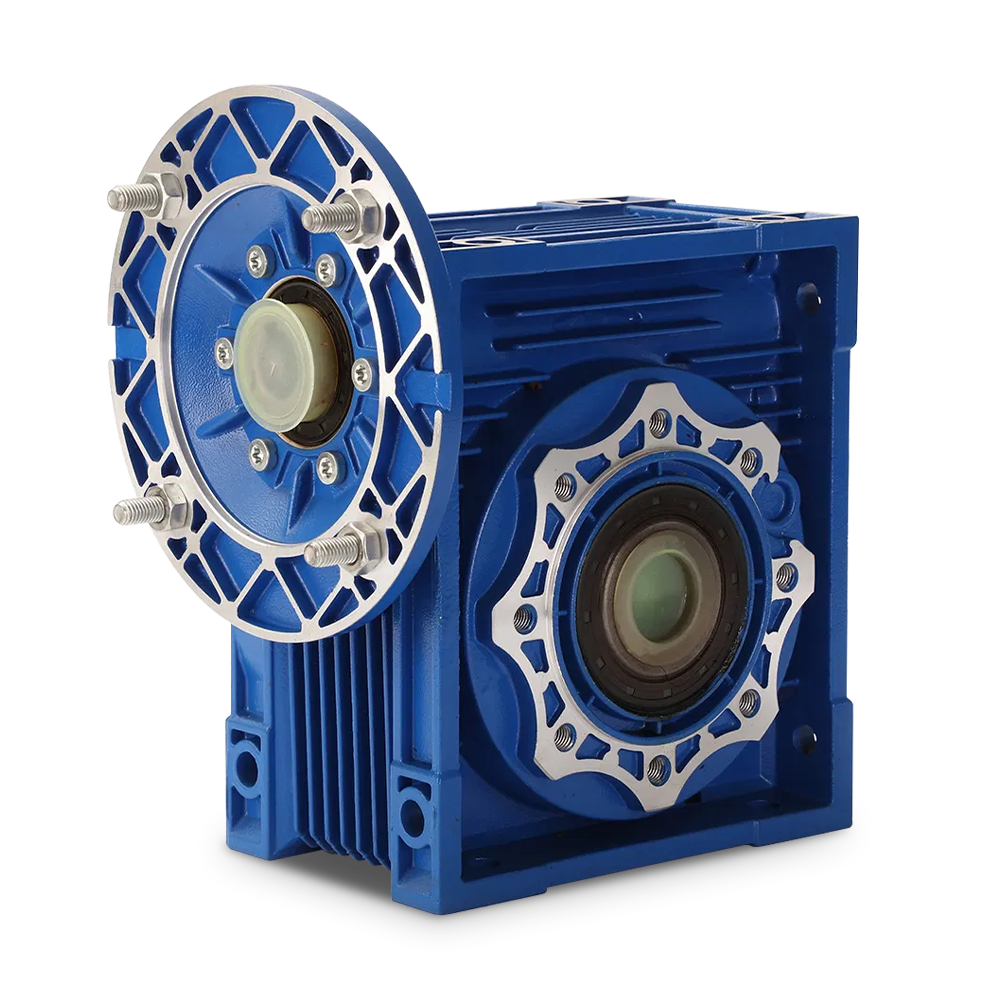
From high-precision sorting to heavy-duty lifting, discover our full range of gearboxes tailored for every aspect of conveyor systems and material handling.