Leave Your Message
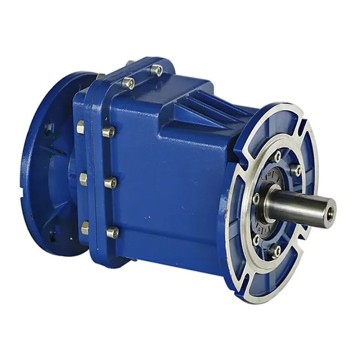
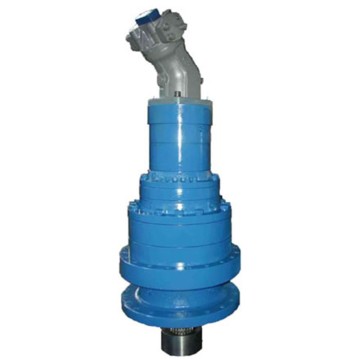
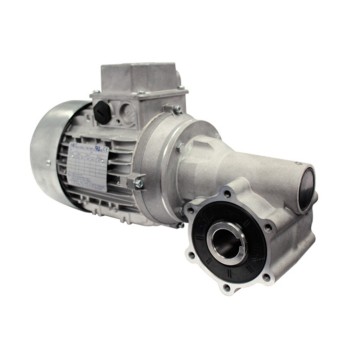
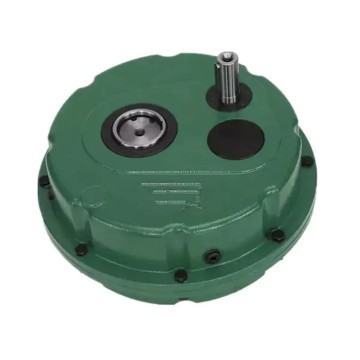
Explore our high-performance gear reducer series engineered for demanding water treatment and environmental applications.
Wastewater treatment and environmental management systems represent one of the most mechanically demanding sectors in modern industry. From municipal sewage plants processing millions of gallons daily to industrial effluent treatment facilities and stormwater management infrastructure, reliable power transmission is non-negotiable.
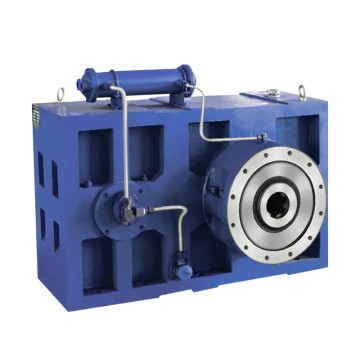
Worm gearboxes have emerged as the preferred drive solution for these environments due to their unique combination of high torque output at low speed, inherent self-locking capability, compact footprint, and exceptional resistance to shock loads — all critical attributes when driving sludge scrapers, aeration mixers, screw conveyors, and valve actuators in corrosive, wet, or chemically aggressive conditions.
The global wastewater treatment equipment market exceeded $25 billion USD in 2023 and is projected to surpass $38 billion by 2030, driven by tightening environmental regulations, rapid urbanization, and growing industrial water reuse mandates. Within this expanding market, worm gear reducers account for a significant share of mechanical drive components — and demand continues to accelerate.
Worm gearboxes serve as the mechanical backbone across the entire water treatment process chain — from intake to final discharge.
Worm gearboxes power the slow-speed, high-torque rotation of clarifier rake arms and sludge thickener mechanisms. Operating continuously at 0.1–2 RPM output, these drives must handle sudden torque spikes from dense sludge accumulation without stalling or damage. Our sealed, heavy-duty worm reducers are engineered for 24/7 continuous duty in these exact conditions.
Biological treatment relies on precise oxygen transfer via surface aerators and submerged mixers. Worm gearboxes provide the exact speed reduction needed to match motor output to optimal impeller velocity, maximizing oxygen transfer efficiency while minimizing energy consumption — a key factor as energy costs account for up to 60% of a treatment plant's operating budget.
Controlling water flow through large-diameter sluice gates and penstocks demands drives with precise position control and absolute self-locking when power is removed. The inherent self-locking characteristic of worm gearboxes makes them the industry standard for gate actuators in flood control, irrigation, and treatment plant flow management systems worldwide.
Dewatering screws, belt press drives, and centrifuge feed conveyors require consistent low-speed torque to move dense, abrasive sludge. Worm gearboxes deliver the necessary torque multiplication while their compact inline or right-angle configurations simplify mechanical integration into tight plant layouts. Stainless steel housing options are available for highly corrosive dewatering environments.
Chemical dosing pumps, pH neutralization mixers, and heavy metal precipitation reactors in industrial wastewater treatment all rely on precise, variable-speed drives. Worm gearboxes paired with inverter-duty motors provide the wide speed range and torque consistency required for accurate chemical treatment processes in pharmaceutical, electroplating, and food processing effluent systems.
Anaerobic digesters processing organic waste require slow, powerful agitation to maintain uniform bacterial culture distribution. Worm gearboxes driving top-entry or side-entry mixers in sealed digester vessels must maintain gas-tight integrity while delivering reliable torque under the extreme pressure and temperature conditions of biogas production — a growing renewable energy application globally.
The evolution of environmental regulations and smart infrastructure is reshaping requirements for worm gear reducers in wastewater systems.
Modern wastewater plants are transitioning to fully automated, data-driven operations. Worm gearboxes are increasingly specified with integrated encoder feedback, vibration sensors, and thermal monitoring — enabling predictive maintenance through SCADA and IIoT platforms. This shift reduces unplanned downtime by up to 40% and is becoming a procurement requirement for major municipal contracts globally.
With energy constituting the largest operational cost in water treatment, regulators in the EU, USA, and Asia are mandating IE3 and IE4 premium efficiency motors. This is driving demand for optimized worm gearbox designs with higher mechanical efficiency ratings, improved bronze alloy worm wheels, and precision-ground worm shafts that maximize power transmission efficiency across the full load range.
As water reuse and direct potable reuse (DPR) projects expand globally, gearboxes in contact with reclaimed water must meet NSF/ANSI 61 standards. This is accelerating adoption of stainless steel housings, FDA-compliant gear lubricants, and EPDM seals resistant to chlorine and ozone disinfection chemicals — capabilities our engineering team has built into our environmental-grade product lines.
The trend toward compact, containerized, and modular water treatment units for remote communities, disaster relief, and industrial sites demands smaller, lighter, and more versatile gearbox configurations. Our compact worm gear series with multiple mounting options and universal motor flanges directly addresses this growing market segment, which is projected to grow at over 8% CAGR through 2030.
Our worm gearboxes are built to perform in the harshest wastewater and environmental system conditions — delivering decades of reliable service with minimal maintenance. From municipal treatment plants to industrial effluent systems and biogas facilities, we provide the precision drive technology your critical infrastructure demands.
Request a Custom SolutionA Legacy of Growth & Innovation
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and establish a solid technical foundation that would support decades of growth.
Responding to evolving market demands, we significantly expanded our production capabilities and R&D investments. This period saw the introduction of custom-engineered and application-specific solutions — including environmental and wastewater-grade gearboxes — enabling us to serve more complex industrial needs and establish long-term global partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools, automated machining centers, and precision quality systems, we now deliver next-generation products that are smarter, more compact, and more energy-efficient — solidifying our position as a global industry innovator in power transmission technology.
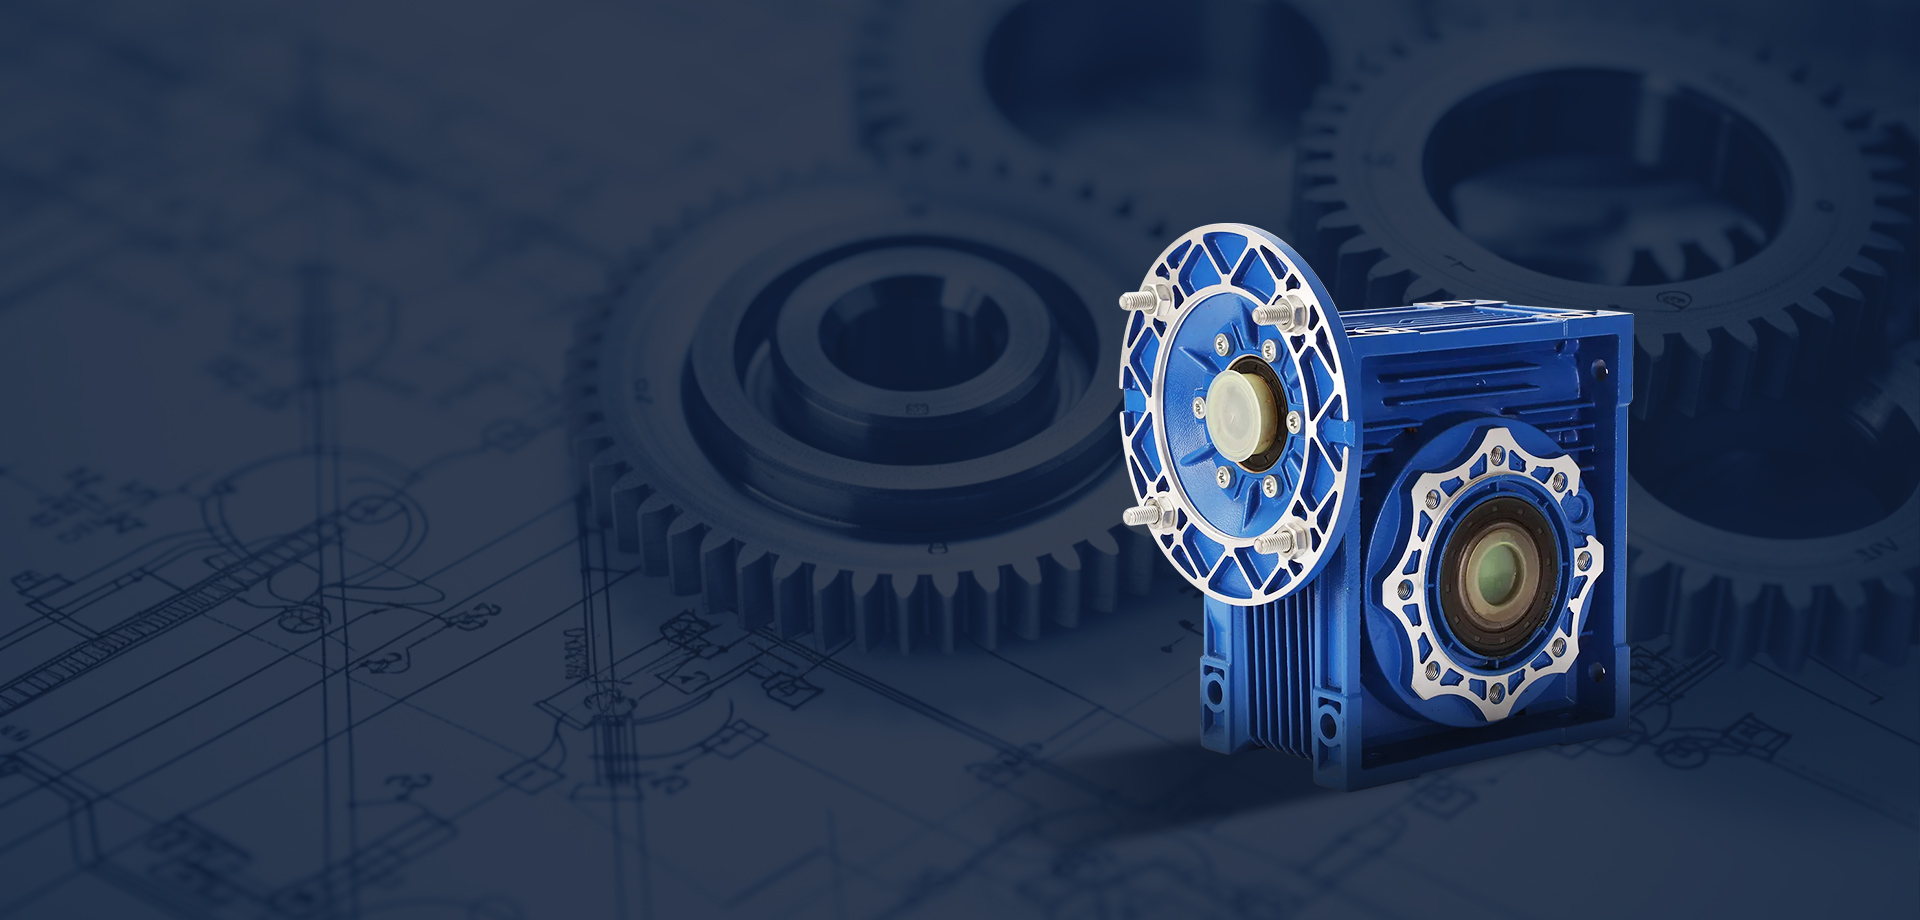
We invest in world-class technology to ensure every product that leaves our facility is built to excel in the most demanding environmental applications.
Quality is at the heart of everything we do — especially for mission-critical wastewater and environmental infrastructure.
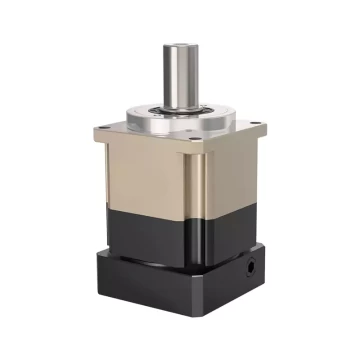
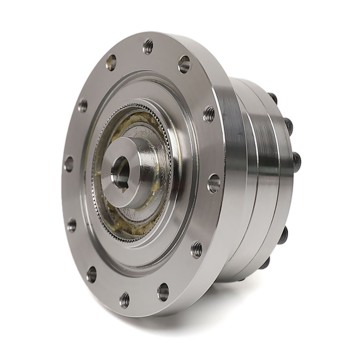
No diversions — just decades of refining worm gear, helical, planetary, and parallel-shaft gearboxes for industrial and environmental applications. Our deep domain expertise means faster problem-solving and better-engineered solutions for wastewater system OEMs and EPC contractors.
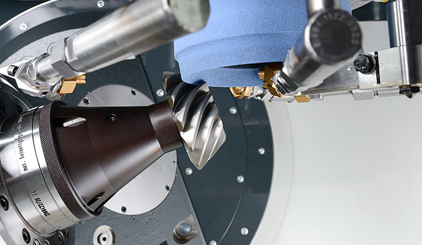
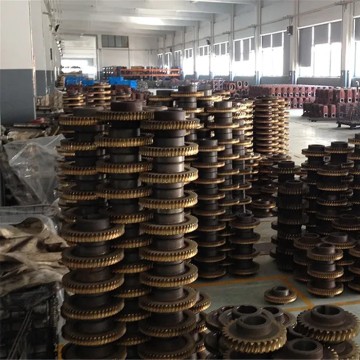
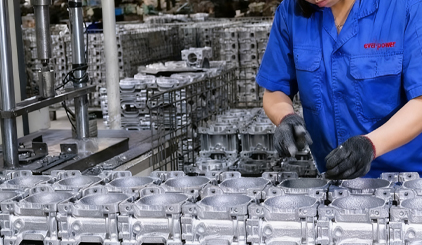
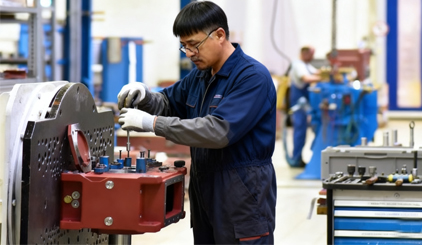
Critical processes including worm shaft grinding, bronze wheel casting, heat treatment, and housing machining are all performed under one roof. This vertical integration ensures consistent quality, shorter lead times, and full traceability — essential for environmental compliance documentation.
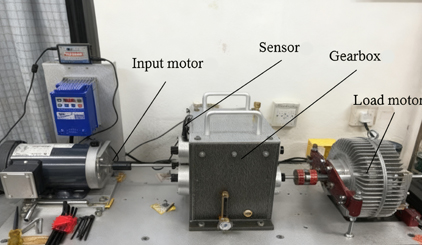
100% factory acceptance testing at rated torque with vibration, temperature rise, and leakage verification — test reports available on request. For wastewater applications where unplanned downtime means environmental incidents and regulatory penalties, this pre-shipment validation is invaluable peace of mind.
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese — because your uptime matters. For environmental system operators, rapid technical support can be the difference between a minor adjustment and a costly process shutdown.
Explore our full range of precision gear reducers designed for diverse industrial and environmental system requirements.