Leave Your Message
Discover our top-tier power transmission solutions customized for mining, excavation, and high-load industrial applications. Built to withstand extreme conditions.
The global mining equipment market is currently experiencing a technological renaissance. As ore grades decline globally, mining corporations are forced to process significantly larger volumes of material to maintain profitability. This operational shift places unprecedented stress on heavy machinery, driving a massive commercial demand for ultra-reliable power transmission components, particularly the Heavy-Duty Worm Gearbox.
In the contemporary industrial landscape, the cost of unplanned downtime in a mining operation can easily exceed hundreds of thousands of dollars per hour. Consequently, procurement managers and heavy equipment engineers are shifting their focus from initial capital expenditure (CAPEX) to Total Cost of Ownership (TCO). Worm gear reducers have become a focal point in this paradigm shift. Their inherent design—offering high torque multiplication in a compact, right-angle footprint—makes them indispensable for space-constrained, high-load applications. Furthermore, the commercial supply chain is increasingly demanding gearboxes that not only deliver raw mechanical power but also integrate seamlessly with modern, automated mining infrastructure.
Supply chain dynamics indicate a strong trend towards localized, highly specialized manufacturing. Companies that can provide end-to-end solutions—from raw gear forging to final assembly load testing—are dominating the market. The reliance on robust worm gears in continuous processing plants, such as those used for copper, lithium, and gold extraction, underscores their critical role in the global transition towards electrification and green energy, which heavily relies on mined raw materials.
A Legacy of Growth & Innovation. Our journey is one of continuous evolution and strategic expansion.
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and build a solid technical foundation.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions, enabling us to serve more complex industrial needs and establish long-term partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools and automated processes, we now deliver next-generation products that are smarter, more compact, and more energy-efficient, solidifying our position as an industry innovator.
In mining operations, the transportation of bulk materials—ranging from blasted rock to refined coal—relies heavily on extensive conveyor networks. Worm gearboxes are the unsung heroes of these systems. Belt conveyors and screw conveyors require right-angle drives to save valuable operational space along the conveyor galleries. The unique sliding action of the worm and worm wheel provides exceptional shock load absorption, a critical feature when tons of irregular, heavy rocks are suddenly dumped onto a moving belt. Furthermore, the inherent self-locking capability of certain high-ratio worm gears acts as a natural backstop, preventing loaded conveyors from rolling backward during a sudden power failure, thereby ensuring worker safety and preventing catastrophic equipment damage.
The comminution process (crushing and grinding) is the most energy-intensive stage in mining. Equipment such as jaw crushers, cone crushers, and ball mills operate under continuous, brutal vibration and extreme torque requirements. Here, the metallurgical integrity of the worm gearbox is tested to its limits. Utilizing centrifugally cast bronze alloy worm wheels paired with case-hardened, precision-ground steel worms allows these gearboxes to withstand the violent torque spikes generated when uncrushable materials enter the chamber. The robust cast iron or ductile iron housings of these reducers ensure that internal gear alignments remain true even when the external environment is subjected to severe seismic-like vibrations.
Underground mining relies on massive hoists and winches to transport personnel, equipment, and extracted ore vertically through mine shafts. Safety is the absolute highest priority in these applications. Worm gearboxes are frequently specified for winch drives due to their precise speed reduction and dynamic braking assistance. The irreversible nature of specific worm gear configurations means that the load cannot back-drive the motor. When combined with secondary mechanical brakes, a worm gear-driven hoist provides a redundant, fail-safe lifting mechanism that meets the strictest international mining safety regulations.
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
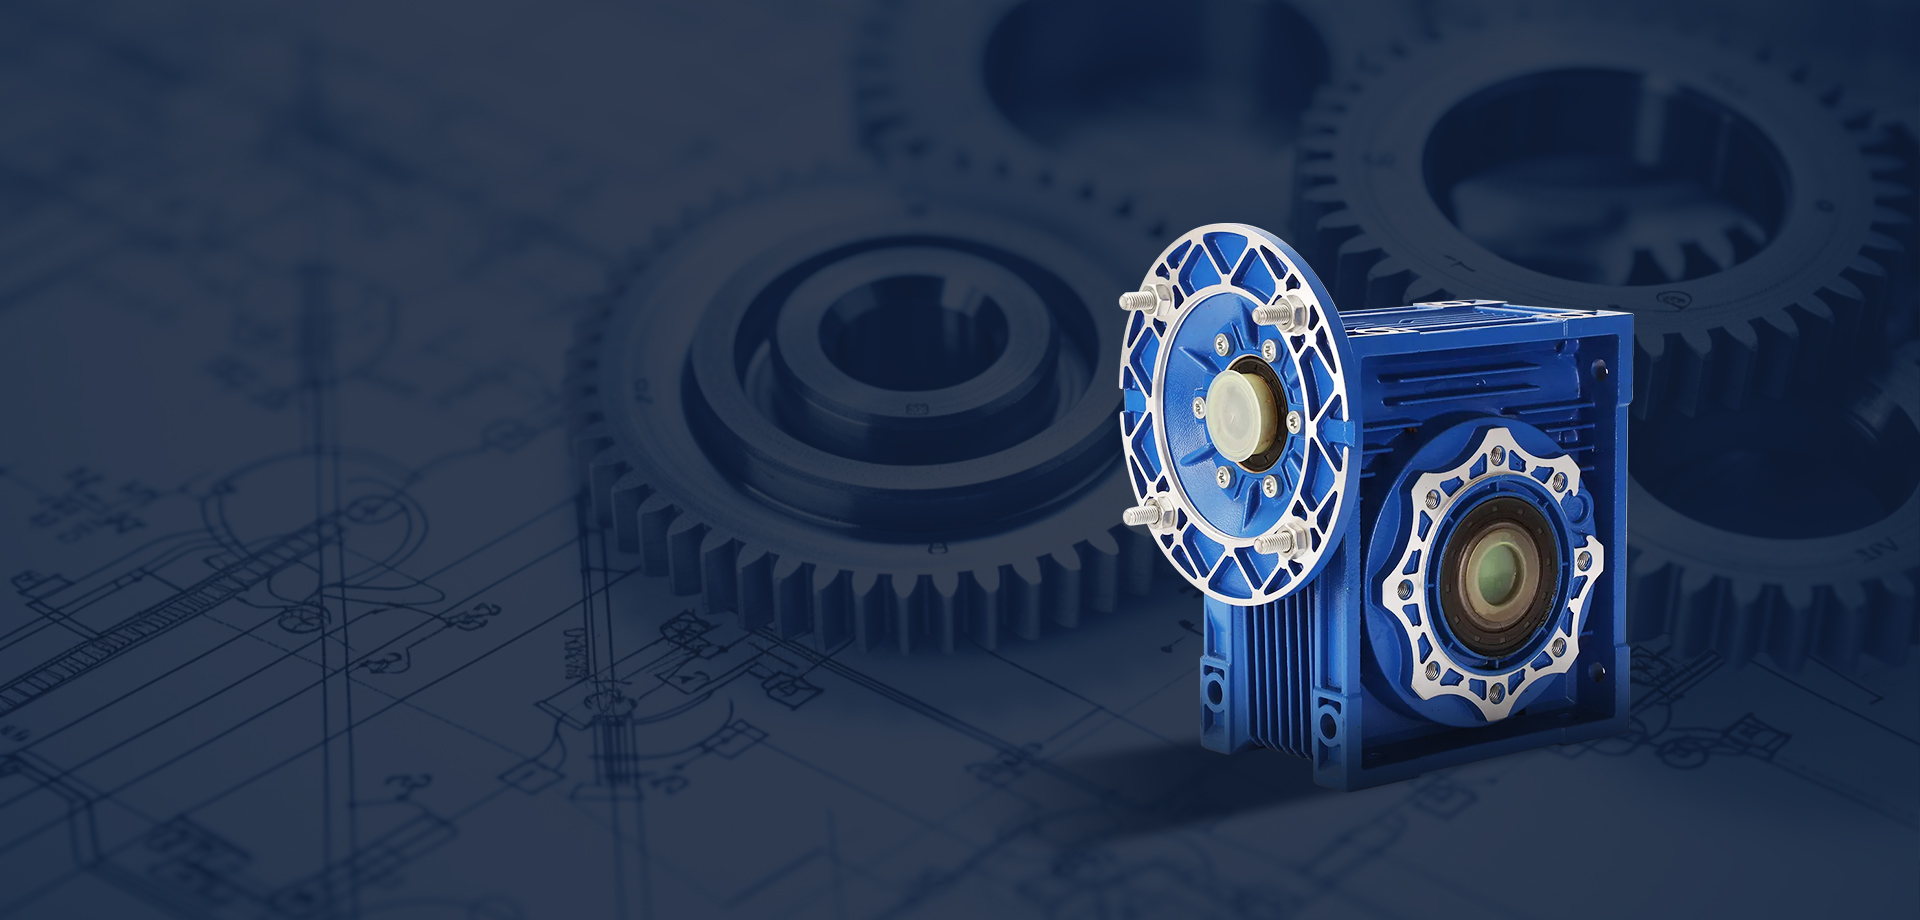
The future of Worm Gearboxes for Mining and Heavy Equipment is inextricably linked to Industry 4.0 and the Industrial Internet of Things (IIoT). Traditionally, maintenance in heavy industries was either reactive (fixing it when it breaks) or strictly scheduled (replacing parts based on operational hours, regardless of actual wear). Both approaches are economically inefficient. Today, we are witnessing the rapid development of "Smart Gearboxes." These advanced units are equipped with embedded sensors that continuously monitor critical parameters such as oil temperature, high-frequency vibration signatures, and acoustic emissions.
By feeding this real-time data into AI-driven predictive maintenance algorithms, mining operators can accurately forecast bearing failures or gear wear weeks before they cause a catastrophic breakdown. This technological leap transforms unexpected downtime into scheduled, manageable maintenance windows. Furthermore, advancements in tribology and synthetic lubrication are pushing the thermal boundaries of worm gearboxes. High-performance synthetic oils drastically reduce sliding friction, increasing the overall mechanical efficiency of the worm drive while extending oil change intervals—a crucial benefit for equipment located in remote, difficult-to-access mining sites.
Quality is at the heart of everything we do. Partner with a manufacturer that understands heavy industry.
No diversions—just decades of refining helical, planetary, and parallel-shaft gearboxes for industrial applications.
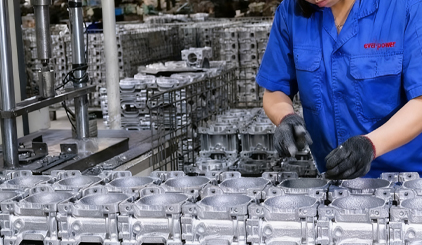
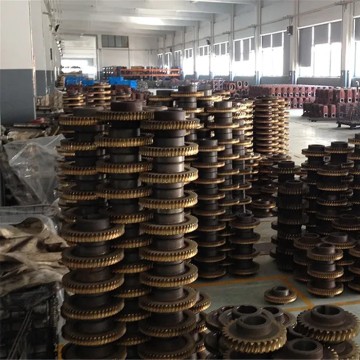
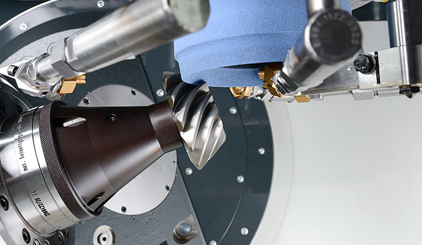
From gear forging to final assembly. Critical processes like grinding and heat treatment are done under one roof.
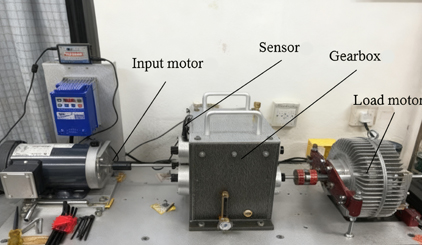
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks.
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations.
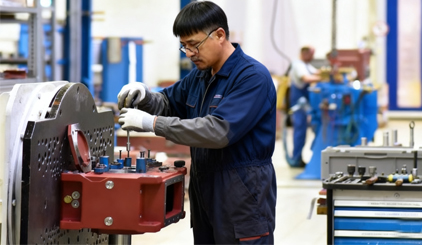
Explore our complete range of gearboxes, precision-engineered to meet the rigorous demands of global mining, extraction, and heavy material processing industries.