Leave Your Message
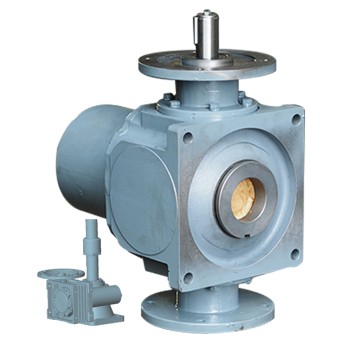
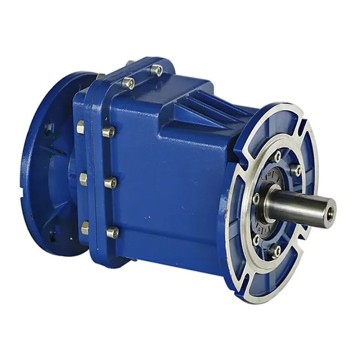
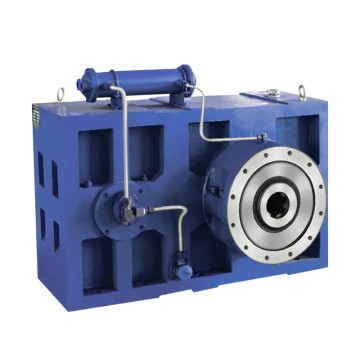
Explore our top-selected worm gearbox and reducer series engineered for conveyor systems, material handling lines, and demanding industrial environments.
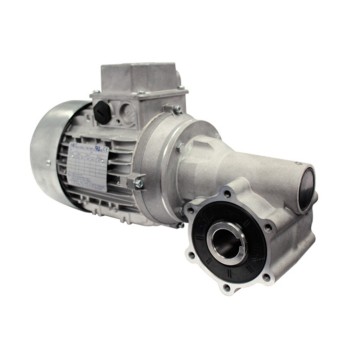
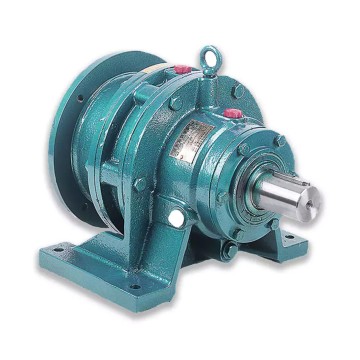
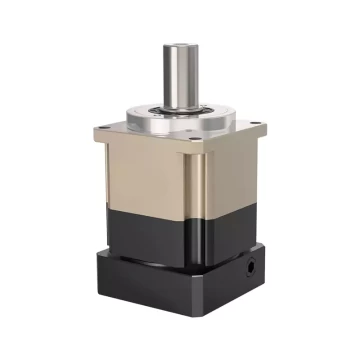
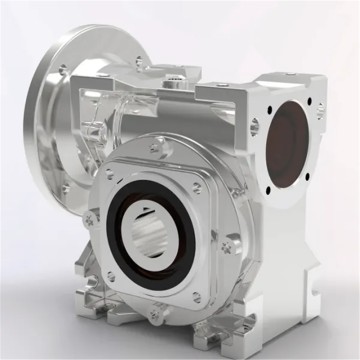
A worm gearbox — also known as a worm gear reducer — is a type of gear system in which a worm (a screw-like gear) meshes with a worm wheel (a toothed gear) to transmit rotational motion and torque between non-intersecting, perpendicular shafts. This unique geometry enables high speed-reduction ratios in a compact form factor, making worm gearboxes indispensable in conveyor systems and material handling applications worldwide.
The inherent self-locking characteristic of worm gears — where the worm can drive the wheel but the wheel cannot back-drive the worm — is a critical safety advantage in vertical or inclined conveyor applications, preventing uncontrolled load reversal when power is cut. This feature alone has made worm gearboxes the preferred drive solution for elevators, escalators, inclined belt conveyors, and lifting platforms in warehouses and distribution centers.
The global conveyor systems market is projected to surpass USD 12 billion by 2030, driven by explosive growth in e-commerce fulfillment, automated warehousing, and smart manufacturing. At the heart of nearly every conveyor drive system lies a gearbox — and worm gearboxes capture a significant share of this demand due to their cost-effectiveness, compactness, and reliability in moderate-duty cycles.
In logistics hubs and distribution centers operated by giants like Amazon, DHL, and JD.com, thousands of worm gear reducers run continuously, driving belt conveyors, roller conveyors, chain conveyors, and sortation systems. The growing adoption of Industry 4.0 and smart factory concepts is pushing manufacturers to deliver worm gearboxes with integrated sensors, IoT connectivity, and predictive maintenance capabilities — transforming a traditionally mechanical component into an intelligent drive node.
In the food & beverage sector, stainless steel worm gearboxes (such as the SSRV Series) are mandatory in hygienic conveyor lines handling packaged goods, fresh produce, and meat processing — where wash-down resistance and corrosion immunity are non-negotiable. The pharmaceutical and chemical industries similarly demand sealed, leak-proof worm gearboxes that meet strict contamination standards.
Traditional worm gearboxes have faced criticism for lower efficiency (typically 70–90%) compared to helical gearboxes. However, advances in synthetic lubricants, precision-ground worm profiles, and optimized bronze alloy wheel materials are pushing efficiency levels higher. Manufacturers are also combining worm stages with helical pre-stages to create worm-helical hybrid reducers that deliver superior efficiency while retaining the self-locking and high-ratio benefits of worm geometry.
Next-generation worm gearboxes are being equipped with embedded vibration sensors, temperature probes, and oil condition monitors that feed real-time data to cloud-based maintenance platforms. This shift enables predictive maintenance scheduling, reducing unplanned downtime in conveyor systems by up to 40% — a critical advantage in 24/7 automated fulfillment operations.
Demand from mobile material handling equipment — including AGVs (Automated Guided Vehicles), collaborative robots, and compact conveyor modules — is driving the development of miniaturized, lightweight worm gearboxes with aluminum housings and hollow shaft configurations that simplify installation and reduce system weight without compromising torque capacity.
Environmental regulations and corporate ESG commitments are accelerating the adoption of eco-friendly manufacturing processes for gearbox production — including reduced-waste precision machining, recyclable housing materials, and biodegradable lubricants compatible with worm gear contact surfaces.
HZPT worm gearboxes power conveyor systems in automotive plants, e-commerce fulfillment centers, food processing lines, mining operations, and pharmaceutical facilities worldwide — delivering consistent performance where reliability is not optional.
Discover Our Sustainability ProjectsFrom agricultural logistics to smart warehousing, worm gearboxes drive critical motion across every major industry vertical.
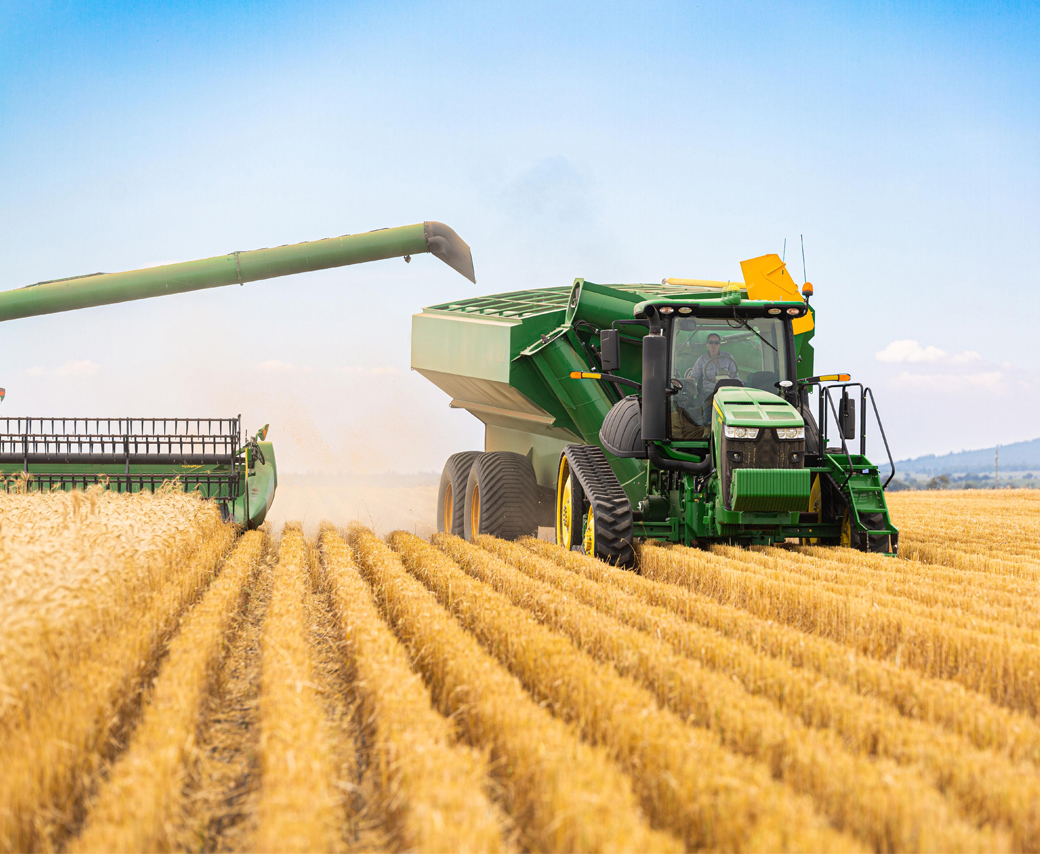
In grain elevators, seed sorting lines, and crop processing conveyors, worm gearboxes deliver the low-speed, high-torque drive needed to move bulk materials reliably — even in dusty, outdoor environments with wide temperature fluctuations. Decades of refinement in helical, planetary, and parallel-shaft configurations ensure optimal performance for agricultural applications.
Read more →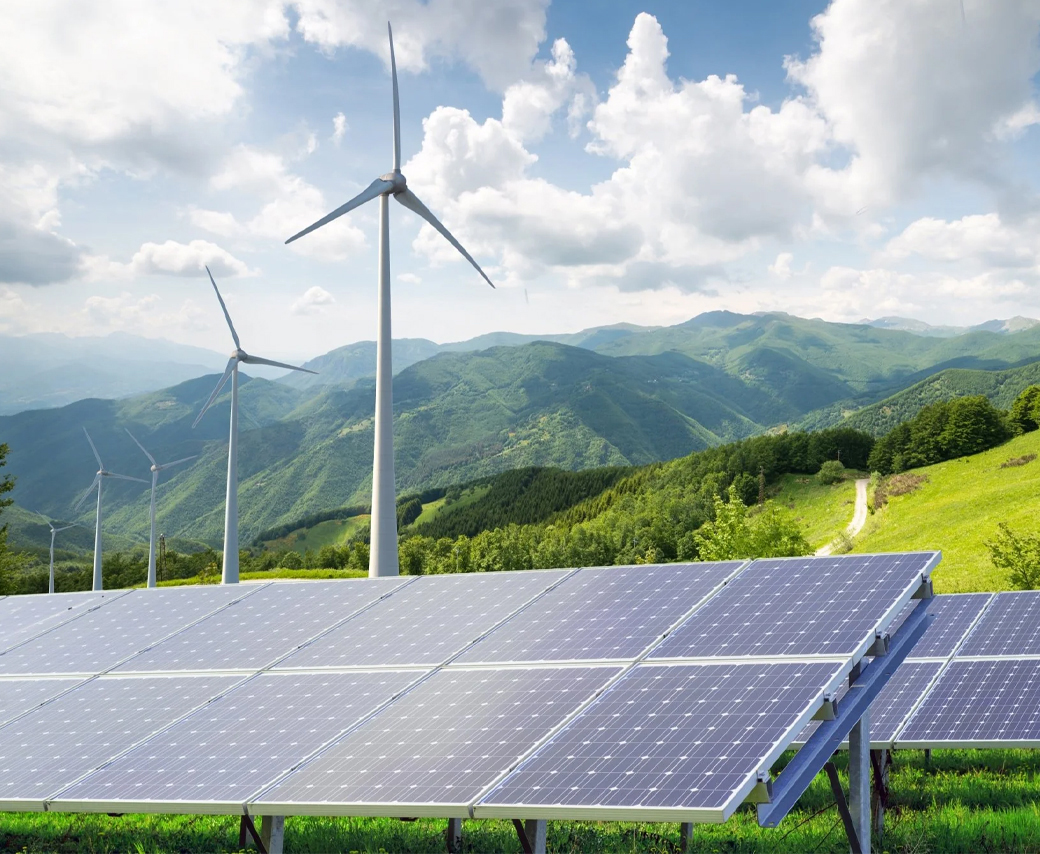
Worm and planetary gearboxes are central to wind turbine nacelle assembly conveyors and component handling systems. Precision yaw and pitch drive gearboxes must operate maintenance-free for 20+ years in extreme environments — demanding the highest standards of material quality and sealing technology.
Read more →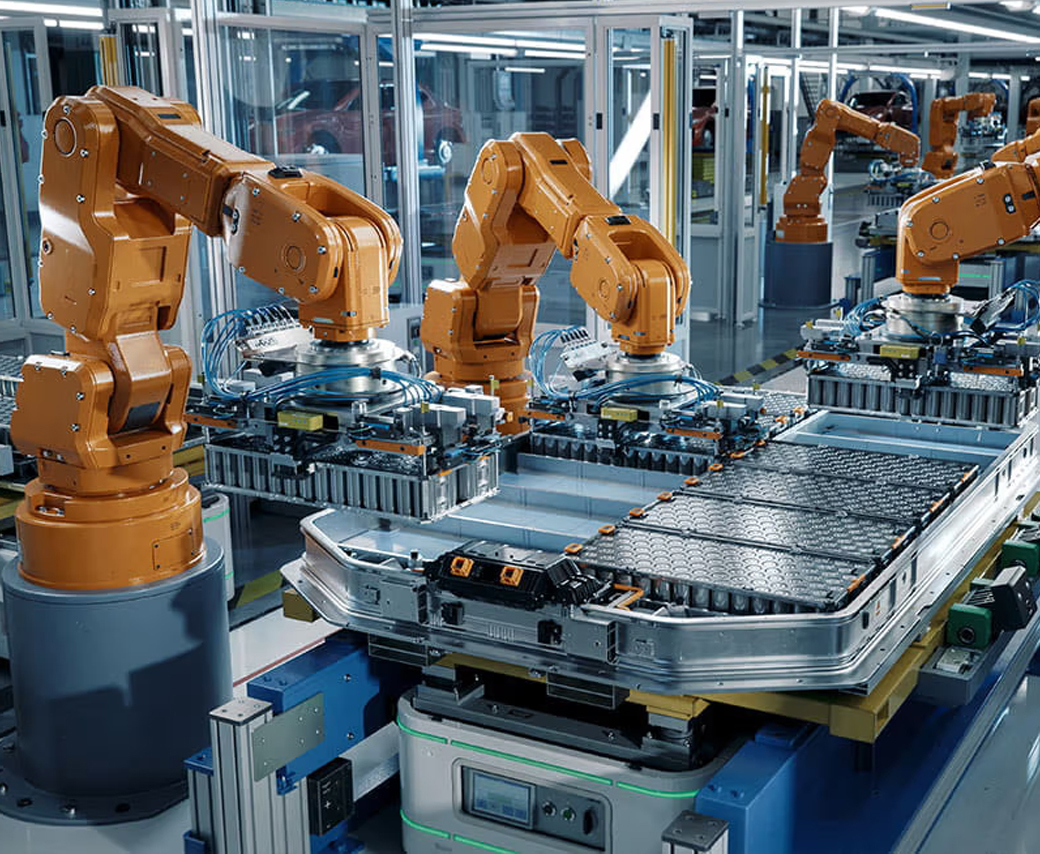
From robotic palletizing systems to high-speed CNC part transfer conveyors and automated assembly lines, worm gearboxes provide the precise speed reduction and torque multiplication needed for micron-level positioning accuracy and smooth, repeatable motion control in Industry 4.0 environments.
Read more →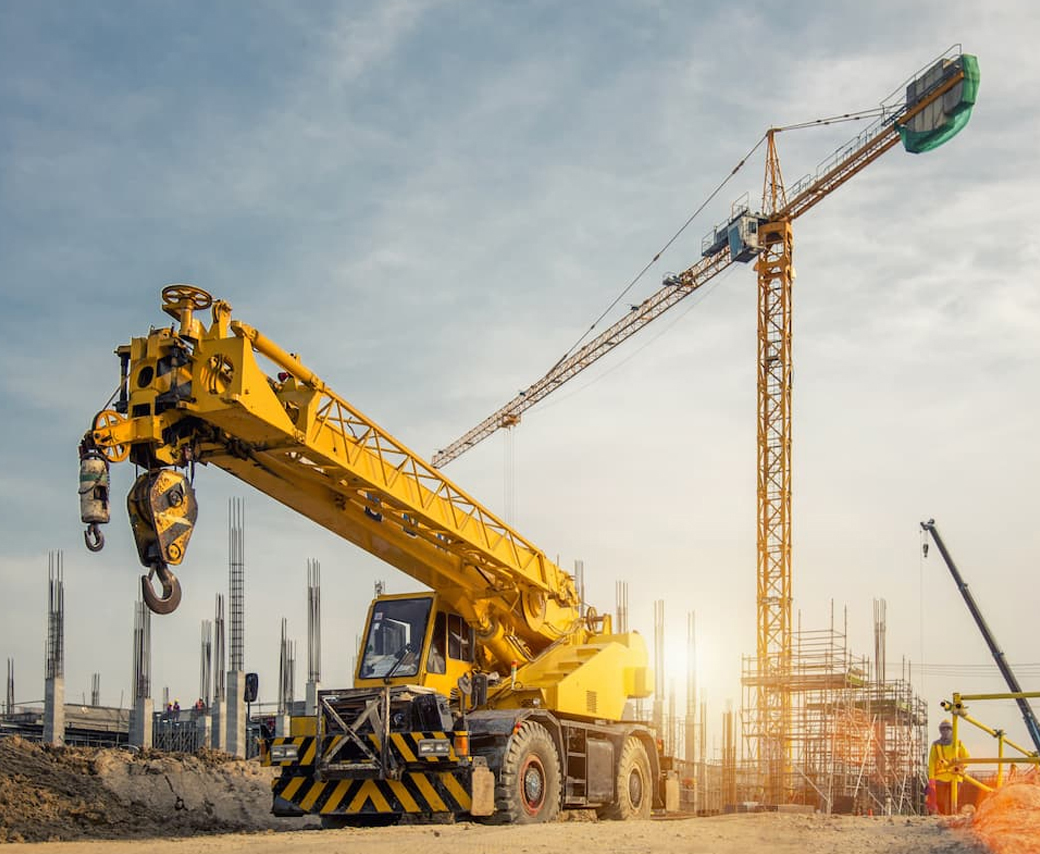
In cranes, concrete mixer conveyors, excavator swing drives, and pile driver feed systems, rugged worm and helical-worm gearboxes handle heavy shock loads, frequent start/stop cycles, and harsh job-site conditions — engineered for durability where failure is not an option.
Read more →The convergence of automation, e-commerce growth, and sustainability mandates is reshaping the worm gearbox landscape for conveyor and material handling applications.
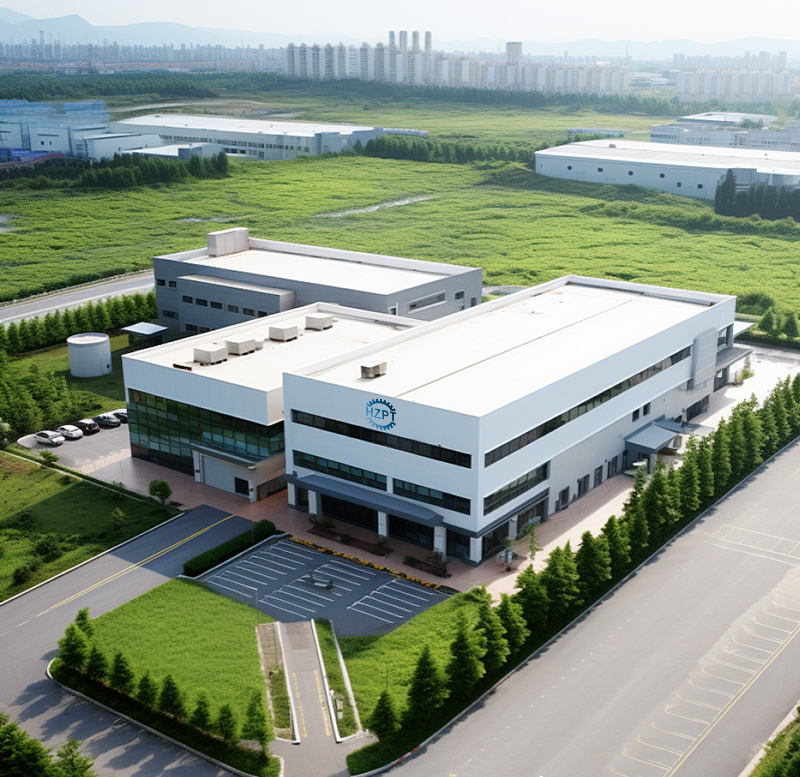

HZPT is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
DISCOVER OUR SUSTAINABILITY PROJECTSBrowse our comprehensive lineup of industrial gearboxes and reducers — engineered for every conveyor, material handling, and power transmission requirement.