Leave Your Message
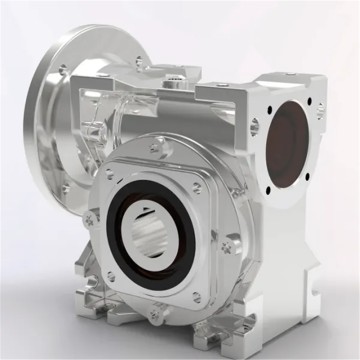
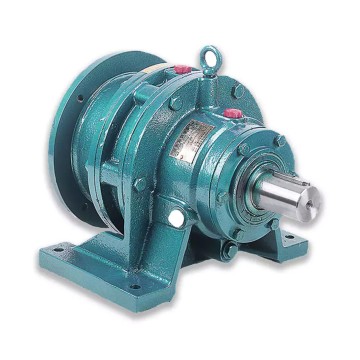
In the rapidly evolving landscape of global logistics, manufacturing, and bulk material handling, the Worm Gear Reducer for Conveyor Systems and Material Handling stands as a critical component in ensuring seamless power transmission. A worm gear reducer is ingeniously designed to transmit high torque while simultaneously reducing the rotational speed of an electric motor. Its unique right-angle configuration makes it exceptionally space-efficient, allowing engineers to design compact conveyor layouts without sacrificing mechanical power. Furthermore, the inherent self-locking characteristic of specific worm gear ratios provides an invaluable safety mechanism—preventing conveyors from reversing under heavy loads in the event of a power failure. This natural braking ability is indispensable in inclined material handling systems, elevating the safety standards across multiple industrial sectors.
From a commercial and industrial standpoint, the demand for robust worm gear reducers has skyrocketed, driven largely by the explosive growth of the e-commerce sector and the automation of global supply chains. Mega-distribution centers operated by retail giants rely on miles of intricate conveyor networks—including belt conveyors, roller conveyors, and cross-belt sorters. Every single node in these automated sorting systems requires highly reliable, low-maintenance gearboxes to operate continuously, 24/7, with minimal downtime. The global market valuation for industrial gearboxes in material handling continues to experience a robust Compound Annual Growth Rate (CAGR), reflecting the industrial shift towards higher efficiency and automated throughput. Beyond e-commerce, heavy industries such as mining, aggregate processing, and agriculture demand heavy-duty worm gear reducers capable of withstanding extreme shock loads, pervasive dust, and continuous operational stress. The commercial reality is clear: the efficiency of a material handling system is directly proportional to the reliability of its gear reducers.
As Industry 4.0 transforms manufacturing floors into smart ecosystems, the Worm Gear Reducer is undergoing a profound technological renaissance. The integration of Artificial Intelligence (AI) and the Internet of Things (IoT) is shifting the paradigm from reactive repairs to predictive maintenance. Modern gearboxes are increasingly being equipped with smart sensors that monitor real-time vibration frequencies, acoustic emissions, and thermal fluctuations. By feeding this telemetry data into AI-driven analytics platforms, facility managers can accurately predict component wear and schedule maintenance long before a catastrophic failure halts the conveyor line. This technological leap significantly reduces Total Cost of Ownership (TCO) and maximizes operational uptime in mission-critical material handling applications.
Material science and advanced lubrication technologies are also setting new industry trends. The push for stringent hygiene standards in the food and beverage industry has led to the widespread adoption of stainless steel worm gear reducers, such as the SSRV series. These specialized units feature smooth, crevice-free housings and IP69K washdown ratings, making them impervious to high-pressure, high-temperature chemical cleanings. Additionally, the development of advanced synthetic polyglycol lubricants has dramatically reduced the sliding friction inherent in worm gear designs. This advancement not only extends the operational lifespan of the bronze worm wheel but also boosts the overall mechanical efficiency of the reducer, helping industrial facilities meet increasingly strict global energy consumption regulations. The future points toward modular, energy-efficient, and highly intelligent power transmission solutions that seamlessly integrate into complex, automated conveyor architectures.
The versatility of the worm gear reducer allows it to be customized for a wide array of highly specialized material handling environments. Understanding these deep-dive application scenarios highlights the engineering precision required to keep global industries moving efficiently.
In modern fulfillment centers, speed and precision are paramount. Worm gear reducers drive the intricate networks of accumulation roller conveyors and high-speed belt sorters. Their compact right-angle design allows them to be tucked neatly under the conveyor frame, maximizing warehouse floor space. The low noise output of precision-machined worm gears is crucial in environments where hundreds of drives operate simultaneously, ensuring a safer and more comfortable acoustic environment for warehouse personnel. Additionally, their rapid start-stop capabilities perfectly match the dynamic indexing requirements of barcode scanning and parcel routing systems.
Conveyor systems in the food processing industry operate under some of the most rigorous regulatory conditions globally. Here, stainless steel worm gear reducers are deployed to drive bottling lines, meat processing conveyors, and packaging machinery. The gearboxes must resist corrosion from daily caustic washdowns while preventing any risk of lubricant leakage that could contaminate the food supply. Utilizing food-grade synthetic oils and robust double-lip seals, these reducers ensure compliance with FDA and HACCP standards while delivering the precise torque needed for delicate packaging operations without crushing the product.
Moving thousands of tons of raw ore, coal, or crushed stone requires immense mechanical resilience. In mining material handling, worm gear reducers are frequently utilized in inclined overland conveyors and bucket elevators. The harsh, abrasive environments necessitate heavy-duty cast iron housings and enhanced dust-proof sealing arrangements. The critical advantage here is the self-locking nature of the high-ratio worm gear; if the main power supply fails, the gearbox mechanically prevents the massive weight of the conveyed aggregate from back-driving the belt, averting catastrophic equipment damage and ensuring worker safety.
Airport baggage handling is a highly complex logistical puzzle requiring absolute reliability. A single gearbox failure can lead to severe flight delays and lost luggage. Worm gear reducers are extensively used to power the check-in conveyors, curved belt sections, and carousel reclaim areas. They offer the perfect balance of smooth acceleration, high torque density, and operational quietness. The modularity of these gear units allows maintenance crews to perform rapid swap-outs during the short overnight maintenance windows, ensuring the BHS remains fully operational for the morning rush.
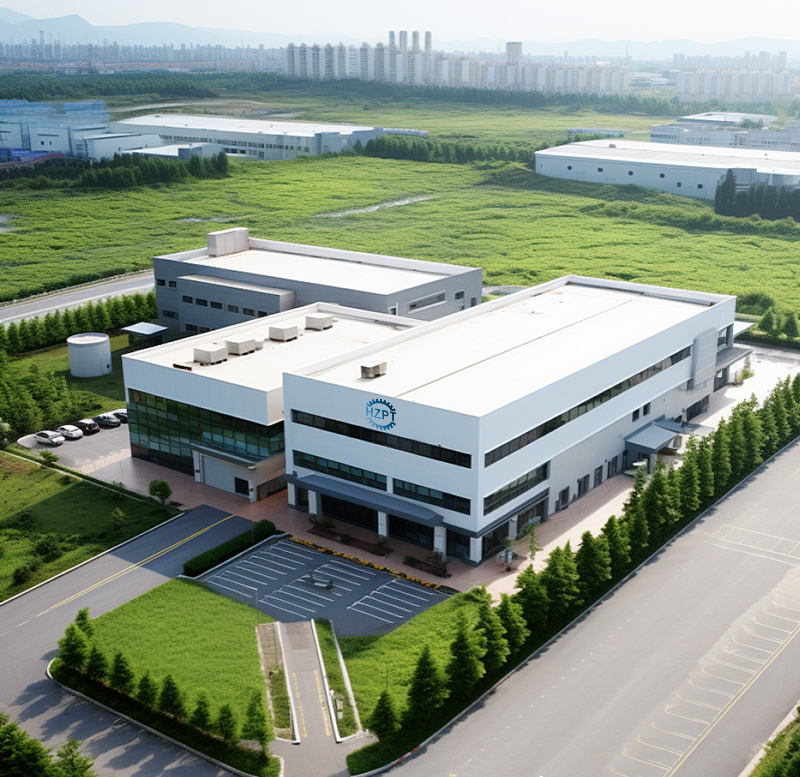

HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
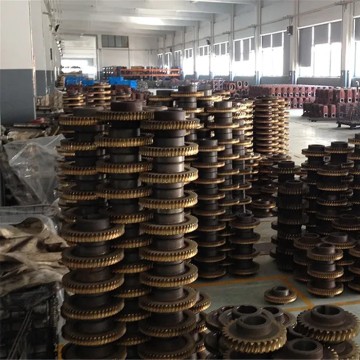
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
DISCOVER OUR SUSTAINABILITY PROJECTS
No diversions—just decades of refining helical, planetary, and parallel-shaft gearboxes for heavy-duty agricultural and bulk material handling applications.
Read more
Planetary gearboxes are at the heart of wind turbine systems and heavy material lifting mechanisms, driving yaw and pitch mechanisms that optimize orientation. Built for 20+ years of maintenance-free operation.
Read more
From robotic arms to high-speed sorting conveyors and machining centers, our low-backlash gearboxes ensure positioning accuracy, smooth motion control, and long-term repeatability in automated production lines.
Explore Applications
Used in cranes, excavators, concrete mixers, and aggregate conveyors, our rugged gearboxes handle heavy loads, frequent starts/stops, and harsh job-site conditions—ensuring durability where failure is not an option.
Explore Applications