Leave Your Message
Engineered for high torque, exceptional durability, and seamless integration into modern conveyor architectures.
In the rapidly evolving landscape of global industry, Speed Reducer Gearboxes for Conveyor Systems and Material Handling have become the unsung heroes of operational efficiency. As e-commerce surges and supply chains become increasingly complex, the demand for robust, reliable, and highly efficient power transmission systems has reached unprecedented levels. A speed reducer gearbox is not merely a mechanical component; it is the vital bridge between the high-speed rotation of electric motors and the high-torque, controlled movement required by heavy-duty conveyor belts, roller conveyors, and automated sorting systems.
Currently, the industrial and commercial sectors are undergoing a massive shift towards Automated Material Handling (AMH). Warehouses, distribution centers, mining operations, and manufacturing plants are replacing manual labor with automated conveyor networks to enhance throughput and reduce operational costs. This paradigm shift requires gearboxes that can operate continuously under extreme loads, varying speeds, and harsh environmental conditions. The global market is witnessing a strong preference for shaft-mounted gearboxes, helical-bevel reducers, and precision planetary gearboxes that offer high power density, space-saving designs, and minimal maintenance requirements.
Furthermore, the integration of speed reducers in material handling is no longer just about torque multiplication; it is about precision control. In applications such as Automated Guided Vehicles (AGVs) and robotic palletizers, the gearbox must ensure zero-backlash and exact positioning. This has driven manufacturers to innovate, utilizing advanced metallurgy, precision gear grinding techniques, and optimized lubrication systems to create gearboxes that deliver maximum efficiency with minimal energy loss.
From rugged mining operations to sterile food processing, our speed reducers are engineered to conquer diverse industrial challenges.
In mining and quarrying, conveyor systems transport thousands of tons of raw materials daily. These environments expose machinery to extreme dust, heavy shock loads, and continuous operation. Shaft-mounted gearboxes (like the DXG/ATA series) and Cycloidal reducers are preferred here. They offer exceptional shock load resistance and are designed to mount directly onto the conveyor head pulley, eliminating the need for complex foundation alignments and reducing the overall footprint.
Modern fulfillment centers rely on high-speed sortation conveyors and Automated Storage and Retrieval Systems (AS/RS). In these scenarios, speed reducers must provide rapid start-stop capabilities, low noise, and high efficiency. Lightweight aluminum housing worm gears and highly efficient helical gearboxes are utilized to drive belt and roller conveyors, ensuring packages move swiftly and accurately without causing acoustic fatigue to warehouse workers.
Material handling in the food industry mandates strict hygiene standards. Conveyors moving meat, poultry, or baked goods require frequent high-pressure washdowns with caustic chemicals. Here, Stainless Steel Worm Gearboxes (such as the SSRV Series) are indispensable. Their smooth, crevice-free surfaces prevent bacterial growth, while the robust sealing technologies protect the internal gearing from water ingress, ensuring compliance with FDA and hygienic design standards.
As material handling moves towards mobile robotics, Automated Guided Vehicles (AGVs) require ultra-compact, high-precision power transmission. High Precision Planetary (TM042) and Harmonic Gearboxes (CF14) are the standard. These reducers offer incredible torque-to-weight ratios, near-zero backlash for precise navigation, and the durability to handle the dynamic loads of moving heavy pallets across warehouse floors.
Our journey is one of continuous evolution and strategic expansion in the power transmission industry.
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and build a solid technical foundation.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions, enabling us to serve more complex industrial needs and establish long-term partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools and automated processes, we now deliver next-generation products that are smarter, more compact, and more energy-efficient, solidifying our position as an industry innovator.
The future of Speed Reducer Gearboxes for Conveyor Systems is deeply intertwined with the principles of Industry 4.0 and smart manufacturing. As industrial facilities strive for zero downtime, the integration of Predictive Maintenance (PdM) technologies into gearboxes is becoming a standard. Modern gear units are increasingly being equipped with smart sensors that continuously monitor vibration signatures, oil temperature, and acoustic emissions. This real-time data is fed into IoT platforms, allowing facility managers to predict bearing wear or gear fatigue long before a catastrophic failure halts the conveyor line.
Another significant trend is the relentless push for Energy Efficiency. Conveyor systems often run 24/7, consuming massive amounts of electricity. To combat this, gearbox manufacturers are optimizing tooth geometry to reduce sliding friction and utilizing advanced synthetic lubricants. When paired with high-efficiency IE4 or IE5 electric motors and Variable Frequency Drives (VFDs), these optimized reducers dramatically lower the total cost of ownership (TCO) and reduce the carbon footprint of material handling operations.
Furthermore, modularity is shaping gearbox design. Plant engineers require versatile solutions that can be easily adapted to different conveyor setups. Modular gearbox systems allow for quick changes in mounting positions, input interfaces, and output shafts, significantly reducing inventory costs for spare parts and minimizing downtime during system upgrades.
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
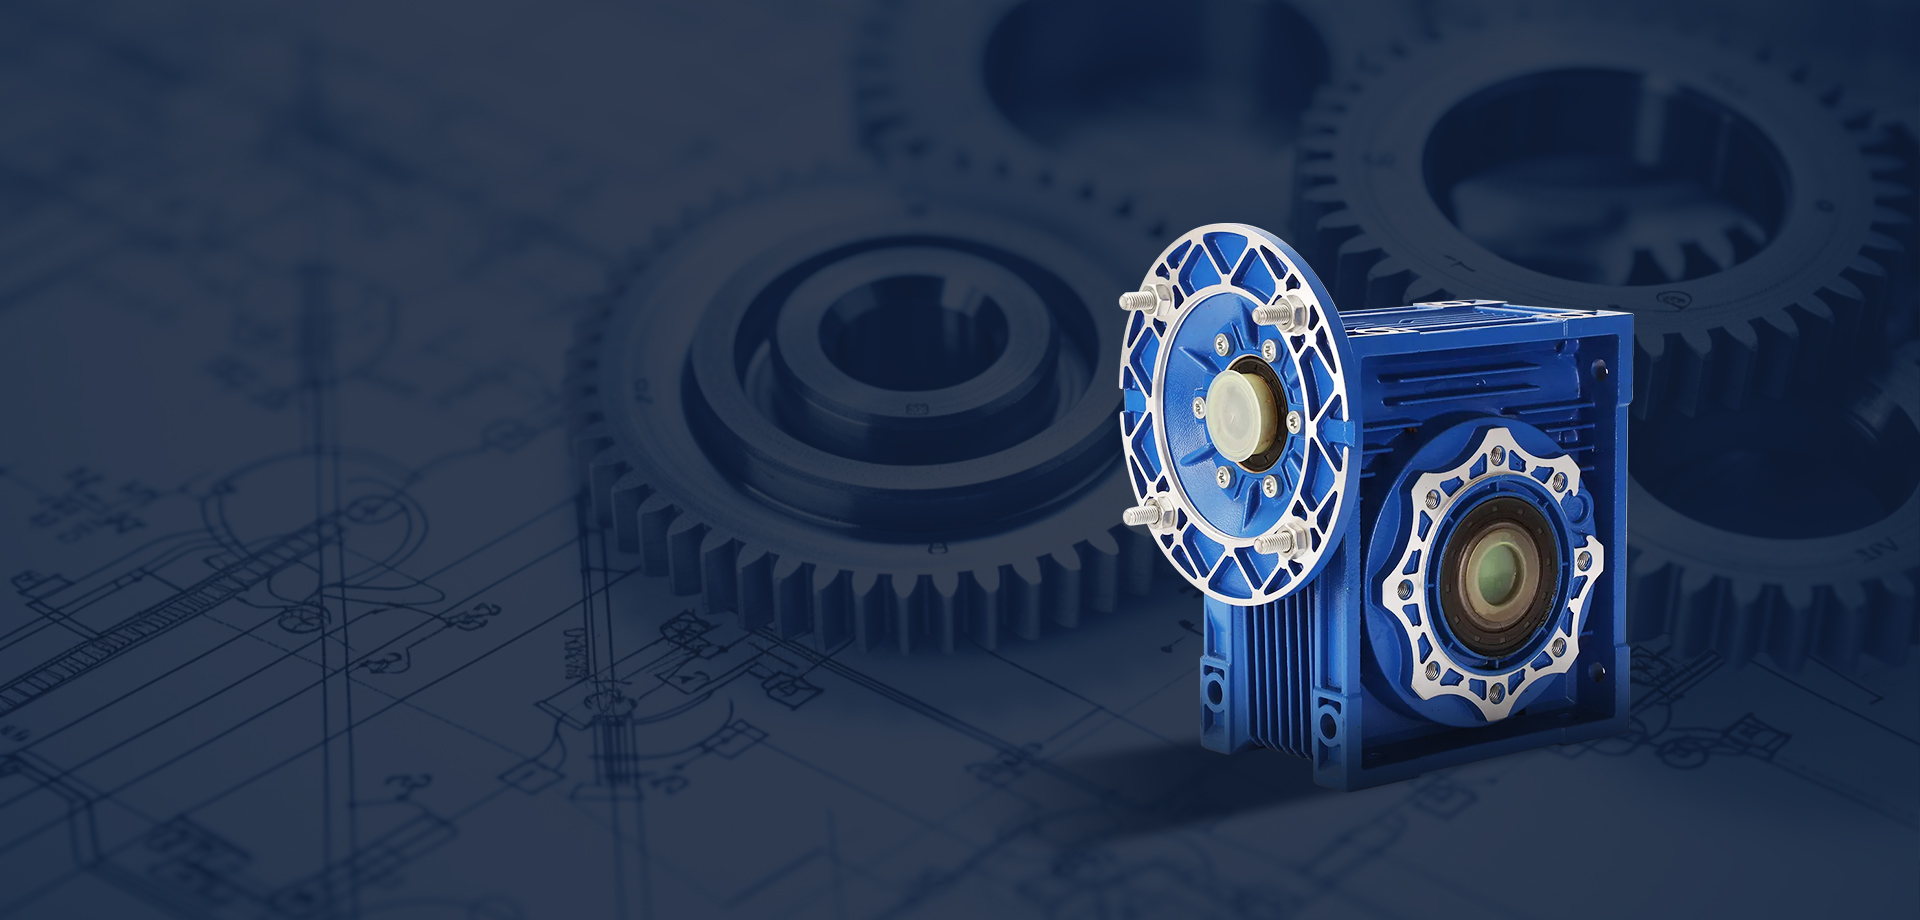
Quality is at the heart of everything we do. Partner with us for reliable material handling solutions.
No diversions—just decades of refining helical, planetary, and parallel-shaft gearboxes for industrial applications.
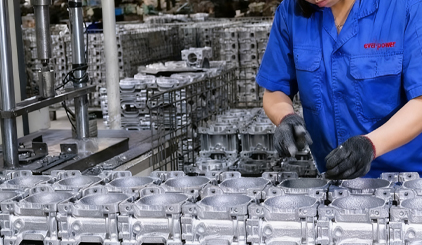
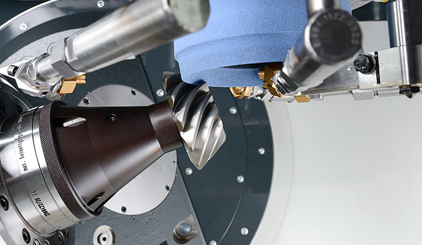
From Gear Forging to Final Assembly. Critical processes like gear grinding, heat treatment, and housing machining are all done under one roof for consistent quality.
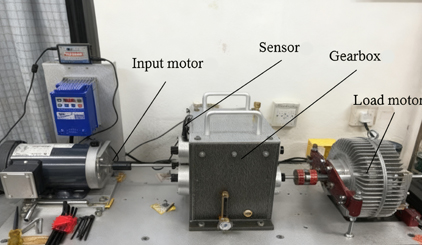
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks—test reports available on request.
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese—because your uptime matters.
Explore our full range of speed reducers, meticulously designed to meet the rigorous demands of global material handling and power transmission applications.
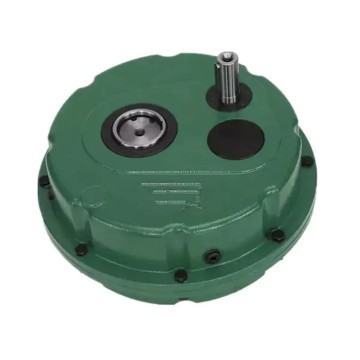 DXG (ATA) Series Shaft-Mounted Gearbox for Conveyor Drives
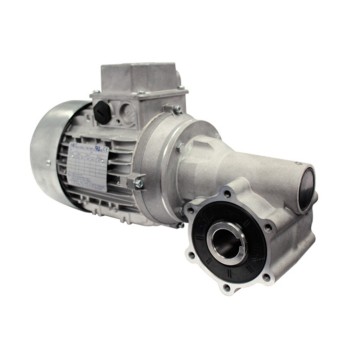 Heavy-Duty Washdown Gearbox for Material Handling
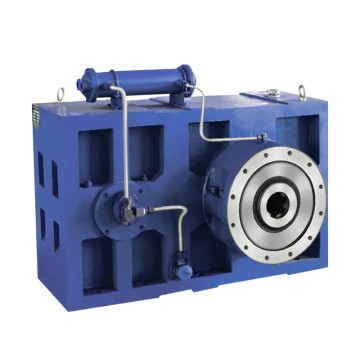 ZLYJ Series High-Torque Extrusion & Conveying Gearbox
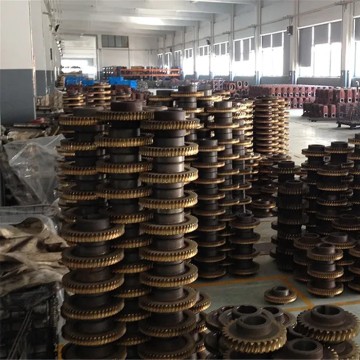 HRV104 Worm Gear Reducer for High-Temp Conveyors
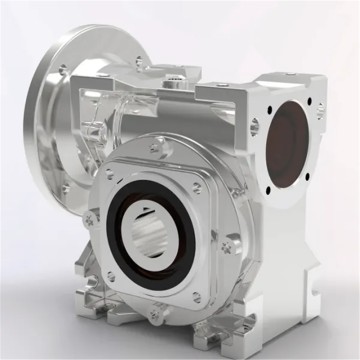 SSRV Series Stainless Steel Gearbox for Food Conveyors
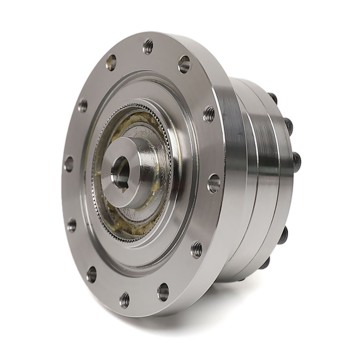 CF14 Precision Harmonic Gearbox for Automated Sorting
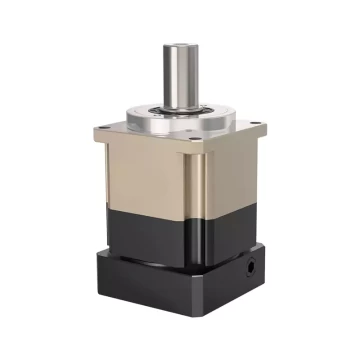 TM042 Planetary Gearbox for AGV Material Handling
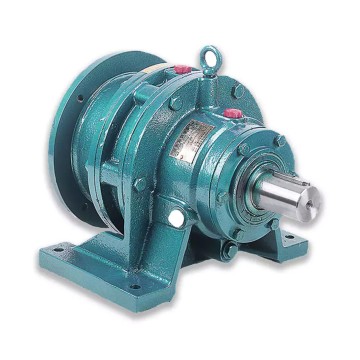 XW/BW Cycloidal Gearbox for Bulk Material Conveyors