Leave Your Message
Explore our most popular gearbox models trusted by packaging and food processing engineers worldwide.
A deep-dive into the technology, market dynamics, and industrial significance of shaft mounted drive solutions.
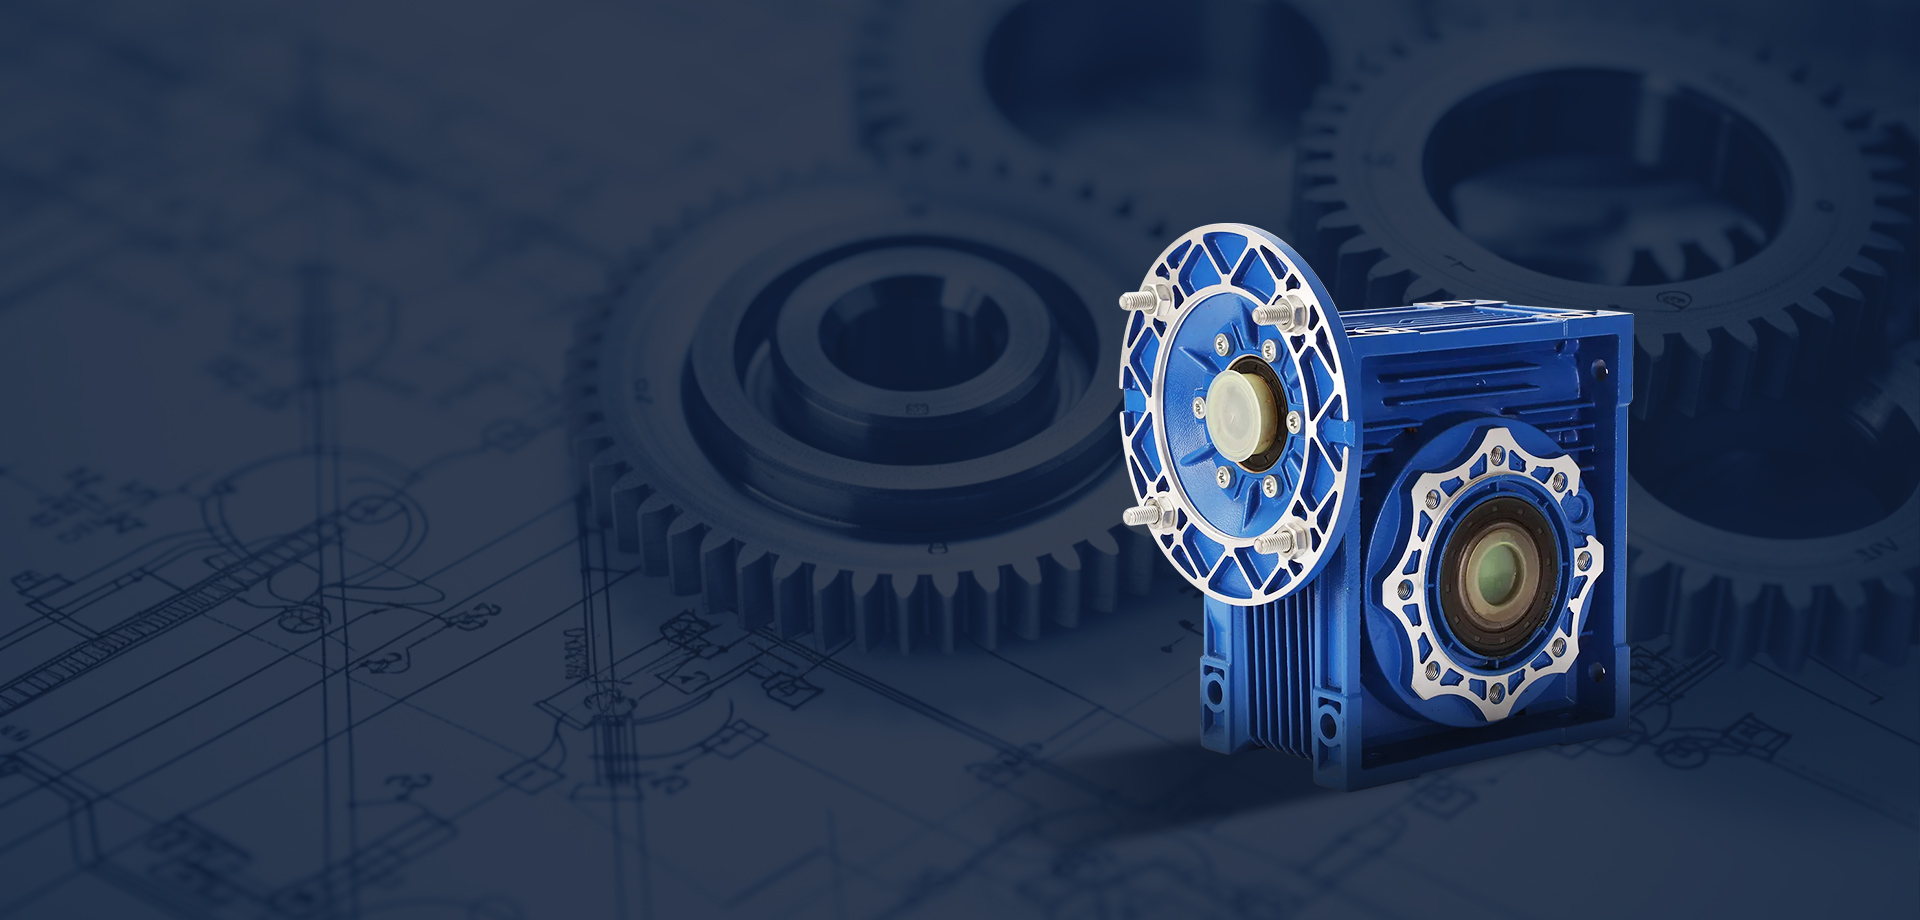
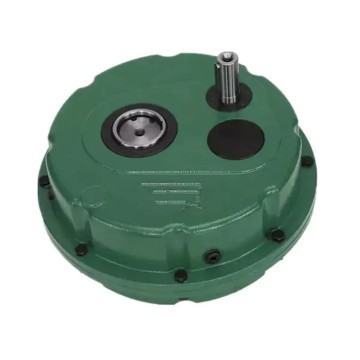
A shaft mounted gearbox is a compact, directly coupled speed reducer that mounts directly onto the driven shaft of a machine — eliminating the need for a separate gearbox baseplate, couplings, or alignment procedures. This elegant engineering approach makes it the preferred power transmission solution across packaging machinery, food and beverage processing lines, conveyor systems, and material handling equipment.
Unlike conventional foot-mounted gearboxes, shaft mounted units use a hollow output bore and a torque arm to absorb reaction forces. The result is a dramatically simplified installation, a smaller footprint, and significantly reduced maintenance overhead — all critical advantages in fast-paced, space-constrained food and packaging facilities.
Shaft mounted gearboxes are the backbone of modern packaging and food processing automation — combining compact design, hygienic construction, and precision torque delivery in a single integrated unit.
The global market for shaft mounted gearboxes in packaging and food processing applications has experienced consistent growth over the past decade, and industry analysts project this trajectory to continue well into the 2030s. Several macro-level forces are driving this expansion:
According to industry research, the food processing equipment market alone is projected to exceed USD 120 billion by 2030, with power transmission components representing a significant and growing segment of total capital expenditure.
Today, shaft mounted gearboxes occupy a well-established and indispensable position within the food and packaging machinery ecosystem. They are routinely specified for:
The dominant gear configurations in this sector include helical and helical-bevel arrangements, valued for their quiet operation, high efficiency, and long service life. Worm gear shaft mounted units remain relevant where very high reduction ratios are needed in a compact package, while planetary configurations are increasingly adopted in servo-driven precision indexing applications.
Technology and market forces are reshaping what packaging and food processing engineers expect from their drive systems.
Next-generation shaft mounted gearboxes are being designed with integrated sensor ports and IoT-compatible housings, enabling real-time vibration, temperature, and oil condition monitoring. Predictive maintenance capabilities are becoming a standard specification request from tier-1 food manufacturers.
IE3 and IE4 motor compatibility, premium helical gear profiles with DIN 6 accuracy class, and advanced synthetic lubricants are enabling shaft mounted gearboxes to achieve lifecycle energy savings of 15–25% compared to previous-generation designs — a key selling point as carbon reduction targets tighten.
EHEDG and 3-A Sanitary Standards are increasingly influencing gearbox housing geometry. Sloped surfaces, smooth radius transitions, IP69K sealing, and FDA-compliant food-grade lubricants are transitioning from premium options to baseline requirements in food zone applications.
Manufacturers are moving toward modular gearbox platforms where a single housing family covers multiple ratio options, mounting configurations, and output shaft types. This dramatically reduces spare parts inventory and lead times for OEM packaging machine builders.
The proliferation of servo-driven packaging machines — particularly in pharmaceutical blister packaging, confectionery wrapping, and portion-controlled food portioning — is driving demand for shaft mounted planetary units with backlash below 3 arcmin and torsional rigidity optimized for dynamic positioning.
Post-pandemic supply chain resilience strategies are prompting food and packaging OEMs to qualify regional gearbox suppliers with full in-house manufacturing capability — reducing dependence on single-source, multi-tier supply chains and improving delivery predictability.
Understanding exactly where and how shaft mounted gearboxes deliver value across packaging and food processing operations.
Flow wrappers operating at 300–1,200 packs per minute demand gearboxes with minimal backlash, high torsional stiffness, and the ability to withstand frequent start-stop cycles. Shaft mounted helical units with anti-shock torque limiters are the preferred solution, providing precise film feed control and consistent seal jaw timing.
In aseptic and ultra-clean filling environments, gearboxes must withstand aggressive CIP (Clean-In-Place) and SIP (Sterilize-In-Place) wash-down cycles. IP69K-rated shaft mounted units with stainless steel external hardware and food-grade H1 lubricants ensure compliance with dairy industry hygiene protocols while maintaining precise fill volume accuracy.
Wet, cold, and chemically aggressive environments in meat processing facilities place extreme demands on gearbox sealing and corrosion resistance. Shaft mounted gearboxes with stainless steel housings, double-lip shaft seals, and NSF H1-certified lubricants provide the reliability required for continuous 24/7 operation in these challenging conditions.
Chocolate and confectionery processing requires extremely precise speed control for consistent product weight and coating thickness. Shaft mounted planetary gearboxes coupled with servo motors provide the sub-arcminute positioning accuracy needed for depositor head indexing and enrobing belt speed synchronization across multi-lane production lines.
The rotational precision required for double-seam can closure demands gearboxes with exceptional concentricity and minimal vibration. Shaft mounted helical-bevel units provide the smooth, consistent torque delivery that ensures hermetic seals across millions of cans per shift in canned food production facilities.
Robotic and conventional palletizers require gearboxes capable of handling high inertia loads, frequent reversals, and variable duty cycles. Shaft mounted units with reinforced output bearings and thermally optimized housings are specified for layer-forming conveyors, pallet elevators, and stretch wrapper turntable drives.
A Legacy of Growth & Innovation
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and establish a solid technical foundation that would support decades of growth.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions, enabling us to serve more complex industrial needs — including specialized shaft mounted gearboxes for food and packaging machinery — and establish long-term OEM partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools, automated CNC machining centers, and rigorous quality management systems, we now deliver next-generation products that are smarter, more compact, and more energy-efficient — solidifying our position as an industry innovator in precision gearbox manufacturing.
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
Every shaft mounted gearbox we produce undergoes a comprehensive, multi-stage quality assurance process before it reaches your production line.
Quality is at the heart of everything we do — and our track record in packaging and food processing applications proves it.
No diversions — just decades of refining helical, planetary, and shaft mounted gearboxes for demanding industrial applications including packaging and food processing.
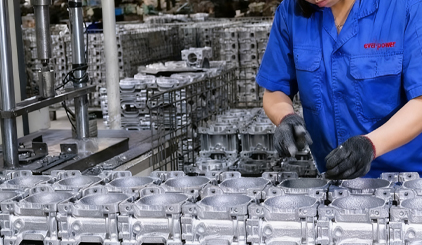
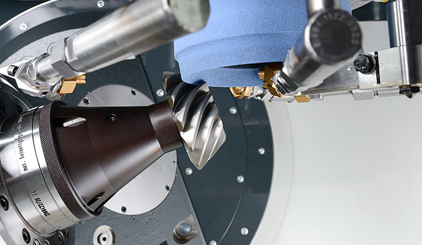
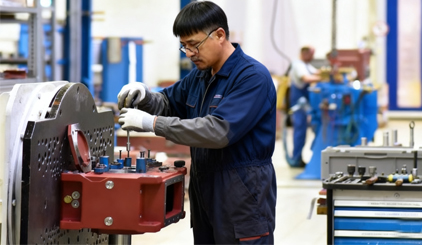
Critical processes including gear grinding, heat treatment, housing machining, and final assembly are all performed under one roof — ensuring consistent quality at every stage.
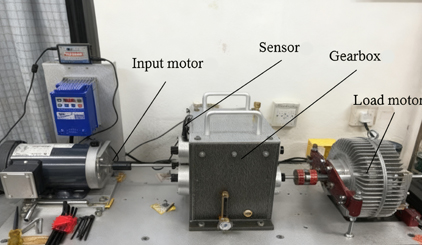
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks — detailed test reports available on request for full traceability.
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese — because your production uptime is our priority.
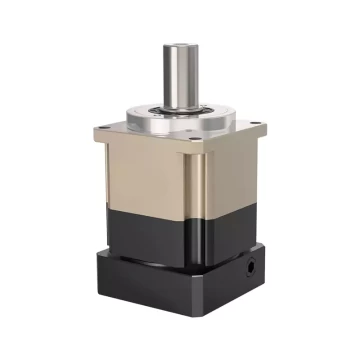
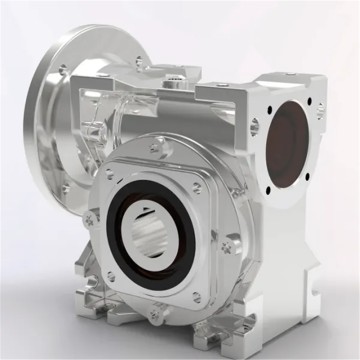
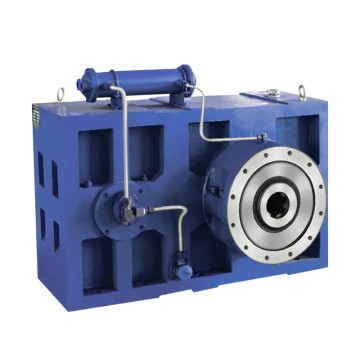
From shaft mounted drives to precision planetary reducers — explore our full portfolio of industrial gearbox solutions for packaging, food processing, and beyond.
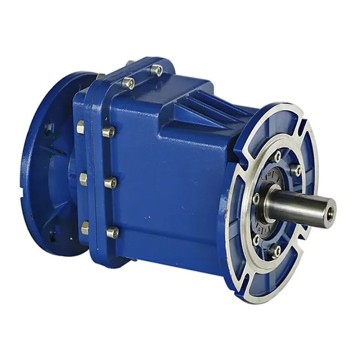
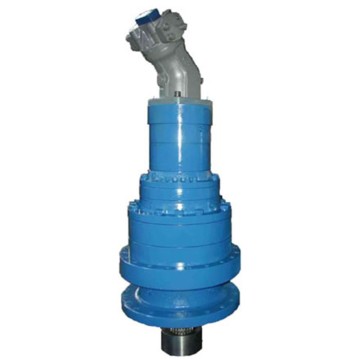
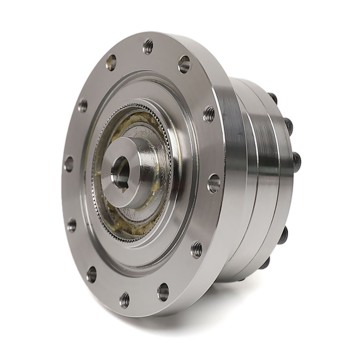
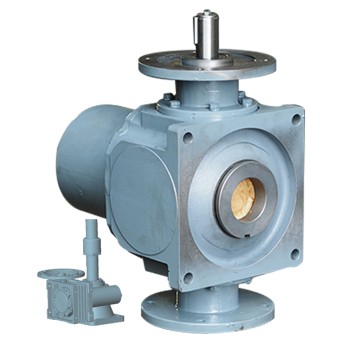
Connect with our engineering team to discuss the right shaft mounted gearbox specification for your application. We provide technical consultation, custom ratio selection, and fast global delivery.
Explore Shaft Mounted Gearboxes →