Leave Your Message
High-performance drive technologies tailored for precise material handling and continuous conveyor operations.
Analyzing the critical role of industrial gearboxes in driving global supply chains and heavy-duty conveyor systems.
In today’s hyper-connected global economy, the efficiency of supply chains relies entirely on the seamless operation of material handling and conveyor systems. As premier industrial gearbox manufacturers, we recognize that the gearbox is the undisputed heart of these mechanical arteries. From colossal mining operations moving thousands of tons of raw ore per hour to sophisticated e-commerce fulfillment centers sorting millions of parcels daily, the demand for robust power transmission has never been higher. The global industrial gearbox market is experiencing a paradigm shift, driven by the relentless pursuit of higher torque density, reduced footprint, and ultimate reliability. Modern material handling requires continuous, 24/7 operation where downtime is measured not just in lost minutes, but in tens of thousands of dollars in lost revenue. Consequently, manufacturers are transitioning away from generic, off-the-shelf reducers toward application-specific drive solutions engineered to withstand punishing radial loads, extreme temperature fluctuations, and continuous start-stop cycles.
The contemporary commercial landscape dictates that energy efficiency is no longer an optional upgrade but a regulatory and economic necessity. Conveyor systems are notoriously energy-intensive. By integrating high-efficiency helical and planetary gearboxes, facilities can dramatically reduce their power consumption. Furthermore, the integration of precision engineering ensures minimal backlash and superior load distribution across gear teeth, translating to whisper-quiet operations and significantly extended service life. This focus on Total Cost of Ownership (TCO) is reshaping how procurement managers and facility engineers select their power transmission partners.
Exploring how specialized gearbox designs solve complex challenges across diverse industrial sectors.
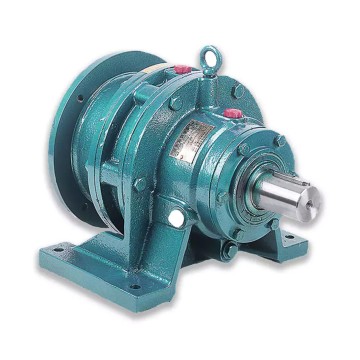
In the unforgiving environments of mining and quarrying, overland conveyor systems span miles, transporting heavy, abrasive materials. Gearboxes in these applications face extreme shock loads, heavy dust ingress, and harsh weather conditions. Solutions like our robust Cycloidal and Helical gearboxes are engineered with reinforced cast-iron housings, oversized bearings, and specialized sealing systems (such as taconite seals) to prevent contamination. The ability to deliver massive torque at low speeds ensures that even fully loaded belts can be started smoothly without catastrophic mechanical failure or belt snapping.
Material handling in the food and beverage industry presents a completely different set of challenges. Strict hygiene regulations mandate that conveyor systems undergo rigorous, high-pressure, high-temperature washdowns using caustic cleaning chemicals. Here, our SSRV Series Stainless Steel Worm Gearboxes shine. Designed with smooth, crevice-free surfaces that prevent bacterial pooling, these gearboxes eliminate the risk of contamination. Furthermore, they are lubricated with food-grade oils (H1 certified) and utilize advanced O-rings and lip seals to ensure zero leakage, maintaining the absolute integrity of the production line.
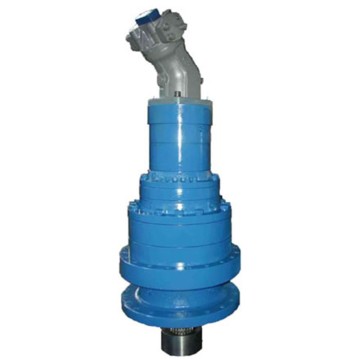
The e-commerce boom has revolutionized warehouse logistics. High-speed cross-belt sorters, roller conveyors, and AGVs require rapid acceleration, deceleration, and absolute precision. High Precision Harmonic and Planetary Gearboxes are deployed here due to their exceptional torque-to-weight ratios and near-zero backlash. In AGV wheel drives, compact design is paramount to maximize battery space while delivering enough power to move heavy pallets. The dynamic responsiveness of these gearboxes allows automated systems to navigate tight warehouse aisles with millimeter accuracy.
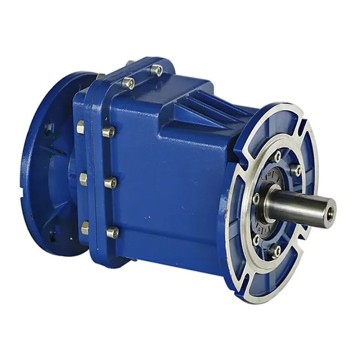
Airport BHS require absolute reliability; a stalled conveyor means missed flights and severe operational bottlenecks. Gearboxes in these systems must operate continuously with low noise levels to maintain a comfortable environment for passengers and staff. High-efficiency helical gear units are typically utilized, often paired with Variable Frequency Drives (VFDs) to adjust belt speeds dynamically based on passenger volume, thereby optimizing energy usage while ensuring smooth luggage transition through security scanners and sorting carousels.
Embracing Industry 4.0, IoT integration, and sustainable manufacturing in gearbox technology.
As we look to the future, the role of industrial gearbox manufacturers is evolving from pure mechanical engineering to mechatronics and digital integration. The most prominent trend is the advent of the "Smart Gearbox." By embedding IoT (Internet of Things) sensors directly into the gearbox housing, operators can monitor real-time data on vibration frequencies, oil temperature, acoustic emissions, and load variations. This data is fed into centralized cloud platforms where AI algorithms predict potential failures weeks before they occur. This shift from reactive maintenance to predictive maintenance drastically reduces unplanned downtime in critical material handling systems.
Another significant trend is the pursuit of sustainability through advanced metallurgy and tribology. Manufacturers are exploring lighter, high-strength alloys and advanced surface treatments (such as carbon-nitriding) to reduce the physical weight of the gearbox without compromising torque capacity. Lighter gearboxes reduce the structural load on conveyor frames and require less energy to operate. Additionally, the development of synthetic, ultra-low-friction lubricants is extending maintenance intervals from months to years, creating "lubricated-for-life" solutions that minimize environmental impact and maintenance costs.
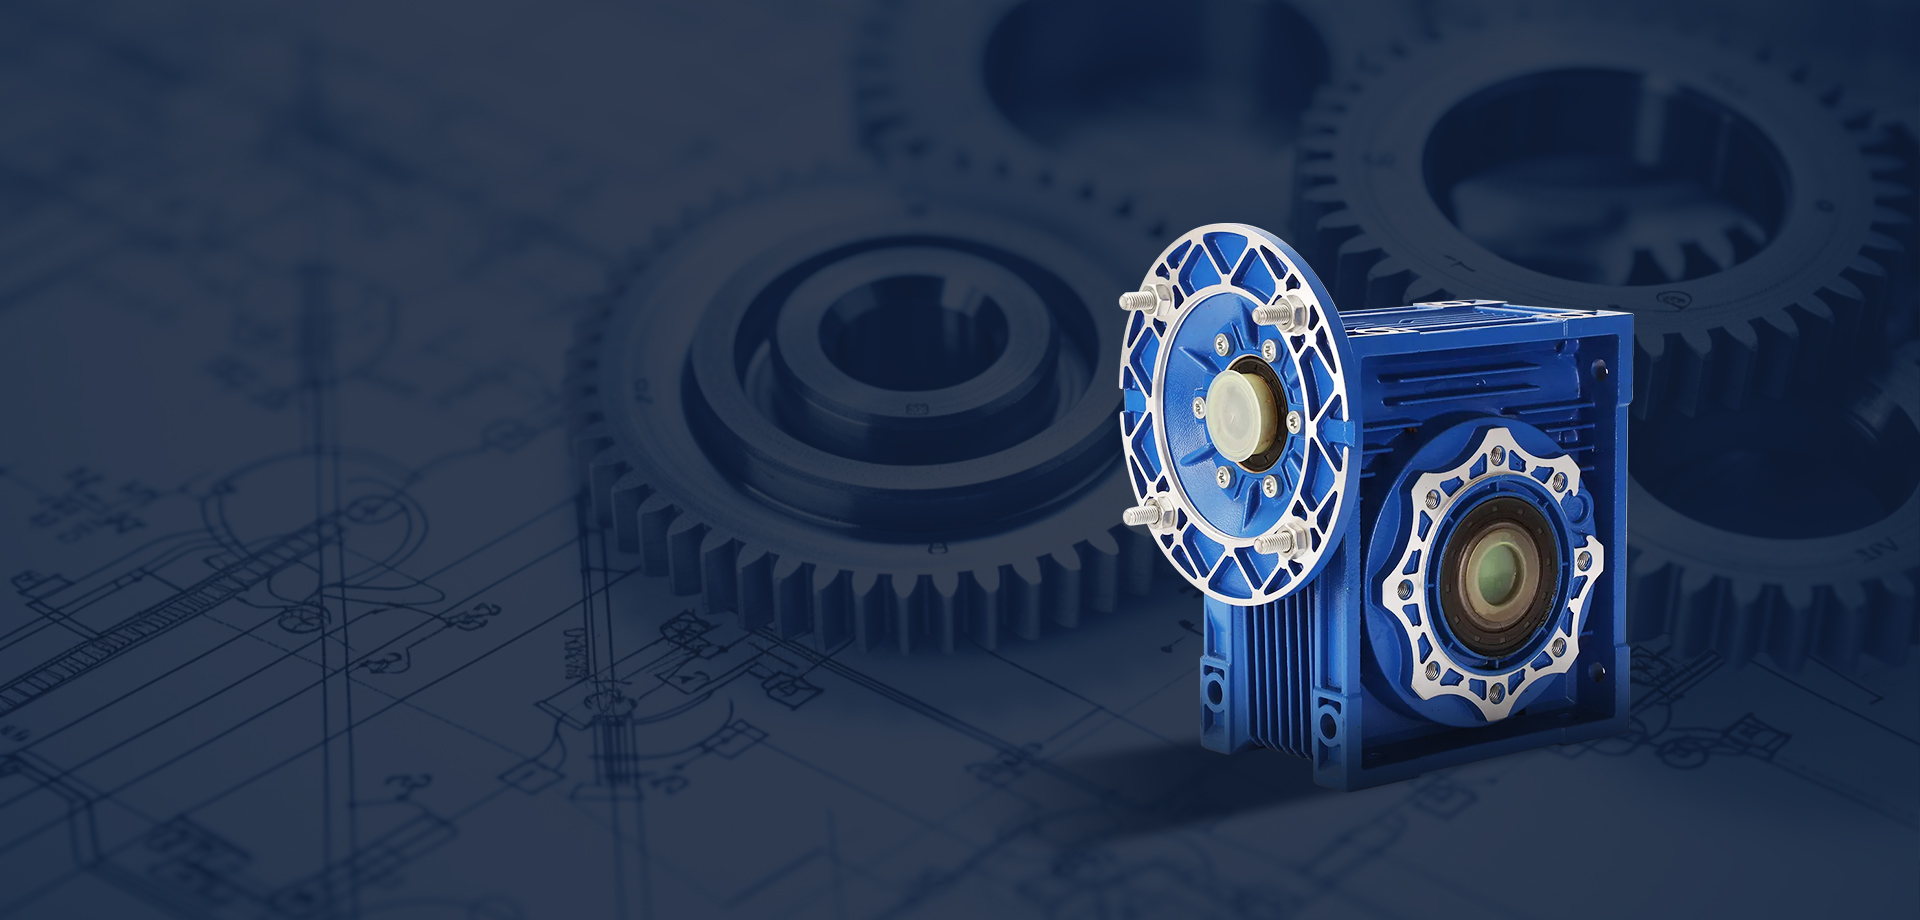
Finally, modularity is becoming a key design philosophy. Conveyor system builders require flexibility. Modern gearboxes are designed with modular input and output flanges, allowing a single base unit to be adapted for solid shafts, hollow shafts, shrink discs, or direct motor mounts. This modularity reduces inventory costs for distributors and accelerates delivery times for end-users, ensuring that the right power transmission solution is always available when a critical conveyor system needs it.
A Legacy of Growth & Innovation
Our journey is one of continuous evolution and strategic expansion.
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and build a solid technical foundation.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions, enabling us to serve more complex industrial needs and establish long-term partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools and automated processes, we now deliver next-generation products that are smarter, more compact, and more energy-efficient, solidifying our position as an industry innovator.
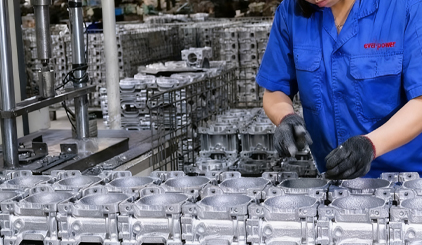
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
Quality is at the heart of everything we do
Explore our full range of industrial gearboxes engineered to optimize every stage of your conveyor and logistics systems.