Leave Your Message
High-performance gearboxes engineered for demanding mining and heavy equipment applications
An industrial gearbox is a mechanical power transmission device that transfers rotational energy from a prime mover — such as an electric motor or diesel engine — to driven machinery, modifying torque and speed to match the specific requirements of the application. In mining and heavy equipment sectors, gearboxes are the critical backbone of virtually every driven system, from massive conveyor belts transporting thousands of tons of ore per hour to the rotary drives of tunnel boring machines cutting through solid rock.
Unlike gearboxes used in light or moderate-duty applications, industrial gearboxes for mining must withstand continuous shock loads, extreme ambient temperatures, heavy dust, moisture ingress, and corrosive environments — all while delivering reliable, maintenance-friendly performance over years of around-the-clock operation.
The global industrial gearbox market is experiencing robust growth, driven primarily by expanding mining operations in Asia-Pacific, Latin America, and Africa, alongside surging demand for construction and infrastructure development worldwide. According to industry analysts, the industrial gearbox market was valued at over USD 28 billion in 2023 and is projected to surpass USD 42 billion by 2030, with the mining and heavy equipment segment accounting for a significant share of this expansion.
Key commercial drivers include:
Chinese manufacturers have become globally competitive in this space, offering ISO-certified, precision-engineered gearboxes at highly competitive price points, serving OEMs and end users across more than 80 countries. Our company, established in 2002, is a prime example of this transformation — combining rigorous quality standards with full in-house production capabilities to deliver world-class industrial gearboxes for mining and heavy equipment.
The industrial gearbox sector is evolving rapidly — here are the key trends shaping the future
Integration of IoT sensors and vibration analysis systems directly into gearbox housings allows real-time monitoring of temperature, oil quality, and gear mesh health — enabling predictive maintenance and eliminating unplanned downtime in critical mining operations.
Advanced helical and planetary gear profiles with optimized contact ratios and micro-geometry corrections are achieving transmission efficiencies above 98%, directly reducing energy consumption and operating costs in high-power mining drives.
Modern planetary and multi-stage helical gearboxes deliver unprecedented power density — enabling the same torque output in a package 30–40% smaller and lighter than traditional designs, critical for mobile mining equipment and underground applications.
Closed-loop oil circulation, synthetic lubricants with extended service intervals, and sealed-for-life designs are reducing environmental impact and maintenance frequency in remote mining sites where lubricant changes are costly and logistically challenging.
Modular gearbox platforms allow rapid customization of gear ratios, shaft configurations, mounting arrangements, and accessory packages — shortening lead times and reducing spare parts inventory for mining operators managing diverse equipment fleets.
Multi-stage labyrinth seals, pressurized housing designs, and IP69K-rated enclosures are becoming standard for gearboxes operating in wet, dusty, or chemically aggressive mining environments, dramatically extending service life.
Industrial gearboxes serve as the critical power link across every major mining and heavy equipment system
Belt conveyors are the arteries of any mining operation, moving ore from the face to the processing plant continuously. High-torque helical or shaft-mounted gearboxes with torque arm mounting are the preferred solution — offering smooth soft-start capability, high radial load capacity, and minimal installation footprint directly on the conveyor shaft. In large coal mines, a single conveyor system may require gearboxes handling over 500 kW with gear ratios from 20:1 to 100:1.
Among the largest machines on earth, bucket wheel excavators require massive slew ring drives and bucket wheel drives with extreme shock load tolerance. Planetary gearboxes with hardened and ground internal gears are essential here, delivering the torque multiplication needed to rotate bucket wheels weighing hundreds of tonnes while absorbing the impact loads of continuous rock and soil cutting.
Grinding mills in mineral processing plants represent some of the highest-power gearbox applications in industry, with single pinion and dual pinion drives handling motors from 1 MW to over 20 MW. These gearboxes must deliver exceptional reliability over multi-year service intervals, as unplanned mill stoppages cost mining companies tens of thousands of dollars per hour in lost production.
Excavators, motor graders, compactors, and asphalt pavers all rely on robust travel drives and swing drives. Compact planetary gearboxes integrated into final drive assemblies provide the torque and speed reduction needed to propel heavy machines across rough terrain while withstanding the continuous shock and vibration inherent in earthmoving operations.
Mining hoists, overhead cranes, and shiploader cranes demand gearboxes with precise speed control, high holding torque, and fail-safe braking integration. Cycloidal and helical-bevel gearboxes are widely used in these applications due to their high reduction ratios in compact form factors and inherent shock absorption characteristics that protect both the drive and the load.
Dewatering pumps, ventilation fans, and slurry pumps are mission-critical in underground mining. Gearboxes for these applications must handle continuous duty cycles, resist moisture and chemical attack, and maintain precise speed ratios to optimize pump and fan efficiency. Parallel-shaft and right-angle helical-bevel gearboxes are commonly specified for these demanding continuous-duty pump drives.
Selecting the correct industrial gearbox for a mining or heavy equipment application requires careful analysis of multiple engineering parameters. Incorrect specification is one of the most common causes of premature gearbox failure in mining operations — resulting in costly unplanned downtime and expensive replacement parts.
In the mining industry, the initial purchase price of a gearbox represents only a fraction of its total cost of ownership (TCO). Maintenance costs, energy losses, spare parts, and the cost of downtime during replacement can easily exceed the original equipment cost many times over during a typical 10–20 year service life.
Investing in a premium, properly specified gearbox from a quality manufacturer delivers measurable TCO advantages: higher efficiency reduces energy bills by thousands of dollars annually in large drives; longer service intervals reduce maintenance labor; superior reliability eliminates the catastrophic cost of unplanned mill or conveyor stoppages. Our customers in the mining sector consistently report that upgrading to our precision-engineered gearboxes delivers full payback within 12–24 months through reduced maintenance and energy savings alone.
We invest in world-class technology to ensure every product that leaves our facility is built to excel
Four pillars that make us the preferred industrial gearbox partner for mining and heavy equipment worldwide
No diversions — just decades of refining helical, planetary, and parallel-shaft gearboxes for industrial applications. Our singular focus means unmatched depth of engineering expertise for mining and heavy equipment gearbox challenges.
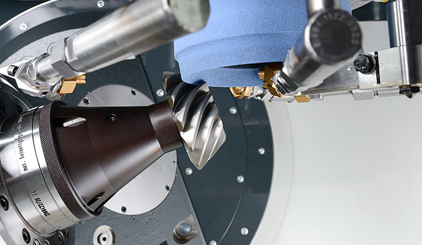
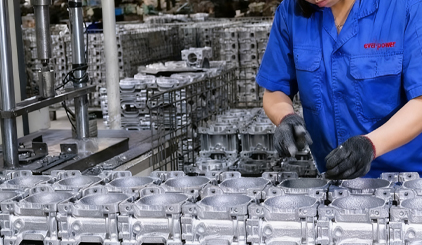
Critical processes like gear grinding, heat treatment, and housing machining are all done under one roof for consistent quality. Full vertical integration eliminates supply chain variability — every component meets our exact specifications.
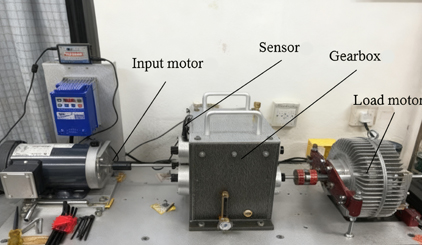
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks — test reports available on request. Mining customers receive documented proof of performance before equipment even leaves our facility.
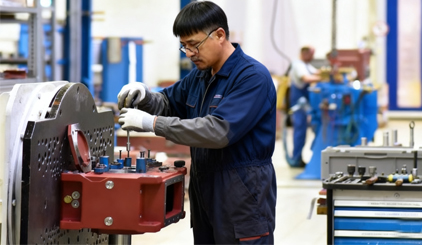
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese — because your uptime matters. Mining operations run 24/7, and so does our commitment to keeping your equipment running.
A Legacy of Growth & Innovation
Our engineering team is ready to help you select, configure, and commission the ideal industrial gearbox for your mining or heavy equipment application. Contact us today for a technical consultation and competitive quotation.
Explore Our Full Gearbox Range →Explore our comprehensive range of gearboxes for mining, heavy equipment, and industrial applications