Leave Your Message
Explore our precision-engineered gearbox series designed for the unique demands of packaging lines and food processing machinery.
In the highly competitive world of packaging and food processing, every component on the production line must meet uncompromising standards of precision, hygiene, efficiency, and reliability. Among all mechanical drive components, the helical gearbox has emerged as the industry's benchmark solution — offering a unique combination of smooth torque transmission, low operational noise, high mechanical efficiency, and compact design that perfectly suits the demands of modern automated packaging lines and food-grade processing environments.
Unlike spur gears, helical gears feature angled teeth that engage progressively, distributing load across multiple teeth simultaneously. This design dramatically reduces vibration and noise — both critical in food facilities where hygiene standards and operator safety are paramount. With efficiencies reaching up to 98%, helical gearboxes minimize energy waste, reduce operating costs, and support sustainability goals that are increasingly demanded by global food brands and packaging companies.
From high-speed horizontal flow wrapping machines and vertical form-fill-seal systems to continuous conveying lines, mixing equipment, slicing machines, and labeling stations, helical gearboxes provide the controlled, reliable drive force that keeps modern food production running 24/7.
Engineered to outperform in the most demanding packaging and food processing environments.
Helical gear geometry enables progressive tooth engagement, achieving transmission efficiencies of up to 98%. This reduces energy consumption, lowers motor load, and delivers long-term cost savings on high-duty-cycle packaging and food processing lines.
Gradual tooth meshing across the full helical profile produces significantly lower noise levels compared to spur gears. Critical for food processing facilities where operator comfort, hygiene, and precision motion control demand quiet, smooth operation.
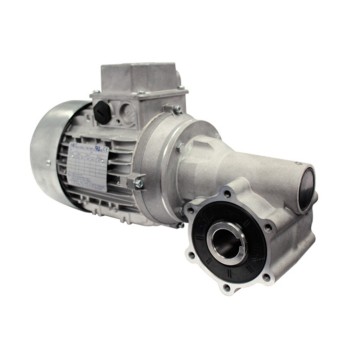
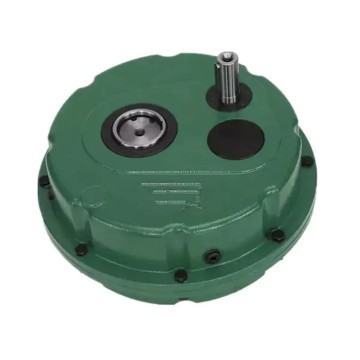
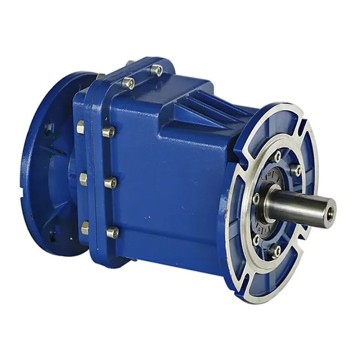
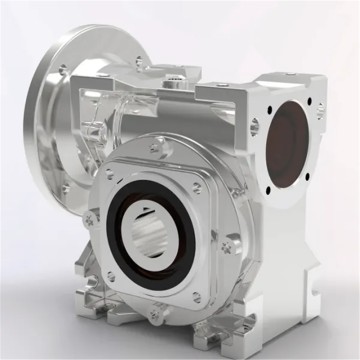
Available in inline, parallel-shaft, right-angle, and foot/flange-mounted configurations, helical gearboxes integrate seamlessly into conveyors, filling machines, sealing equipment, labelers, and other space-constrained packaging line modules.
Stainless steel housings, food-grade lubricants, IP67/IP69K ingress protection, and smooth, crevice-free exterior surfaces ensure full compliance with FDA, EHEDG, and other international food safety standards for direct and indirect food contact zones.
The helical tooth profile distributes load across a larger contact area, enabling higher torque transmission within a smaller housing footprint — ideal for heavy-duty packaging presses, bottle filling carousels, and industrial mixers operating under continuous load.
Precision-ground gear teeth, high-quality sealed bearings, and robust housing materials ensure service lives of 30,000+ hours with minimal maintenance. Lifetime-lubricated sealed units further reduce planned maintenance downtime on continuous production lines.
The global helical gearbox market for packaging and food processing machinery is experiencing robust growth, driven by automation, sustainability, and digital transformation.
The global industrial gearbox market is projected to surpass USD 35 billion by 2030, with the food processing and packaging machinery segment accounting for a significant and growing share. Rising consumer demand for packaged and processed food products, accelerated by urbanization and e-commerce growth in Asia-Pacific, Latin America, and Africa, is driving unprecedented investment in automated packaging lines — and with it, surging demand for precision helical gearboxes. Major food brands and contract packaging companies worldwide are retrofitting legacy lines and commissioning entirely new automated facilities, placing helical gearboxes at the center of this industrial wave.
Modern helical gearboxes are increasingly designed with embedded IoT sensors for real-time vibration monitoring, temperature tracking, and predictive maintenance alerts. Integration with industrial control systems (PLC, SCADA) enables fully automated production lines where gearbox health data feeds directly into maintenance scheduling, minimizing unplanned downtime and maximizing OEE (Overall Equipment Effectiveness) on continuous food packaging operations.
Tightening energy efficiency regulations in Europe (IE3/IE4 motor integration), North America, and increasingly Asia are pushing food processors to replace aging worm gearboxes with high-efficiency helical units. The energy savings — often 20-40% per unit — translate directly to lower carbon footprints and compliance with ESG commitments. Helical gearboxes with IE4-compatible input flanges are rapidly becoming the preferred specification for new-build food factories seeking LEED certification or carbon-neutral production targets.
Post-pandemic food safety awareness and increasingly stringent regulatory frameworks (FDA 21 CFR, EU 1935/2004, FSMA, HACCP) are raising the bar for gearbox hygiene design in direct food contact zones. Demand for smooth-body stainless steel helical gearboxes with IP69K wash-down protection, NSF-H1 certified lubricants, and removable drain plugs has accelerated significantly, particularly in meat processing, dairy, beverage bottling, and fresh produce packaging applications.
Global supply chain disruptions have accelerated the diversification of gearbox sourcing strategies among major OEMs and food processing companies. Chinese manufacturers like HZPT — offering globally certified, competitively priced helical gearboxes with short lead times, full customization capability, and local warehousing in key markets — are capturing increasing market share from traditional European suppliers, particularly in Southeast Asia, Middle East, and South American growth markets.
Helical gearboxes power a vast spectrum of critical functions across the packaging and food processing value chain.
In horizontal flow wrap machines (HFFS) and vertical form-fill-seal (VFFS) systems operating at speeds of 100–600 packs per minute, helical gearboxes drive film-feeding rollers, cross-sealing jaw mechanisms, and product infeed conveyors. The smooth, shock-free torque delivery of helical gears is essential here — any vibration or torque spike can compromise seal integrity, cause film breakage, or damage delicate food products. Compact inline helical gearboxes with precise gear ratios allow OEM machine builders to achieve the exact film feed speeds required for different packaging formats without motor resizing.
Rotary filling carousels for bottled water, carbonated drinks, juices, and dairy products require helical gearboxes to drive the main carousel turntable, star-wheel transfer mechanisms, and capping head spindles. The high rotational inertia of large-diameter carousels demands gearboxes with superior torque capacity and zero backlash for precise bottle positioning at each fill station. Stainless steel helical gearboxes with food-grade IP69K wash-down protection are mandatory in CIP (Clean-in-Place) bottling environments where daily high-pressure hot water cleaning is standard practice.
Band saw systems, deboning lines, slicing machines, and portioning equipment in meat and seafood processing facilities impose unique demands: high starting torques, frequent speed changes, and extremely aggressive wash-down cleaning with chlorine-based disinfectants. Helical gearboxes with corrosion-resistant stainless steel or coated aluminum housings, oversized sealed bearings, and USDA-accepted NSF-H1 lubricants are specified for these applications. The ability to deliver precise speed control during slicing operations is critical for consistent product weight and yield optimization.
Industrial bread and pastry lines incorporate helical gearboxes in dough mixing drives, dough sheeting roller trains, baking oven conveyor systems, and decorating/depositing equipment. Sugar-based and dough environments create sticky contamination risks that demand easy-clean smooth-body gearbox housings. Variable-speed helical gearbox-motor combinations allow bakers to fine-tune dough processing speeds for different product recipes without mechanical adjustments, supporting faster product changeovers on multi-product lines.
Downstream from primary packaging, helical gearboxes power high-precision label applicator heads, case erectors, case packing robots, palletizer drives, and stretch wrapping machines. In label applicators, positioning accuracy within ±0.5mm is required for correct label placement — achievable only with low-backlash helical gearboxes. Palletizer column lift drives demand high-torque helical units capable of handling loads up to several tons while maintaining smooth, jerk-free vertical movement to prevent product damage.
Across all food processing and packaging facilities, helical gearboxes are the preferred drive for belt conveyors, roller conveyors, screw conveyors, and bucket elevators. The high efficiency and compactness of helical gear units allow conveyor designers to minimize gearmotor sizes while meeting torque requirements, reducing capital and energy costs. Multi-stage helical gearboxes enable wide speed ratio ranges (up to 400:1 in three-stage units) that cover the full speed spectrum from slow accumulation conveyors to high-speed merge/divert sorters.
Precise film feed and sealing jaw drives at 600+ packs/min with zero vibration and reliable seal integrity.
IP69K stainless steel helical gearboxes for rotary carousels, capping heads, and CIP wash-down zones.
High-torque, corrosion-resistant gearboxes with NSF-H1 lubrication for hygienic protein processing lines.
Variable-speed helical drives for dough mixers, sheeters, and oven conveyors with easy recipe changeover.
Low-backlash helical gearboxes ensuring ±0.5mm label positioning accuracy at high throughput speeds.
Multi-stage helical gear units for belt conveyors, bucket elevators, and high-load palletizer column drives.
HZPT helical gearboxes serve a broad spectrum of industries beyond food and packaging — delivering the same precision and reliability wherever power transmission matters.
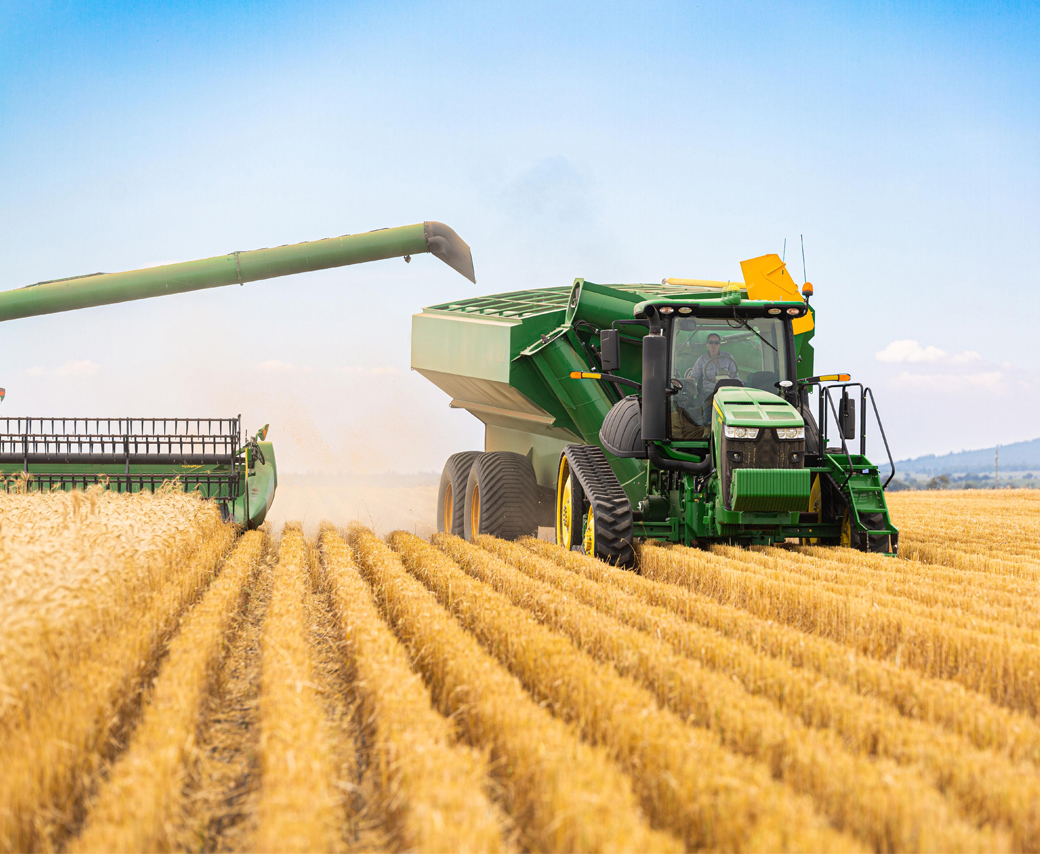
No diversions — just decades of refining helical, planetary, and parallel-shaft gearboxes for agricultural applications including tractors, harvesters, and irrigation pump drives demanding extreme durability under variable field conditions.
Read more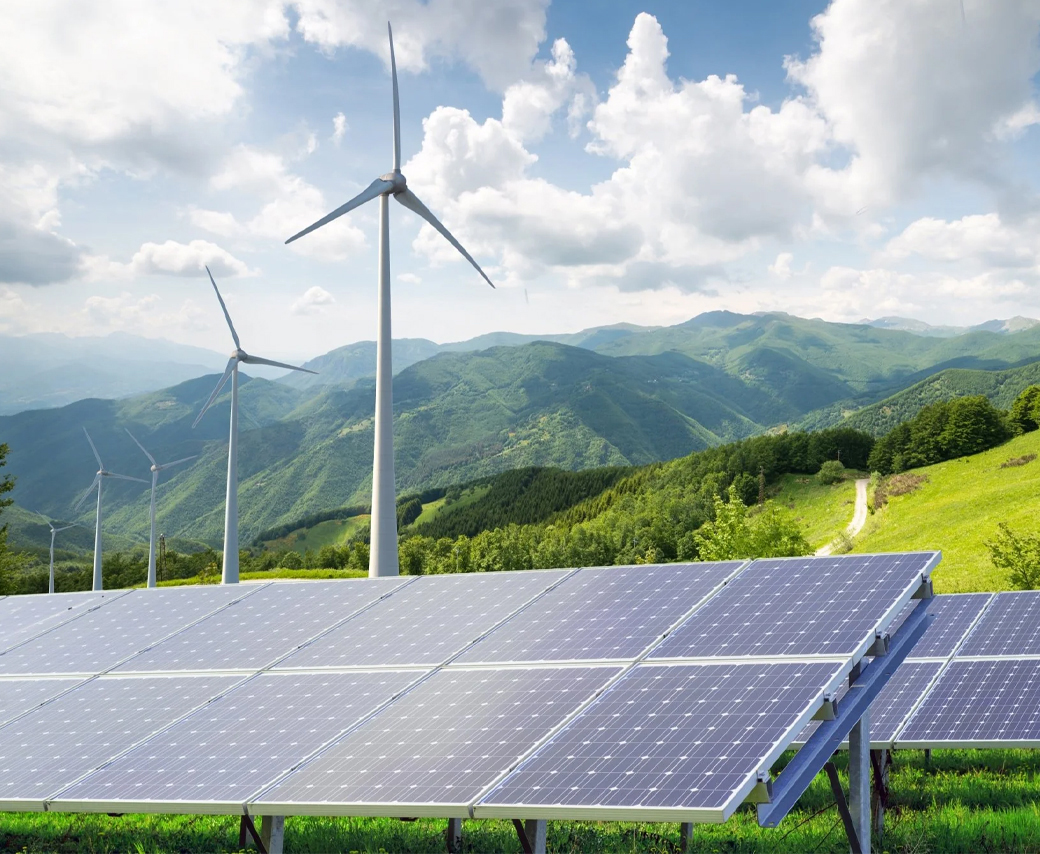
Planetary gearboxes are at the heart of wind turbine systems, driving yaw and pitch mechanisms that optimize blade angle and nacelle orientation. Built for 20+ years of maintenance-free operation in extreme environments.
Read more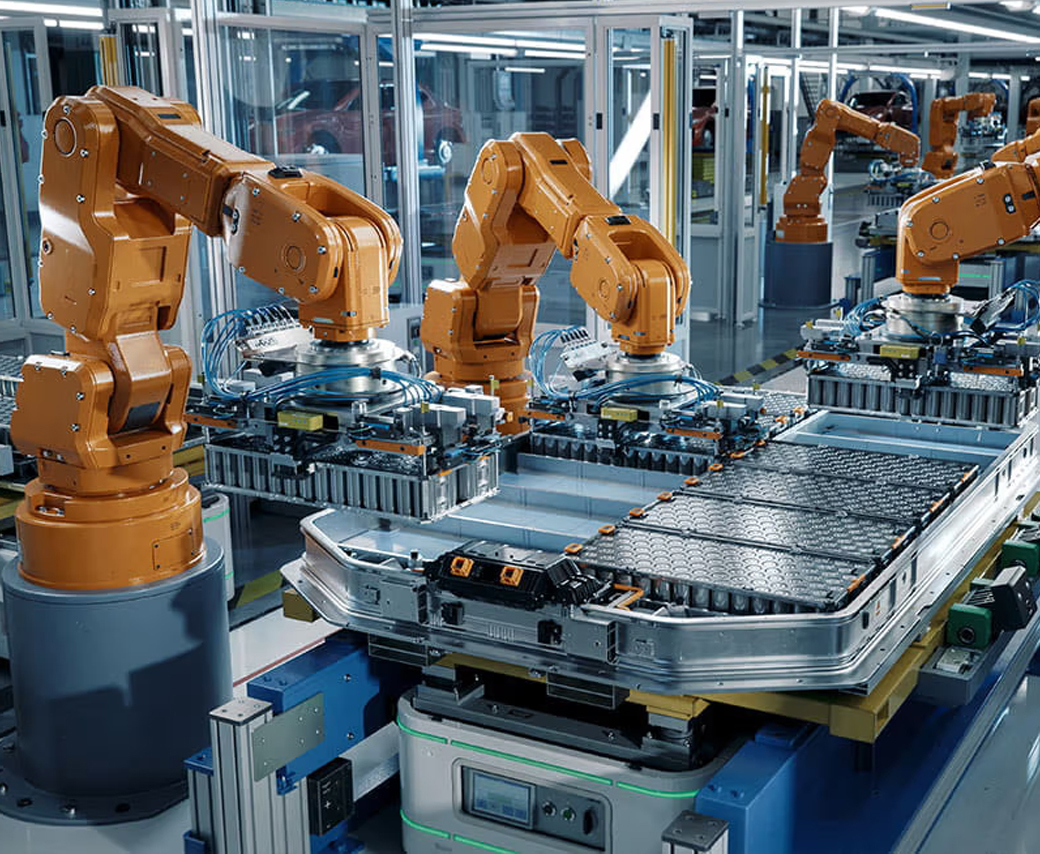
From robotic arms to high-speed CNC lathes and machining centers, our low-backlash planetary gearboxes ensure micron-level positioning accuracy, smooth motion control, and long-term repeatability in automated production lines.
Read more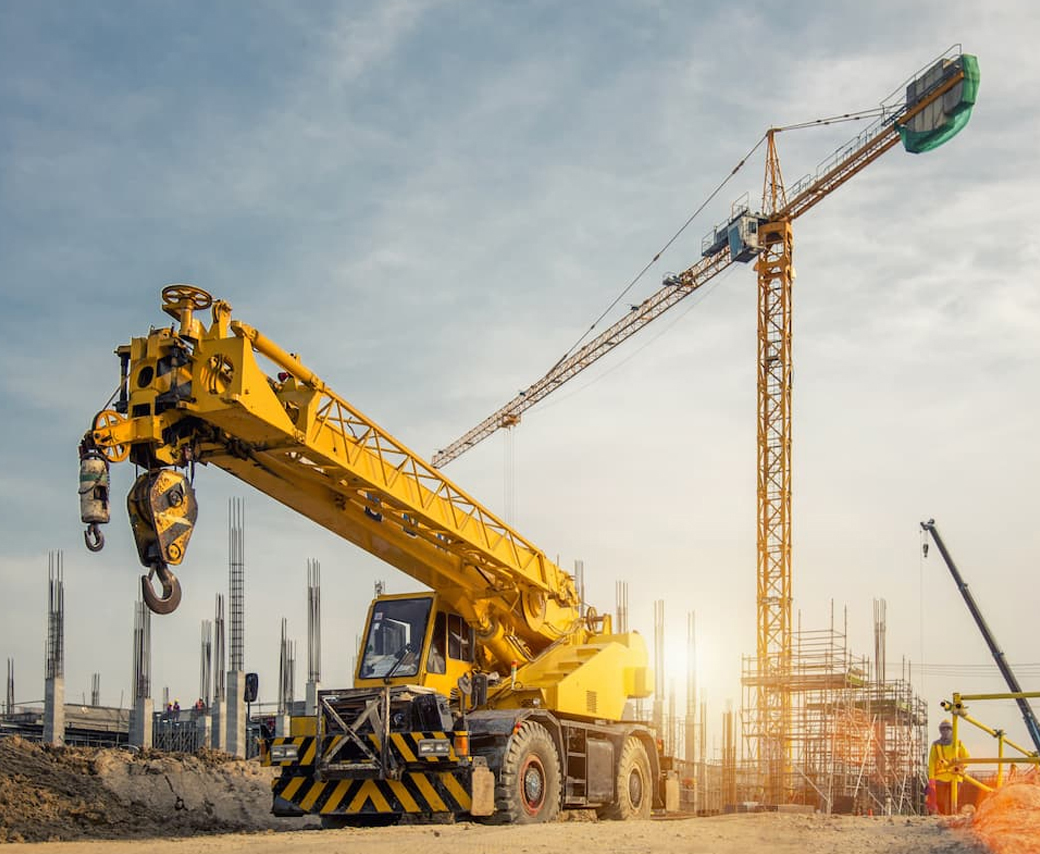
Used in cranes, excavators, concrete mixers, and pile drivers, our rugged helical and planetary gearboxes handle heavy loads, frequent starts/stops, and harsh job-site conditions — ensuring durability where failure is not an option.
Read more

HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
Discover our complete range of precision gearboxes engineered for packaging lines, food processing systems, and beyond.