Leave Your Message
Explore our featured high-performance gearbox products engineered for demanding industrial and mining applications.
A helical gearbox is a type of mechanical power transmission device in which the gear teeth are cut at an angle (helix angle) to the gear axis. Unlike spur gears, helical gears engage gradually and progressively, resulting in smoother, quieter operation and the ability to carry significantly higher loads. These characteristics make helical gearboxes the preferred choice for mining, quarrying, and heavy equipment industries — environments defined by extreme torque demands, continuous 24/7 operation, heavy shock loads, dust, moisture, and temperature extremes.
In underground coal mines, open-pit copper extraction, iron ore processing plants, and aggregate quarrying operations, helical gearboxes serve as the backbone of every critical drive system — from massive conveyor belts transporting thousands of tons of ore per hour, to crushers, ball mills, hoists, and ventilation fans. The ability to transmit power reliably under continuous heavy loads, while maintaining high efficiency (typically 96–99% per stage), directly impacts the profitability and safety of mining operations.
Why engineers and procurement specialists specify helical gearboxes for the most demanding applications on earth.
Helical gears distribute load across multiple teeth simultaneously, enabling extremely high torque transmission in a compact form factor. This is essential for mining conveyors and crushers handling hundreds of kilowatts of continuous power.
The angled tooth engagement produces a gradual meshing action that dramatically reduces noise and vibration — critical in enclosed mining facilities and underground operations where equipment noise affects worker safety and equipment longevity.
With efficiencies of 96–99% per stage, helical gearboxes minimize energy losses — a significant economic advantage in large-scale mining operations running 24/7 where even a 1% efficiency gain translates to substantial annual energy savings.
Manufactured from high-grade alloy steels with precision-ground tooth profiles and advanced surface treatments, HZPT helical gearboxes are engineered for 50,000+ hours of continuous operation in abrasive, dusty, and corrosive mining environments.
Modular housing designs allow for flexible shaft configurations, mounting options, and ratio selections — enabling engineers to specify the exact gearbox for each unique application without costly custom engineering from scratch.
IP65/IP67 sealing standards, integrated cooling systems, and proprietary surface treatment processes ensure reliable operation in temperatures from -30°C to +80°C, high humidity, and continuous exposure to abrasive dust and water ingress.
Helical gearboxes are deployed across every critical drive point in modern mining and heavy industrial operations.
Long-distance overland conveyors and underground mine conveyors rely on helical or helical-bevel gearboxes to transmit motor power to drive pulleys. These systems may run continuously for months, transporting thousands of tons of ore daily. High starting torque capability, thermal stability, and shock load absorption are non-negotiable requirements met by industrial helical gearboxes.
Crushers subject gearboxes to severe cyclic shock loads as rock is fractured. Helical gearboxes with reinforced housings, high-capacity bearings, and hardened gear profiles withstand these impact forces while maintaining precise speed reduction ratios — ensuring consistent crusher throughput and minimizing unplanned downtime.
Grinding mills are among the most power-intensive equipment in mineral processing, often driven by motors exceeding 5,000 kW. Multi-stage helical gearboxes provide the massive torque multiplication required while maintaining smooth, low-vibration operation that protects mill liners and structural components from fatigue damage.
Shaft hoists for personnel and ore transport demand absolute reliability and precise speed control. Helical gearboxes in hoist applications must handle dynamic braking loads, frequent starts and stops, and maintain exact positioning accuracy — all while supporting safety-critical certification requirements.
Underground mine ventilation is a life-safety system. Axial and centrifugal fans driven by helical gearboxes must operate continuously and reliably. The low-noise characteristic of helical gears is particularly valued in this application, as excessive vibration can indicate — or cause — structural issues in underground fan installations.
Excavators, bulldozers, tunnel boring machines (TBMs), and large cranes all incorporate helical gearboxes in their slew, travel, and lift drive systems. The compact power density of helical gearboxes allows machine designers to maximize payload capacity and machine performance without compromising structural integrity or mobility.
The mining and heavy equipment sectors are undergoing rapid transformation — and gearbox technology is evolving in step.
The global push toward zero-emission mining is driving the adoption of electric-powered haul trucks, loaders, and drills. Battery-electric and trolley-assist systems require high-efficiency helical gearboxes optimized for electric motor characteristics — including high starting torque, wide speed ranges, and regenerative braking compatibility. This trend is creating demand for a new generation of compact, high-efficiency helical gearbox designs.
Industry 4.0 is transforming maintenance strategies from reactive to predictive. Modern helical gearboxes are increasingly equipped with embedded vibration sensors, temperature monitors, and oil condition sensors connected to IoT platforms. Real-time condition monitoring allows mining operators to detect early signs of gear wear, bearing failure, or lubrication degradation — preventing catastrophic failures and reducing unplanned downtime by up to 40%.
The development of new carburized and case-hardened alloy steels, combined with advanced gear grinding and superfinishing processes, is enabling helical gearboxes to achieve higher power density at reduced weight. Proprietary surface treatment processes — including shot peening, phosphating, and DLC coatings — are extending gear life in abrasive mining environments while reducing lubrication requirements.
Leading manufacturers are developing modular gearbox platforms that allow mining operators to standardize on a smaller number of gearbox families across diverse applications. This reduces spare parts inventory, simplifies maintenance training, and enables faster replacement during planned shutdowns — all critical factors in maximizing mine productivity and reducing total cost of ownership.
Mining companies face increasing regulatory and investor pressure to reduce energy consumption and carbon emissions. High-efficiency helical gearboxes play a direct role in meeting these targets — replacing older worm gear or spur gear reducers with modern helical units can reduce drive system energy consumption by 15–25%, delivering both environmental and economic benefits at scale.
Rapid infrastructure development and resource extraction in Africa, Southeast Asia, and Latin America is creating significant new demand for reliable, cost-effective helical gearbox solutions. Global suppliers with strong technical support networks and localized service capabilities — like HZPT's presence in 60+ countries — are well-positioned to capture this growing market opportunity.
HZPT is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
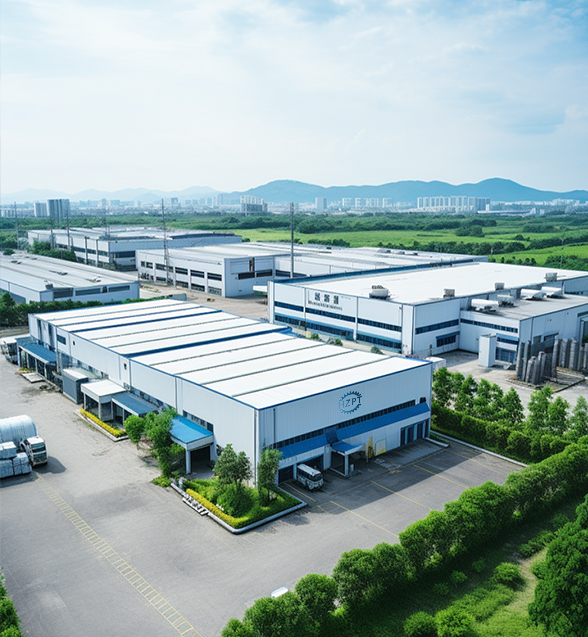
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
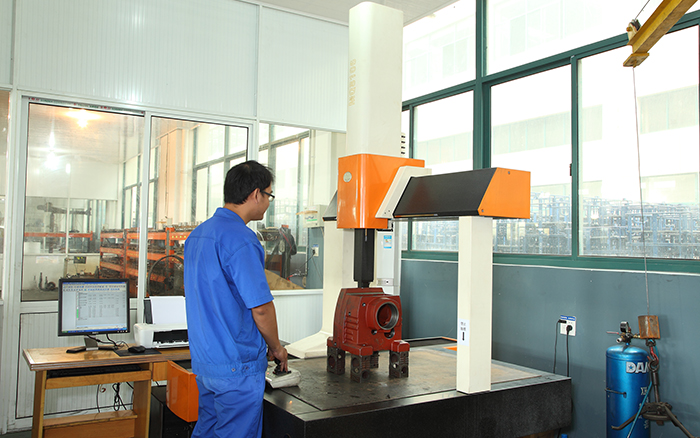
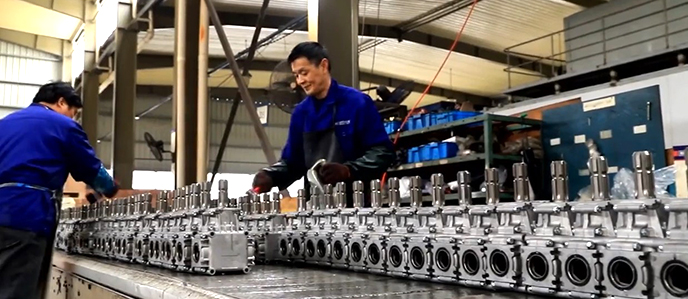
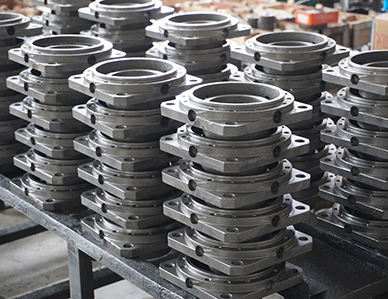
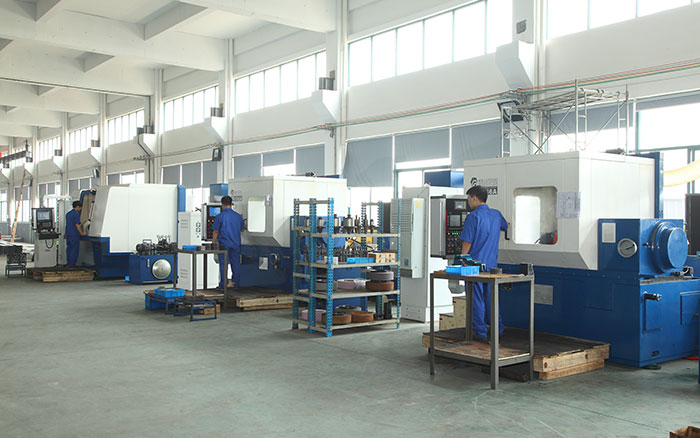
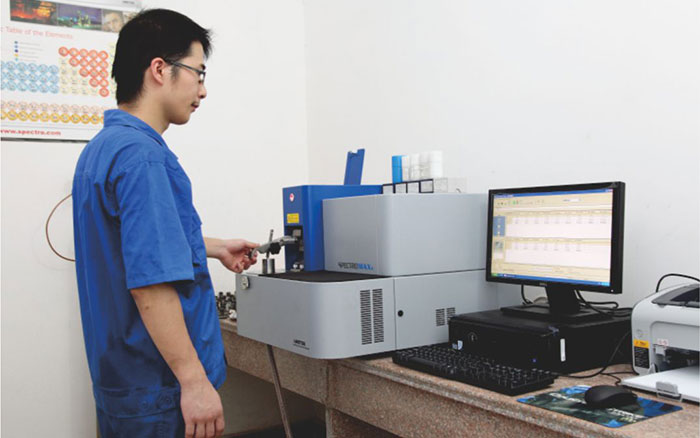
World-class engineering talent and experienced production professionals drive every product we build.
Our engineering team, led by veterans with over 15+ years of industry experience, is the core of our innovation. We maintain active "Industry-University-Research" collaborations with leading institutions to pioneer advancements in gear geometry, materials science, and tribology.
Our production floor is staffed by highly trained and experienced technicians, with over 30% holding advanced technical certifications. Their craftsmanship and attention to detail are embedded in every product we build.
Our leadership team brings international expertise and modern management practices, steering the company with a clear vision for sustainable growth and technological leadership in global power transmission markets.
Our commitment to quality and innovation is validated by third-party accreditations and intellectual property.
We hold 30+ national patents, including 5 invention patents. These cover key areas like "Modular Housing Design," "High-Efficiency Helical-Herringbone Gear Profiles," "Integrated Cooling Systems," and "Proprietary Surface Treatment Processes." Every helical gearbox we manufacture for mining and heavy equipment applications is backed by rigorous quality management systems and internationally recognized certifications — giving procurement teams and engineers full confidence in product reliability and compliance.
From helical reducers to planetary gearboxes — explore our full portfolio of precision power transmission solutions.
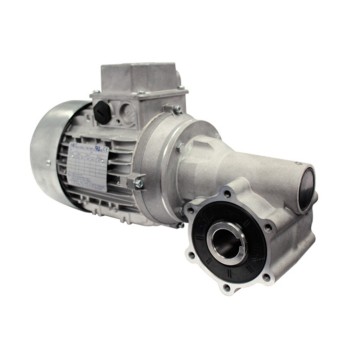 Automatic Car Wash Gearbox
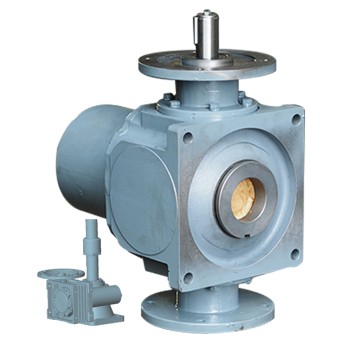 SWL Screw Jack Gearbox for Jump Form Construction Lifting
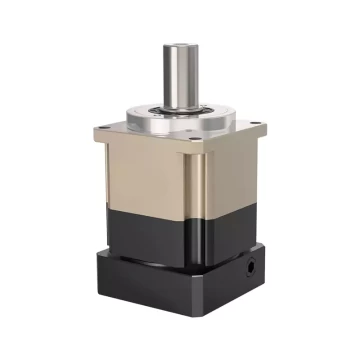 TM042 Series High Precision Planetary Gearbox Helical Gear Reducer
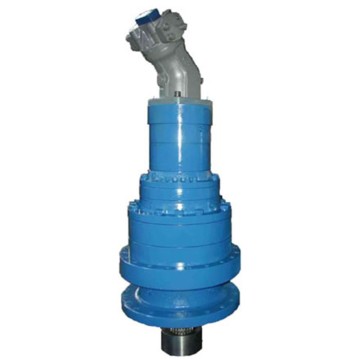 Pitch Drive Planetary Gearbox Reducer for Wind Turbine
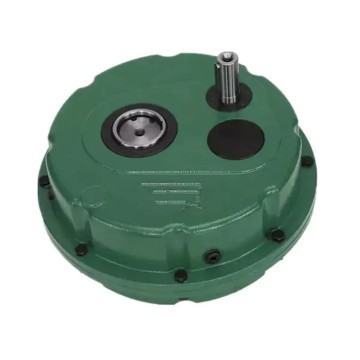 DXG (ATA) Series Shaft-Mounted Gearbox
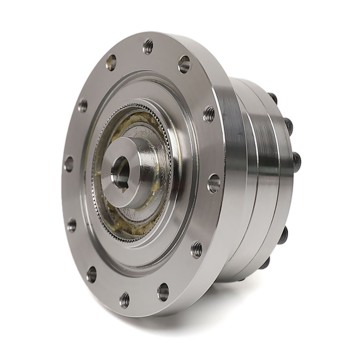 CF14 High Precision Harmonic Gearbox Reducer
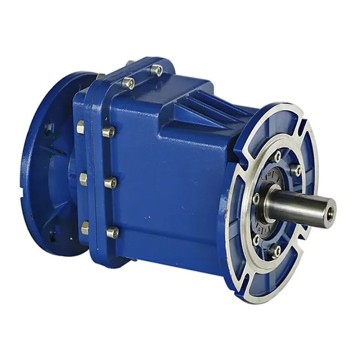 RC Series Helical Gearbox
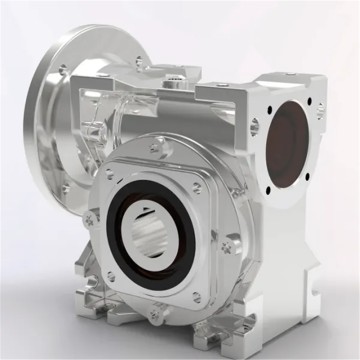 SSRV Series Stainless Steel Worm Gearbox Reducer