Leave Your Message
Explore our most-requested gearbox models engineered for crane, hoist, and lifting equipment applications.
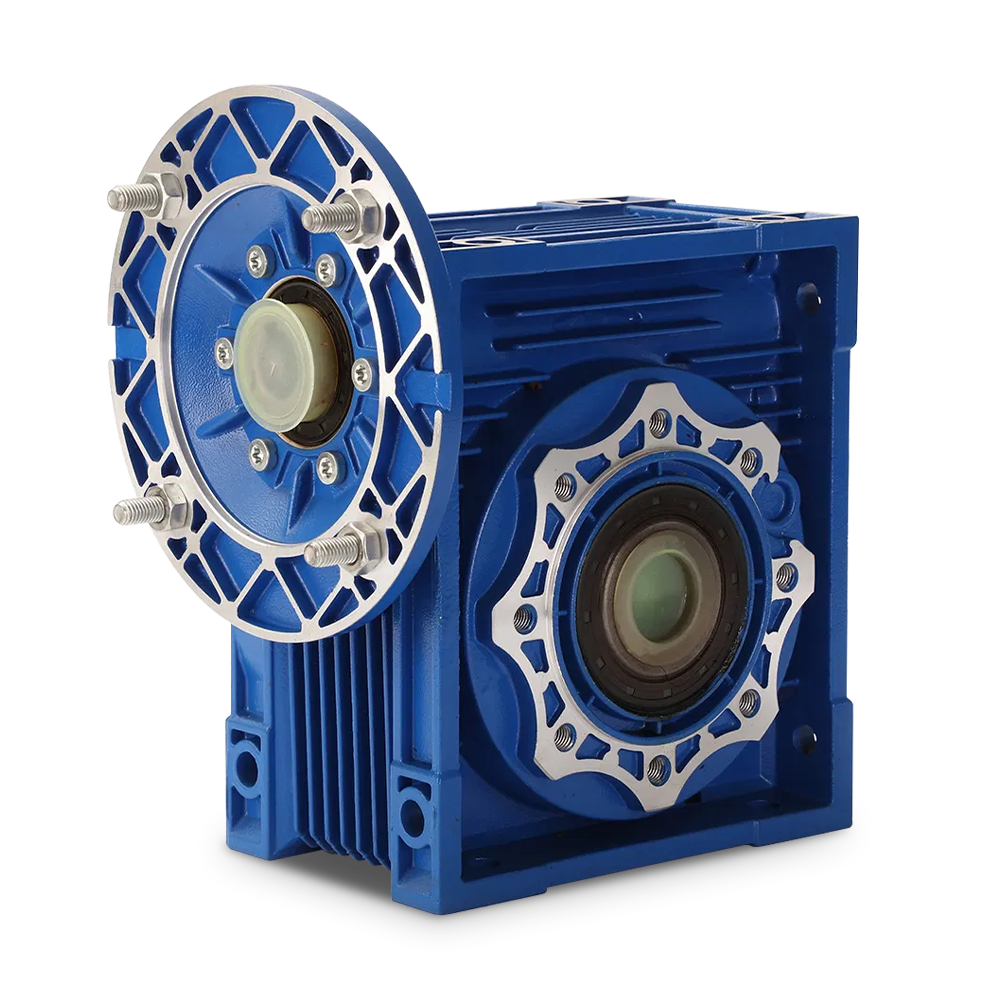
A helical bevel gearbox is a right-angle power transmission device that combines the smooth, low-noise characteristics of helical gearing with the directional change capability of bevel gears. The result is a compact, high-efficiency reducer capable of transmitting large torques at precise speed ratios — making it the preferred choice for cranes, hoists, and a wide range of lifting equipment worldwide.
Unlike standard worm gearboxes, helical bevel units achieve mechanical efficiencies of up to 98%, significantly reducing energy losses and heat generation during continuous-duty lifting cycles. The helical tooth profile distributes load across multiple teeth simultaneously, delivering quieter operation and longer service life even under shock loads typical of overhead crane travel drives and hoist drum applications.
Helical bevel gearboxes outperform worm drives in energy efficiency, making them the go-to solution for high-duty-cycle crane and hoist applications where operating costs matter.
The lifting industry operates under some of the most demanding mechanical conditions in any industrial sector. Overhead bridge cranes, gantry cranes, jib cranes, electric chain hoists, wire rope hoists, and construction tower cranes all share a common requirement: reliable, precise, and efficient torque transmission under variable and often shock-loaded conditions.
Helical bevel gearboxes address these demands through several key design advantages:
The global market for industrial gearboxes used in material handling and lifting equipment has been on a consistent growth trajectory. Driven by rapid expansion in e-commerce logistics infrastructure, port automation, smart manufacturing, and large-scale construction projects, demand for high-performance helical bevel gearboxes is accelerating across every major industrial economy.
According to industry analysis, the global crane and hoist market is projected to exceed USD 45 billion by 2030, with power transmission components — particularly gearboxes — representing a significant share of the total equipment value. Asia-Pacific leads demand growth, fueled by infrastructure investment in China, India, and Southeast Asia, while Europe and North America are driving premium demand for energy-efficient, IoT-ready gearbox solutions.
Key market segments driving helical bevel gearbox adoption in lifting applications include:
The global crane and hoist market is projected to exceed USD 45 billion by 2030. Helical bevel gearboxes are at the center of this growth, powering the next generation of automated lifting systems.
In overhead bridge cranes, helical bevel gearboxes serve dual roles: long-travel and cross-travel wheel drives, and hoist drum reduction. The right-angle configuration allows the motor to be mounted parallel to the bridge girder, minimizing overall crane height and enabling installation in low-headroom facilities. Multi-stage helical bevel units with integrated backstop devices prevent load drift during power interruptions — a critical safety requirement in steel processing and automotive plants.
Ship-to-shore (STS) and rubber-tyred gantry (RTG) cranes at container terminals demand gearboxes capable of handling millions of load cycles per year. Helical bevel gearboxes in these applications are typically specified with IP65 or higher sealing, corrosion-resistant coatings, and synthetic lubricants rated for wide temperature ranges. The high efficiency of helical bevel units directly reduces electricity consumption — a major operational cost driver at large port facilities handling thousands of container moves per day.
Tower cranes present unique challenges: variable load profiles, frequent start/stop cycles, and exposure to outdoor environmental conditions. Helical bevel gearboxes for tower crane hoisting drives are engineered with thermal monitoring provisions and modular designs that allow field servicing without full disassembly. Slewing ring drives use helical bevel units with integrated pinion shafts, providing the precise speed control needed for safe load positioning at height.
Industrial wire rope hoists from 1-tonne to 100-tonne capacity rely on compact helical bevel gearboxes mounted coaxially with the drum. The combination of helical and bevel stages achieves the high reduction ratios needed for slow, controlled lifting while maintaining the compact envelope required for standard hoist body dimensions. Noise levels below 72 dB(A) are achievable, meeting workplace noise regulations in sensitive environments such as hospitals, laboratories, and clean rooms.
Offshore pedestal cranes and marine deck cranes operate in some of the harshest environments on earth — salt spray, temperature extremes, and constant vibration. Helical bevel gearboxes for these applications feature stainless steel fasteners, epoxy-coated housings, and labyrinth seals with positive pressure lubrication to prevent water ingress. Classification society approvals (DNV, ABS, Lloyd's Register) are standard requirements for offshore crane gearboxes.
The integration of IoT sensors into helical bevel gearbox housings is transforming maintenance practices across the crane industry. Vibration sensors, temperature probes, and oil quality monitors embedded in the gearbox provide real-time data to plant management systems, enabling predictive maintenance strategies that reduce unplanned downtime by up to 40%. Leading manufacturers are now offering gearboxes withbuilt-in wireless connectivity, allowing remote diagnostics and performance optimization through cloud-based analytics platforms.
With industrial energy costs rising and carbon reduction targets tightening globally, end users are prioritizing gearbox efficiency more than ever. Helical bevel gearboxes with optimized gear geometry, low-friction bearings, and synthetic lubricants can reduce energy consumption by 15-25% compared to older worm gear designs. This efficiency gain translates directly to lower operating costs and reduced carbon footprint — critical factors for companies pursuing ISO 50001 energy management certification and ESG reporting goals.
Modern helical bevel gearbox families are designed around modular platforms that allow rapid configuration for specific applications. Standardized mounting interfaces, interchangeable gear stages, and flexible input/output shaft arrangements enable manufacturers to offer thousands of ratio and torque combinations from a limited set of core components. This modularity reduces lead times, simplifies spare parts inventory, and lowers total cost of ownership for crane fleet operators.
The push for higher power density and longer service life is driving adoption of advanced gear materials and surface treatments. Case-hardened alloy steels with nitriding or carbonitriding surface treatments achieve surface hardness exceeding 60 HRC while maintaining tough, ductile cores resistant to shock loads. Micro-pitting resistant gear profiles and super-finished tooth flanks extend gear life by 50% or more in high-cycle applications.
The widespread adoption of VFDs for crane motor control has implications for gearbox design. Helical bevel gearboxes paired with VFD-controlled motors must handle the additional electrical bearing currents and torsional vibrations introduced by PWM inverter switching. Modern gearbox designs incorporate insulated bearings and torsionally compliant couplings to mitigate these effects, ensuring reliable operation across the full VFD speed range.
Engineered for reliability, efficiency, and long service life in the most demanding lifting applications.
CNC gear grinding to ISO 6 quality ensures smooth, quiet operation and maximum load capacity.
Interchangeable stages and mounting options enable rapid customization for specific crane configurations.
Tapered roller and spherical roller bearings rated for high radial and axial loads typical of lifting applications.
Optimized housing design and synthetic lubricants maintain stable operating temperatures under continuous duty.
Optional backstop devices prevent reverse rotation and load drift in hoist drum applications.
Multi-stage labyrinth seals and optional positive pressure systems protect against dust and moisture ingress.
Proven performance and global reach built on 15+ years of engineering excellence.
From automated warehouses to offshore platforms, our helical bevel gearboxes power critical lifting operations worldwide.
Long-travel, cross-travel, and hoist drum drives for manufacturing, steel mills, and automotive plants.
STS and RTG crane slewing, trolley, and hoisting drives engineered for millions of load cycles.
Hoisting and slewing drives with thermal monitoring for safe, precise load positioning at height.
Corrosion-resistant gearboxes with classification society approvals for harsh marine environments.
Compact drum drives from 1-tonne to 100-tonne capacity with noise levels below 72 dB(A).
High-efficiency gearboxes for automated storage and retrieval systems (AS/RS) and overhead conveyors.
The lifting equipment industry is evolving rapidly. Here's what's driving change in helical bevel gearbox technology.
IoT sensors and cloud analytics enable predictive maintenance, reducing unplanned downtime by up to 40%.
Optimized gear geometry and synthetic lubricants reduce energy consumption by 15-25% vs. legacy designs.
Standardized interfaces and interchangeable stages reduce lead times and simplify spare parts management.
Nitrided alloy steels and micro-pitting resistant profiles extend gear life by 50% in high-cycle applications.
Insulated bearings and torsionally compliant couplings ensure reliable operation with variable frequency drives.
Asia-Pacific leads demand growth, while Europe and North America drive premium IoT-ready gearbox adoption.
Your Trusted Partner in Precision Gearbox Solutions
HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
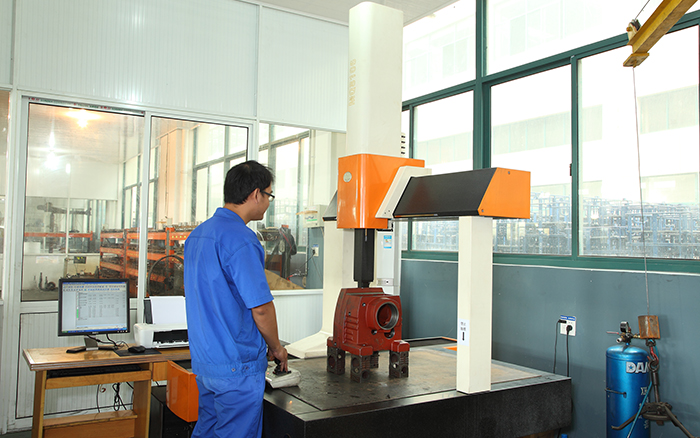
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
DISCOVER OUR SUSTAINABILITY PROJECTS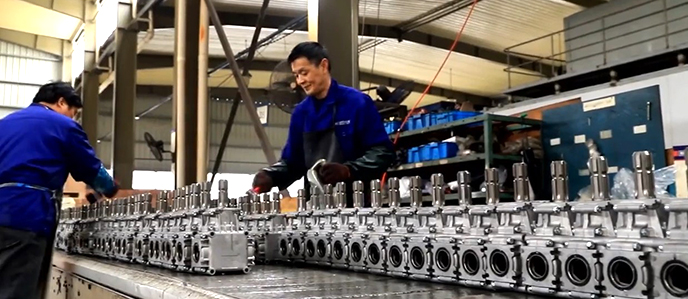
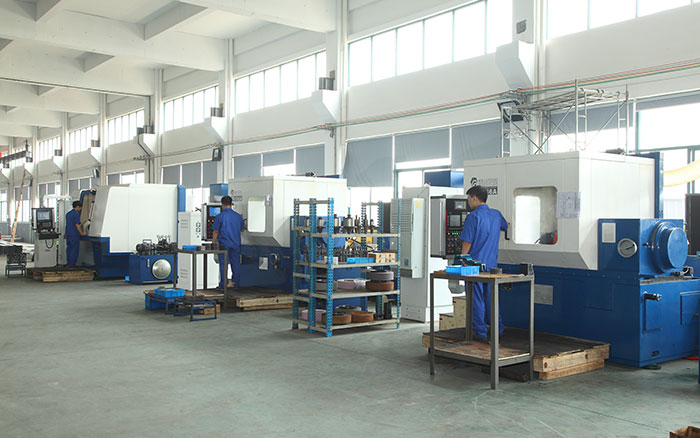
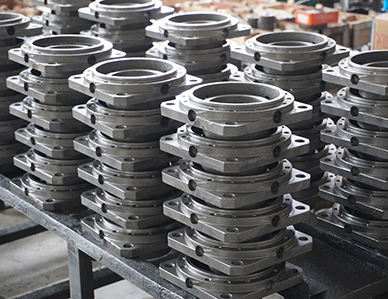
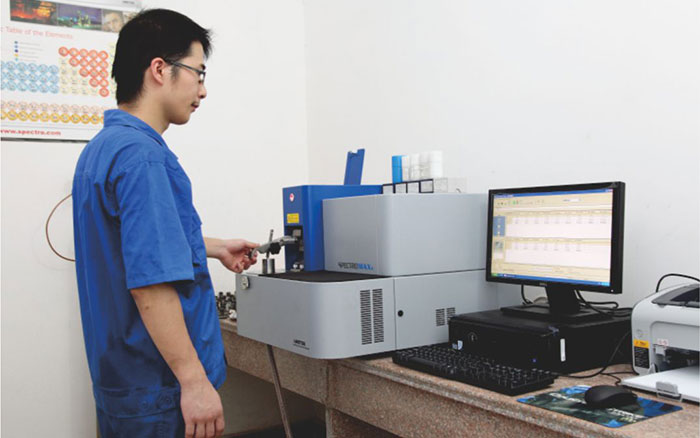
Expertise, craftsmanship, and leadership driving innovation in every gearbox we build.
Our engineering team, led by veterans with over 15+ years of industry experience, pioneers advancements in gear geometry, materials science, and tribology through active Industry-University-Research collaborations.
Our production floor is staffed by highly trained technicians, with over 30% holding advanced technical certifications. Their craftsmanship and attention to detail are embedded in every product we build.
Our leadership team brings international expertise and modern management practices, steering the company with a clear vision for sustainable growth and technological leadership.
Our commitment to quality and innovation is validated by third-party accreditations and intellectual property. We hold 30+ national patents, including 5 invention patents covering key areas like "Modular Housing Design," "High-Efficiency Helical-Herringbone Gear Profiles," "Integrated Cooling Systems," and "Proprietary Surface Treatment Processes."
From precision planetary reducers to heavy-duty cycloidal gearboxes, we offer comprehensive solutions for every industrial application.
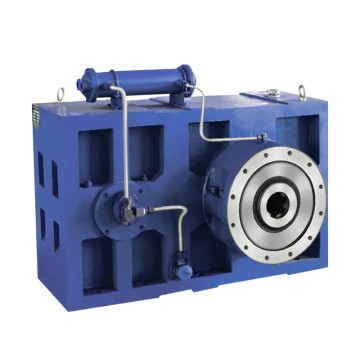 ZLYJ Series Plastic Extruder Gearbox Reducer
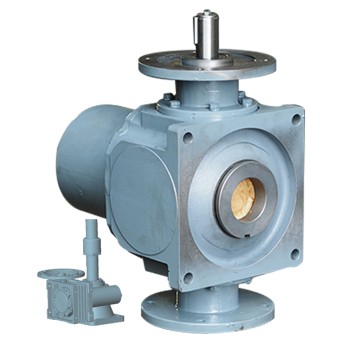 SWL Screw Jack Gearbox for Jump Form Construction Lifting
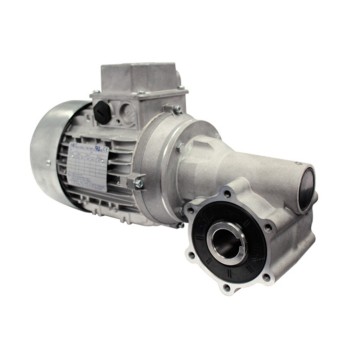 Automatic Car Wash Gearbox
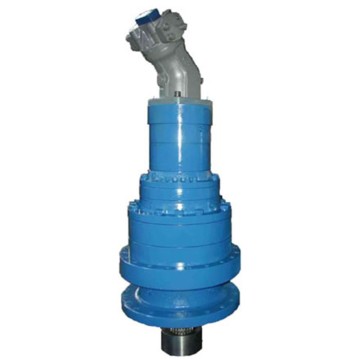 Pitch Drive Planetary Gearbox Reducer for Wind Turbine
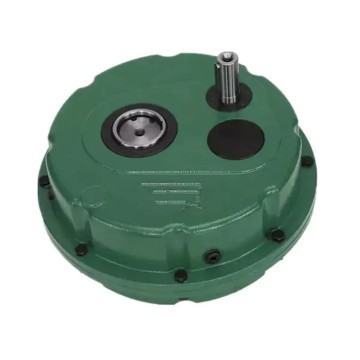 DXG (ATA) Series Shaft-Mounted Gearbox
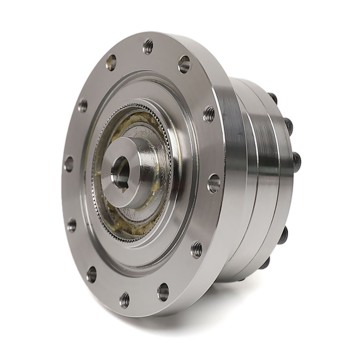 CF14 High Precision Harmonic Gearbox Reducer
 XW/BW Series Cycloidal Gearbox – Cyclo Pinwheel Reducer
 TM042 Series High Precision Planetary Gearbox Helical Gear Reducer