Leave Your Message
Explore our top-rated gearbox series designed for crane, hoist, and lifting applications
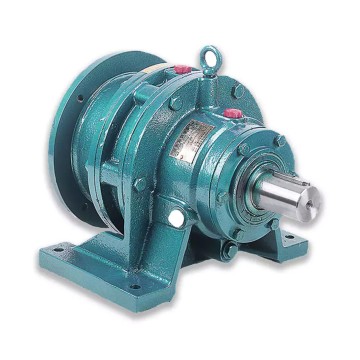
A cycloidal gearbox (also known as a cyclo drive or cycloidal speed reducer) operates on a fundamentally different principle from conventional gear trains. Instead of meshing teeth, it uses an eccentric cam to drive a cycloidal disc that rolls around the inside of a ring gear, transmitting torque through a series of output pins. This architecture delivers exceptional shock-load absorption — a critical requirement for cranes, hoists, and lifting equipment where sudden load engagements and emergency stops are routine.
In lifting applications, the consequences of gearbox failure can be catastrophic. Cycloidal drives are engineered with multiple contact points simultaneously sharing the load — typically 60–70% of all pins engage at once — resulting in extremely high torque density and unmatched overload capacity. This makes them the preferred choice for overhead bridge cranes, wire rope hoists, jib cranes, and heavy-duty material handling systems.
Cycloidal gearboxes can absorb shock loads up to 500% of rated torque, making them ideal for crane hoist duty cycles with frequent start-stop operations.
Achieve ratios from 6:1 to 6000:1 in a single stage within an extremely compact envelope — essential for space-constrained crane end trucks.
Multi-point tooth engagement distributes impact forces across dozens of contact points, preventing catastrophic failure under sudden load application.
Rolling contact replaces sliding friction, dramatically reducing noise levels — critical for indoor warehouse cranes and precision lifting environments.
Minimal wear components and robust hardened steel construction ensure 20,000+ hour service life even under continuous heavy-duty lifting cycles.
From port container cranes to precision surgical lifts — cycloidal drives power the world's most critical vertical motion systems
In steel mills and heavy fabrication facilities, overhead cranes handle loads exceeding 500 tonnes with frequent duty cycles. Cycloidal gearboxes installed in the hoist drum drive and cross-travel drive deliver the torque density required while maintaining precise positioning accuracy within ±1mm. Their ability to hold loads statically — thanks to inherent self-locking characteristics — provides an additional safety layer in manned environments.
Port container cranes operate in corrosive marine environments with continuous 24/7 duty cycles. Cycloidal gearboxes with IP65/IP67 sealed housings and marine-grade surface treatments resist salt spray and humidity while delivering the extreme torque required to lift 40-tonne containers at high speeds. The compact form factor also simplifies integration into the tight mechanical spaces of rubber-tyred gantry (RTG) crane bogies.
Tower cranes demand gearboxes that perform reliably at heights exceeding 200 metres in wind, rain, and temperature extremes. Cycloidal drives in the slewing, luffing, and hoisting mechanisms provide smooth, controllable motion essential for precise load placement. Construction personnel hoists (man-riders) use cycloidal gearboxes specifically for their fail-safe load-holding capability and compliance with EN 81-3 and FEM standards.
Nuclear facilities demand absolute precision and zero tolerance for mechanical failure. Cycloidal gearboxes are specified for fuel assembly handling cranes and reactor head lift rigs due to their minimal backlash (less than 1 arcminute), vibration-free operation, and proven reliability in radiation environments. Their sealed construction prevents contamination of sensitive areas — a non-negotiable requirement in nuclear safety protocols.
Modern healthcare facilities use ceiling-mounted patient hoists for safe patient transfer. Cycloidal drives in these systems provide whisper-quiet operation (below 55dB), precise speed control for patient comfort, and reliable load holding without brake dependency. The compact profile allows integration into architecturally sensitive ceiling track systems while meeting stringent medical device safety standards.
High-volume automotive plants operate hundreds of hoists simultaneously for engine installation, body panel handling, and sub-assembly lifting. Cycloidal gearboxes deliver the consistent, repeatable performance required for takt-time production cycles, with low maintenance intervals that minimise production downtime. Explosion-proof variants serve paint shop environments where solvent vapours demand ATEX-rated equipment.
Emerging technologies and market forces are reshaping how cycloidal gearboxes are designed, specified, and deployed
Next-generation cycloidal gearboxes are being equipped with embedded IoT sensors monitoring temperature, vibration signature, oil contamination, and load cycles in real time. Integration with crane PLC systems enables predictive maintenance scheduling, reducing unplanned downtime by up to 60% in port and steel mill crane fleets.
As overhead crane manufacturers transition to fully electric and regenerative drive systems, cycloidal gearboxes are being optimised for direct coupling with permanent magnet servo motors. This combination delivers unprecedented positioning accuracy (±0.1mm) for automated warehouse cranes and robotic lifting systems in Industry 4.0 facilities.
Advanced high-strength aluminium alloys and 3D-printed titanium components are enabling the next generation of ultra-lightweight cycloidal drives for aerospace ground support equipment and offshore platform cranes where every kilogram of drive weight directly impacts payload capacity.
The global lifting equipment market is projected to exceed USD 42 billion by 2030, driven by port expansion projects in Asia and the Middle East, renewable energy infrastructure construction, and automated warehouse development. Cycloidal gearboxes are positioned as the preferred drive solution for the most demanding applications in this growth wave.
Evolving international standards including FEM 1.001, ISO 4301, and ASME B30 series are driving demand for certified, traceable gearbox components. Manufacturers who invest in third-party certification, full material traceability, and documented test protocols gain significant competitive advantage in regulated markets.
End users are increasingly demanding application-engineered solutions rather than catalogue products. Custom cycloidal gearboxes with specific mounting configurations, integrated brakes, encoder feedback, and special seal packages for food-grade or pharmaceutical lifting environments represent the fastest-growing segment of the market.
Our flagship XW/BW Series Cycloidal Gearbox represents the pinnacle of cyclo pinwheel reducer technology, purpose-built for crane hoist drives, winch systems, and heavy lifting machinery. The series covers output torque from 150 Nm to 22,000 Nm with reduction ratios from 9:1 to 87:1 in a single stage, and up to 7569:1 in two stages.
Key design features include a hardened steel cycloidal disc with mirror-finish tooth profile for maximum efficiency, a robust cast iron housing with precision-bored bearing seats, and a dual-lip seal system with labyrinth protection for operation in dusty, wet, or chemically aggressive crane environments.
The XW/BW Series is CE marked, ISO 9001:2015 certified, and compliant with FEM crane duty classifications M3–M8 — making it suitable for the most demanding hoist applications.
A Legacy of Growth & Innovation in Industrial Gearbox Manufacturing
Established in 2002, HZPT began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardised models — including cycloidal, helical, and planetary types — allowed us to build a reputation for reliability and establish a solid technical foundation that continues to underpin everything we do today.
Responding to market demands from crane OEMs, port equipment manufacturers, and mining companies, we significantly expanded our production capabilities and R&D investment. This period saw the introduction of custom-engineered and application-specific cycloidal drive solutions for lifting and hoisting, enabling us to serve more complex industrial needs and establish long-term global partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools, CNC gear grinding centres, and automated assembly processes, we now deliver next-generation cycloidal gearboxes that are smarter, more compact, and more energy-efficient — solidifying our position as a global innovator in lifting drive technology.
We invest in world-class technology to ensure every cycloidal gearbox that leaves our facility is built to excel in the most demanding lifting environments
CMM & Gear Testing: In-process and final inspection using German coordinate measuring machines (CMM) and gear testers, providing micron-level accuracy for critical cycloidal disc and pin wheel components.
Metallurgical Laboratory: A fully equipped metallurgical lab for material spectroscopy, hardness testing, and microstructural analysis ensures raw material integrity from the very start of the production process.
Full-Load Performance Testing: A dedicated full-load performance test rig simulates real-world crane and hoist operating conditions. Every unit undergoes rigorous testing for noise, vibration, temperature rise, and sealing before shipment — ensuring flawless performance at your site from day one.
Traceable Documentation: Full material certificates, heat treatment records, dimensional inspection reports, and performance test certificates are available for every unit — essential for crane regulatory compliance and insurance requirements.
Quality is at the heart of everything we do — from raw material selection to after-sales technical support
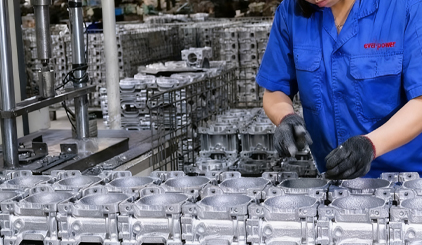
No diversions — just decades of refining cycloidal, helical, planetary, and parallel-shaft gearboxes for crane, hoist, and lifting equipment applications worldwide.
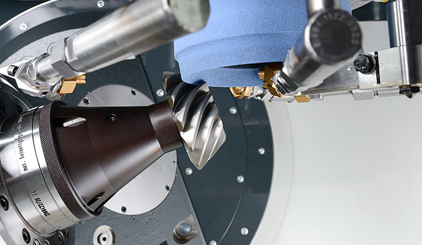
Critical processes including cycloidal disc grinding, heat treatment, housing machining, and final assembly are all performed under one roof — ensuring consistent quality and full traceability for every lifting gearbox.
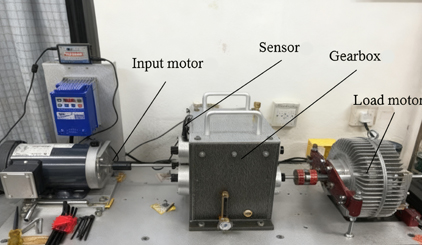
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks — test reports available on request. Your crane gearbox arrives ready to perform from the first lift.
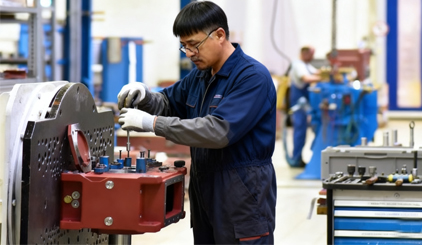
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese — because your crane uptime and lifting safety matter to us as much as they do to you.
For jump form construction and vertical lifting applications where precise, controllable elevation is required, our SWL Screw Jack Gearbox provides a reliable mechanical lifting solution. When paired with cycloidal drive units for the primary power transmission stage, this combination delivers the controlled, safe lifting action required by EN 1570 and ISO 24652 standards for construction lifting platforms.
The SWL series is available in worm gear and bevel gear configurations, with lifting capacities from 2.5kN to 1000kN, making it suitable for everything from architectural facade lifting to large-scale formwork elevation in high-rise construction projects.
Explore SWL Screw Jack Series →Our application engineers are ready to help you select, configure, and certify the optimal cycloidal drive solution for your lifting equipment — whether you're an OEM, an end user, or a maintenance engineer seeking a direct replacement.
Request a Technical Consultation →Explore our full range of industrial gearboxes — from cycloidal and planetary to helical and screw jack drives