Leave Your Message
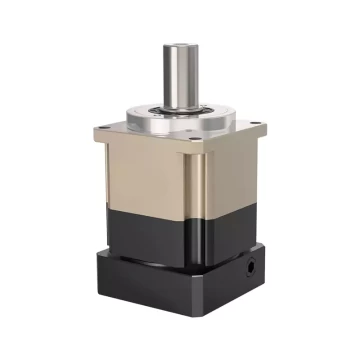
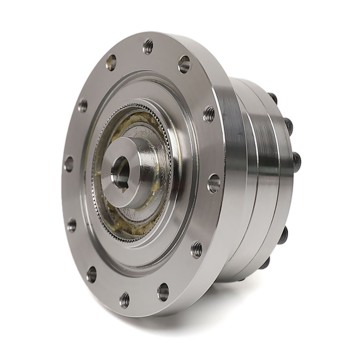
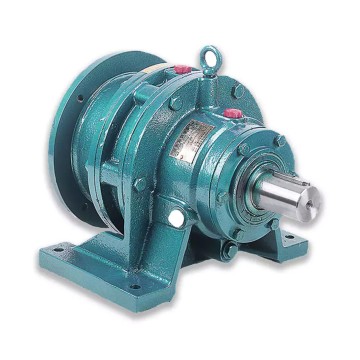
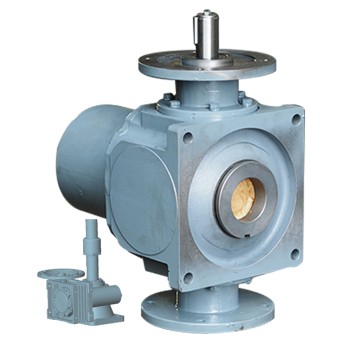
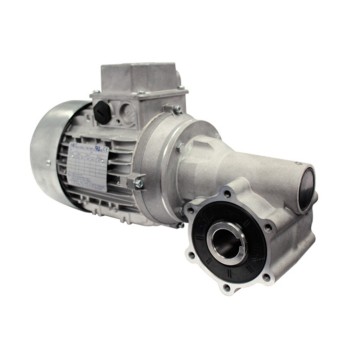
Our flagship gearbox series engineered for high-efficiency conveyor systems, material handling automation, and precision industrial drive applications.
Custom gearbox manufacturing for conveyor and material handling systems is one of the fastest-growing segments in the global power transmission industry.
The explosive growth of global e-commerce has triggered unprecedented demand for high-speed conveyor gearboxes in fulfillment centers, sortation systems, and automated parcel handling facilities.
Industry 4.0 and smart factory initiatives are reshaping material handling. Custom gearboxes are now integrated with sensors, encoders, and IoT modules to enable real-time performance monitoring and predictive maintenance.
Major investments in port automation, mining operations, food processing, and pharmaceutical production across Asia, Europe, and North America are creating sustained demand for reliable, custom-engineered gearbox solutions.
The custom gearbox sector is undergoing rapid technological transformation. Understanding these trends is essential for procurement engineers and system integrators.
Next-generation gearboxes for conveyor systems are being equipped with embedded vibration sensors, temperature monitors, and wireless communication modules. This enables real-time condition monitoring via cloud platforms, dramatically reducing unplanned downtime in high-throughput material handling operations such as airport baggage systems, automotive assembly lines, and large-scale distribution centers.
With energy costs and carbon footprint under global scrutiny, custom gearbox manufacturers are investing in IE4/IE5-compatible helical and planetary gear profiles, advanced surface coatings, and low-viscosity synthetic lubricants. Modern conveyor gearboxes can achieve transmission efficiencies exceeding 97%, delivering significant energy savings over the equipment lifecycle — a critical factor for 24/7 logistics operations.
Modular gearbox platforms allow manufacturers to rapidly configure solutions across a wide range of torque, speed, and mounting requirements without full custom engineering cycles. This dramatically shortens lead times for conveyor OEMs who need to quickly adapt to changing warehouse layouts, production line reconfigurations, or new product SKUs in their material handling systems.
The adoption of carburized and case-hardened alloy steels, combined with proprietary surface treatment processes such as shot peening and phosphating, is extending gear life by up to 3× compared to conventional designs. For material handling environments with heavy shock loads — such as mining conveyors, port cranes, and bulk handling systems — these advancements are critical for reliability and total cost of ownership.
Custom gearbox manufacturers are increasingly adopting closed-loop manufacturing processes, recyclable packaging, and ISO 14001-certified environmental management systems. Buyers in Europe and North America are increasingly requiring environmental compliance documentation as part of their supplier qualification process, making sustainability a genuine competitive differentiator.
Custom gearbox solutions are deployed across a vast spectrum of conveyor and material handling applications. Here is an in-depth analysis of the most critical use cases.
High-speed sortation conveyors, tilt-tray systems, and robotic picking stations require compact planetary gearboxes with ultra-low backlash and high positioning repeatability. Custom configurations with hollow shaft outputs enable direct drive of conveyor rollers, eliminating coupling losses and simplifying maintenance.
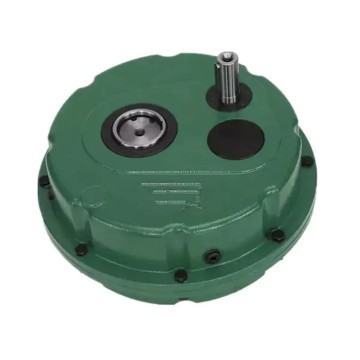
Belt conveyor drives in mining operations demand heavy-duty helical-bevel or shaft-mounted gearboxes capable of handling starting torques 2–3× the nominal rating. Custom thermal management, IP65+ sealing, and extended oil change intervals are essential for remote, harsh environments.
Container handling cranes, ship-to-shore loaders, and automated guided vehicles (AGVs) at modern ports rely on custom-engineered gearboxes with marine-grade corrosion protection, high shock load capacity, and fail-safe braking integration. Precision slewing ring drives and travel drives represent specialized sub-segments.
Hygienic conveyor gearboxes for food processing must meet FDA/EHEDG standards, featuring stainless steel housings (as in SSRV series), food-grade lubricants, and smooth external surfaces that resist bacterial growth. Washdown resistance and compliance with HACCP protocols are non-negotiable requirements.
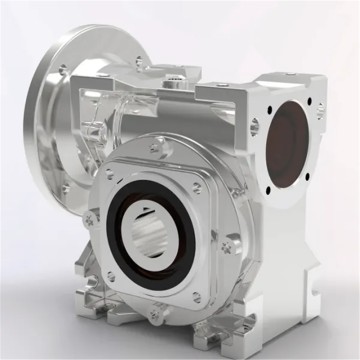
Jump form systems, material hoists, and construction elevators require screw jack gearboxes with high mechanical advantage, self-locking worm gear stages, and robust load-holding capability. SWL screw jack gearboxes are engineered specifically for these demanding vertical material handling applications.
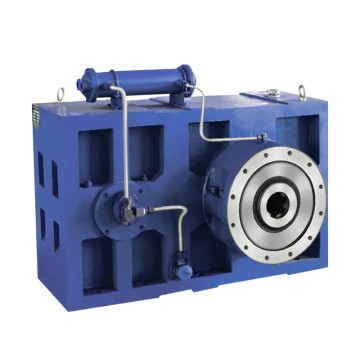
Single and twin-screw extruder gearboxes must withstand continuous high-thrust axial loads from the screw, while maintaining precise speed ratios for consistent melt quality. ZLYJ series extruder gearboxes are purpose-built for these demanding polymer processing environments with integrated thrust bearings.
Standard off-the-shelf gearboxes rarely meet the precise demands of modern conveyor and material handling systems. Here is why custom manufacturing matters.
Custom gearboxes are engineered to exact torque, speed ratio, mounting, and environmental specifications — eliminating over-engineering and reducing total system cost.
Purpose-built gear geometry, optimized lubrication systems, and premium materials result in gearboxes that outlast standard units by 2–5× in demanding conveyor duty cycles.
Custom mounting flanges, output shaft configurations, and connection interfaces mean zero adaptation work for OEM assembly lines — accelerating time-to-market for new conveyor systems.
Reduced energy consumption, fewer maintenance interventions, and longer replacement intervals deliver measurable ROI over the full lifecycle of material handling equipment.
HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
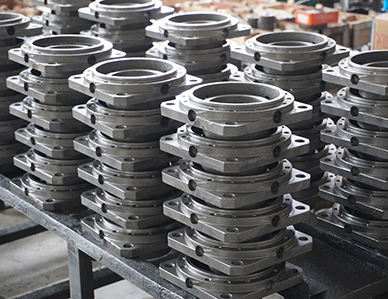
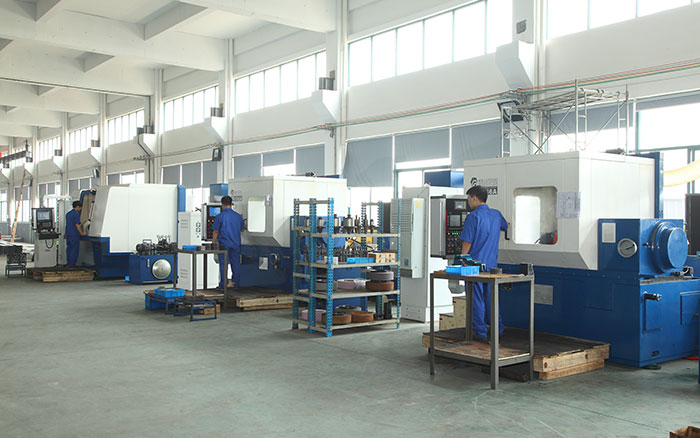
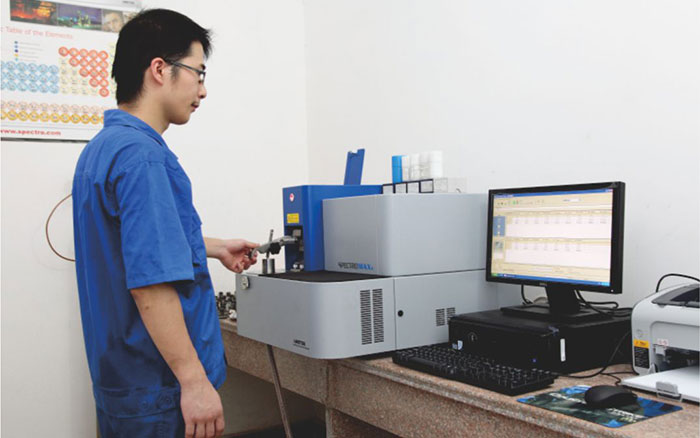
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
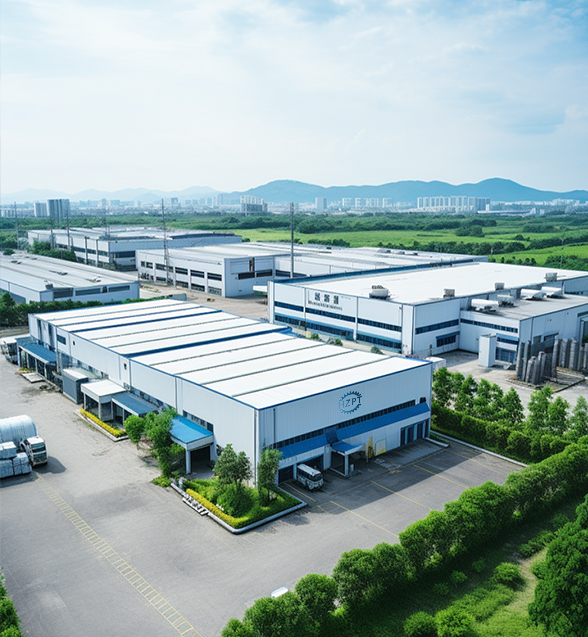
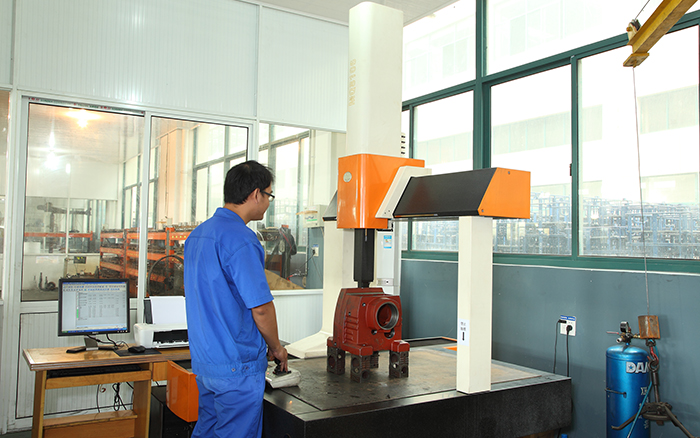
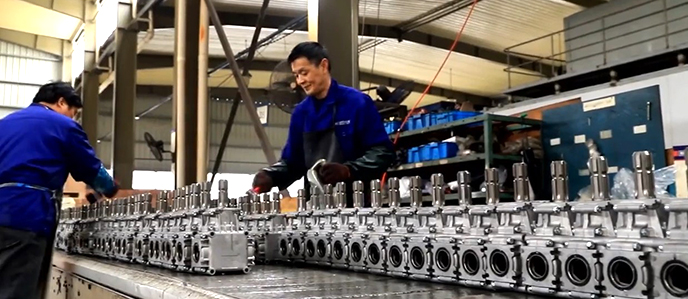
Our engineering team, led by veterans with over 15+ years of industry experience, is the core of our innovation. We maintain active "Industry-University-Research" collaborations with leading institutions to pioneer advancements in gear geometry, materials science, and tribology.
Our production floor is staffed by highly trained and experienced technicians, with over 30% holding advanced technical certifications. Their craftsmanship and attention to detail are embedded in every product we build.
Our leadership team brings international expertise and modern management practices, steering the company with a clear vision for sustainable growth and technological leadership in global power transmission markets.
Our commitment to quality and innovation is validated by third-party accreditations and intellectual property.
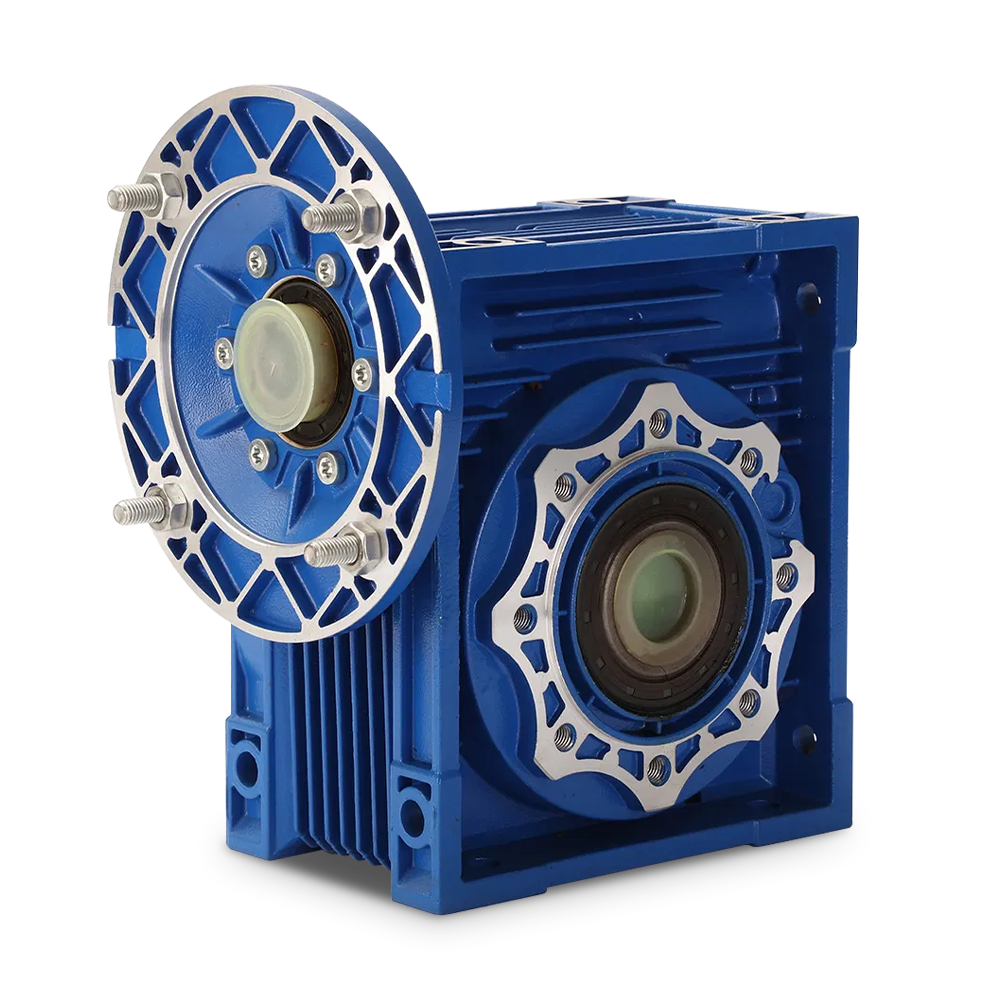
Explore our full lineup of custom-engineered gearbox solutions designed for every conveyor system, material handling, and industrial drive requirement.