Leave Your Message
Engineered for high load capacity, superior durability, and precision performance under extreme conditions
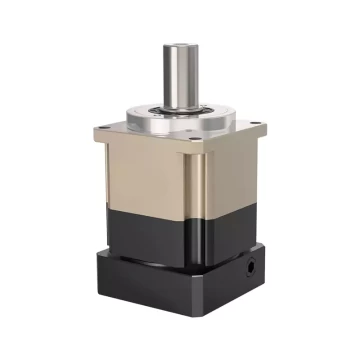
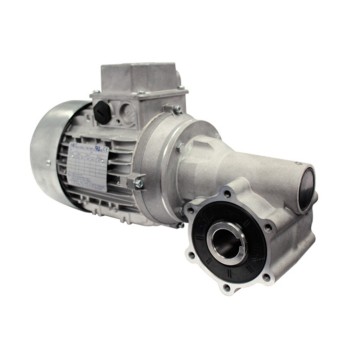
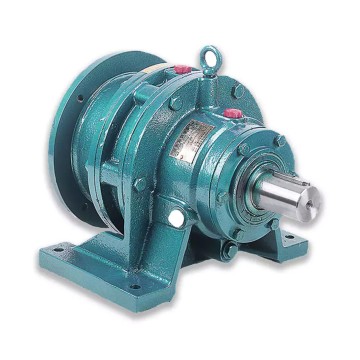
In the heavy machinery sector, standard, off-the-shelf transmission units often fall short of meeting the rigorous, highly specialized demands of modern engineering tasks. Global construction machinery and engineering equipment operate in some of the most unforgiving environments on Earth—ranging from sub-zero arctic mining fields to scorching desert infrastructure projects. In these scenarios, the gearboxes must withstand massive shock loads, severe vibration, high contamination from abrasive dust, and continuous, high-torque operations. This is where specialized custom gearbox manufacturers step in to bridge the gap between standard mechanical engineering and bespoke high-performance power transmission.
Custom gearboxes are not merely modified catalog components; they are engineered from the ground up. Designers must carefully calculate gear geometry, select advanced metallurgical formulations, plan sophisticated lubrication paths, and integrate thermal dissipation systems tailored to the exact duty cycles of the target machine. Whether it is a multi-stage planetary gear system for a tunnel boring machine or a compact, high-precision helical-bevel drive for an electric excavator, customization ensures that the gearbox matches the envelope space, weight limitations, and electrical or hydraulic input characteristics of the equipment perfectly.
The global construction machinery market is undergoing a profound transformation. Major OEMs (Original Equipment Manufacturers) are shifting from hydraulic-dominated drivetrains to hybrid and fully electric systems. This paradigm shift has created a massive surge in demand for specialized custom gearboxes. High-speed electric motors require gearboxes with significantly higher input speeds, lower backlash, and exceptional efficiency to maximize battery life. Consequently, manufacturers who can customize gearboxes to manage input speeds exceeding 10,000 RPM while maintaining massive torque multiplication at the wheels or tracks are gaining substantial market share.
Additionally, the globalization of supply chains has placed a premium on reliability. A single gearbox failure on a mining excavator or a tower crane can lead to project delays costing tens of thousands of dollars per hour. As a result, EPC (Engineering, Procurement, and Construction) companies and machinery OEMs are increasingly partnering with established custom gearbox manufacturers in China who offer the dual advantages of state-of-the-art manufacturing facilities and cost-efficient production. The focus has shifted from finding the cheapest gear reducer to securing long-term technical partnerships that offer comprehensive design validation, advanced prototyping, and rigorous testing protocols.
Modern engineering equipment demands maximum torque output within highly restricted installation spaces. Custom planetary gearboxes utilize multi-point load sharing across planet gears to achieve unmatched torque-to-weight ratios.
To resist surface fatigue, pitting, and tooth breakage under sudden shock loads, gears undergo advanced carburizing, nitriding, and induction hardening. This ensures a hard, wear-resistant outer shell with a tough, ductile core.
Operating in mud, water, and abrasive dust requires multi-stage labyrinth seals and synthetic lubricants that maintain viscosity across extreme temperature ranges, preventing premature bearing and gear failures.
Custom designs allow for exact gear ratios to match specific motor torque curves, along with custom input flanges for seamless integration with hydraulic motors, AC/DC electric motors, or PTO drives.
To understand the necessity of custom gearbox manufacturing, one must analyze the diverse and demanding applications across the construction and engineering sectors:
Excavators require two distinct types of gearboxes: travel drives (track drives) and swing drives. The travel drive is housed inside the undercarriage crawler frame, requiring an ultra-compact, multi-stage planetary design that can fit within the narrow track width while delivering immense torque to move tons of steel over rough terrain. The swing drive, which rotates the upper superstructure, must handle massive radial loads and sudden braking forces. Custom manufacturers design these with integrated output pinions, heavy-duty slewing bearings, and dynamic multi-plate parking brakes to ensure smooth, precise, and safe positioning.
Concrete transit mixers and batching plants present unique challenges. The mixing drum must rotate continuously at slow speeds under full load. Any interruption in rotation can cause the concrete to cure inside the drum, destroying the equipment. Custom gearboxes for concrete mixers combine helical and epicyclic gear stages to handle high torque, while incorporating water-resistant sealing and spherical roller bearings to accommodate the inevitable structural misalignments and flexing of the truck chassis during off-road travel.
TBMs are the giants of construction machinery, boring through solid rock under cities and mountains. The cutterhead drive of a TBM is powered by a ring of multiple planetary gearboxes working in unison. These custom gearboxes must deliver millions of Newton-meters of torque. They are designed with specialized load-sharing systems, internal cooling jackets to dissipate intense friction heat, and real-time sensor ports to monitor vibration, temperature, and oil degradation, ensuring uninterrupted underground operations.
The intersection of digital technology and heavy industry is driving several key trends in custom gearbox design:
HZPT: A Legacy of Growth & Innovation
Our journey is one of continuous evolution and strategic expansion. From our humble beginnings to our current position as a global leader in high-torque power transmission, we have remained dedicated to engineering excellence.
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and establish a solid technical foundation in the power transmission industry.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions, enabling us to serve more complex industrial needs and establish long-term partnerships with major machinery OEMs.
In the era of Industry 4.0, we have fully embraced smart manufacturing. By integrating advanced digital design tools, automated assembly lines, and digital testing rigs, we now deliver next-generation products that are smarter, more compact, and more energy-efficient, solidifying our position as an industry innovator.
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
Quality is the cornerstone of our manufacturing philosophy. We understand that a gearbox failure in the field can be catastrophic, which is why we employ a multi-layered quality control system throughout the production cycle:
Quality is at the heart of everything we do
No diversions—just decades of refining helical, planetary, and parallel-shaft gearboxes for heavy-duty industrial and construction machinery applications.
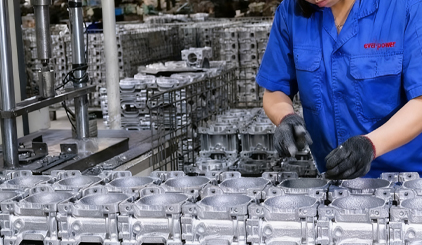
Critical processes like gear grinding, heat treatment, and housing machining are all done under one roof for consistent quality control and shorter lead times.
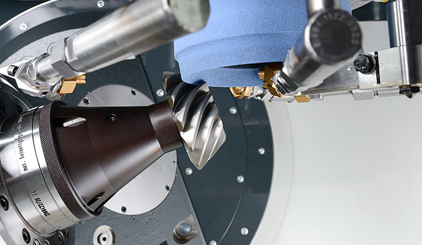
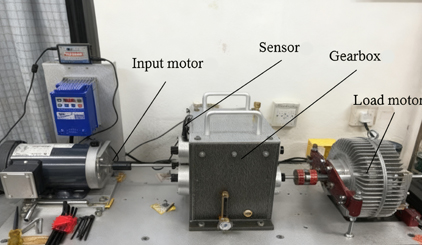
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks—detailed test reports are available on request for complete transparency.
Our experienced engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese—because your uptime matters.
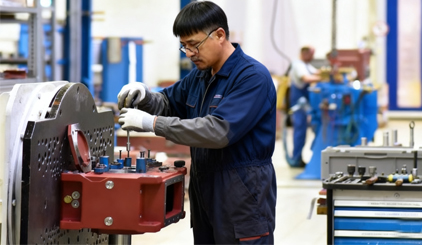
Explore our wide range of high-torque, custom-engineered gearboxes and speed reducers