Leave Your Message
Precision-engineered gearbox solutions purpose-built for demanding environmental and treatment applications.
From irrigation canals to advanced wastewater treatment facilities — the intersection of agriculture and environmental engineering.
Agricultural gearboxes have long been the unsung workhorses of farming operations — powering spreaders, tillers, mowers, and conveyors across millions of hectares worldwide. However, the past decade has witnessed a remarkable convergence: the same robust, corrosion-resistant, and high-torque gearbox technology that drives agricultural machinery is increasingly being deployed in wastewater treatment plants, irrigation water management systems, biogas facilities, and broader environmental protection infrastructure.
Modern wastewater treatment and environmental systems require drive components that can withstand corrosive media, continuous 24/7 operation, variable torque loads, and stringent regulatory requirements around energy efficiency and emissions. Agricultural-grade gearboxes — particularly helical, planetary, and worm gear designs — offer exactly this combination: robust construction, high mechanical efficiency, adaptability to wet and chemically aggressive environments, and cost-effectiveness at scale.
The design philosophy behind agricultural gearboxes prioritizes durability under unpredictable field conditions — muddy, wet, dusty, temperature-varying environments. These same attributes translate directly to the challenges of wastewater plants, where gearboxes must drive aerator agitators, thickener rakes, screw conveyors, belt filter presses, sludge pumps, and irrigation channel gate mechanisms reliably, 24 hours a day, 365 days a year.
Key technical advantages include: sealed IP65/IP67-rated housings that resist ingress of water and contaminants; stainless steel or epoxy-coated surfaces that withstand hydrogen sulfide and other corrosive gases common in wastewater environments; high shock-load tolerance suitable for aeration basin mixers; and flexible mounting configurations (shaft-mounted, foot-mounted, flange-mounted) for integration into diverse infrastructure layouts.
The commercial and industrial landscape shaping the future of gearbox applications in environmental systems.
Governments worldwide are committing trillions to clean water and environmental protection infrastructure. The UN's Sustainable Development Goal 6 — Clean Water and Sanitation — is accelerating new wastewater plant construction in Asia, Africa, and Latin America, creating massive demand for reliable mechanical drive systems including agricultural-type gearboxes for pumping, aeration, and conveyance applications.
Wastewater treatment is one of the most energy-intensive municipal operations — typically consuming 30–40% of a city's energy budget. Modern helical planetary gearboxes achieve transmission efficiencies above 97%, compared to 85–90% for older worm gear designs. Regulators in the EU, North America, and increasingly in China are mandating IE3/IE4 motor-gearbox packages, driving rapid replacement of legacy drive systems with high-efficiency alternatives.
Industry 4.0 is transforming both gearbox manufacturing and wastewater operations. Sensor-equipped gearboxes with embedded vibration monitoring, temperature sensing, and oil condition analysis enable predictive maintenance in treatment plants — reducing unplanned downtime by up to 45%. Leading manufacturers now offer gearboxes with integrated IIoT connectivity, allowing remote monitoring of critical environmental infrastructure.
The intersection of agriculture and environmental compliance is creating new specialized markets. Large-scale livestock farms, food processing facilities, and agricultural cooperatives are required to treat their effluent before discharge. Biogas digesters, slurry agitators, compost turning equipment, and constructed wetland pumping systems all rely on heavy-duty agricultural gearboxes — driving strong commercial growth in this specialized niche.
As treatment plants are built in increasingly space-constrained urban and peri-urban environments, demand is growing for compact, high-torque-density gearbox solutions. Planetary and cycloidal designs are gaining ground over traditional parallel-shaft reducers due to their power-to-weight ratio and coaxial configurations — both key advantages in retrofit applications where existing infrastructure limits available installation space.
Southeast Asia, Sub-Saharan Africa, and South America represent the fastest-growing markets for both agricultural mechanization and wastewater infrastructure. International development banks (World Bank, ADB, AfDB) are funding large-scale water treatment projects that specify high-quality, internationally-certified mechanical drive equipment — presenting significant commercial opportunities for established gearbox manufacturers with proven quality management systems.
Specific industrial use cases where agricultural gearboxes deliver proven performance in environmental systems.
Surface aerators, submersible agitators, and horizontal rotor aerators in activated sludge basins represent one of the most demanding gearbox applications in wastewater treatment. Gearboxes must transmit continuous high torque while submerged or splash-exposed, resisting biologically active, H₂S-laden environments. Heavy-duty helical bevel gearboxes with stainless steel shafts and double-lip seals are the standard solution, operating for 80,000+ hours between major overhauls.
Gravity thickeners and secondary clarifiers use slow-speed, high-torque rake mechanisms to concentrate sludge at the bottom of circular tanks. These applications demand gearboxes with extremely high torque multiplication (reduction ratios of 200:1 to 1,000:1), robust overload protection, and the ability to withstand sudden torque spikes when rakes encounter dense sludge blankets. Cycloidal and planetary gearboxes are particularly well-suited for this critical environmental role.
Large-scale irrigation canal gate operators, water distribution pumping stations, and flood control infrastructure require reliable, weather-resistant gearboxes for sluice gate actuation, pump speed control, and channel flow regulation. Screw jack gearboxes and worm gear reducers power gate lifting mechanisms that protect both agricultural land and surrounding ecosystems from flooding — a direct intersection of agricultural and environmental management.
Anaerobic digesters processing agricultural waste, food industry effluent, and municipal sludge require slow-speed agitator drives capable of working in sealed, methane-atmosphere vessels under elevated pressure and temperature. ATEX/IECEx-certified gearboxes with explosion-proof sealing are essential for safety. These systems convert waste into renewable energy, with gearbox reliability directly impacting biogas yield and plant profitability.
Mechanical sludge dewatering — the final step before sludge disposal or reuse as agricultural fertilizer — relies on belt filter presses and screw press dewatering machines powered by precision gearboxes. These applications require accurate speed control, high radial load capacity, and resistance to the chemically aggressive environment of conditioned sludge. Compact helical inline gearboxes with variable frequency drive (VFD) compatibility are the industry standard.
Agricultural composting facilities and organic waste processing plants use rotary drum composters, windrow turners, and conveyor systems that all rely on heavy-duty agricultural gearboxes for material handling and processing. The abrasive, high-moisture, high-temperature environment of composting operations demands the same corrosion resistance and reliability characteristics as wastewater treatment — making agricultural gearbox technology directly transferable to this growing environmental sector.
A Legacy of Growth & Innovation
Our journey is one of continuous evolution and strategic expansion — building world-class gearbox manufacturing capability over more than two decades.
Established in 2002, we began with a clear mission: to produce gearboxes of unmatched quality and durability. Our initial focus on standardized models allowed us to build a reputation for reliability and establish a solid technical foundation that continues to underpin everything we do today.
Responding to market demands, we significantly expanded our production capabilities and R&D efforts. This period saw the introduction of custom-engineered and application-specific solutions — including gearboxes for wastewater treatment and environmental systems — enabling us to serve more complex industrial needs and establish long-term global partnerships.
In the era of Industry 4.0, we have embraced smart manufacturing. By integrating advanced digital design tools, automated CNC machining centers, and IoT-enabled quality monitoring, we now deliver next-generation products that are smarter, more compact, and more energy-efficient — solidifying our position as an industry innovator for environmental and agricultural drive solutions globally.
We invest in world-class technology to ensure every product that leaves our facility is built to excel.
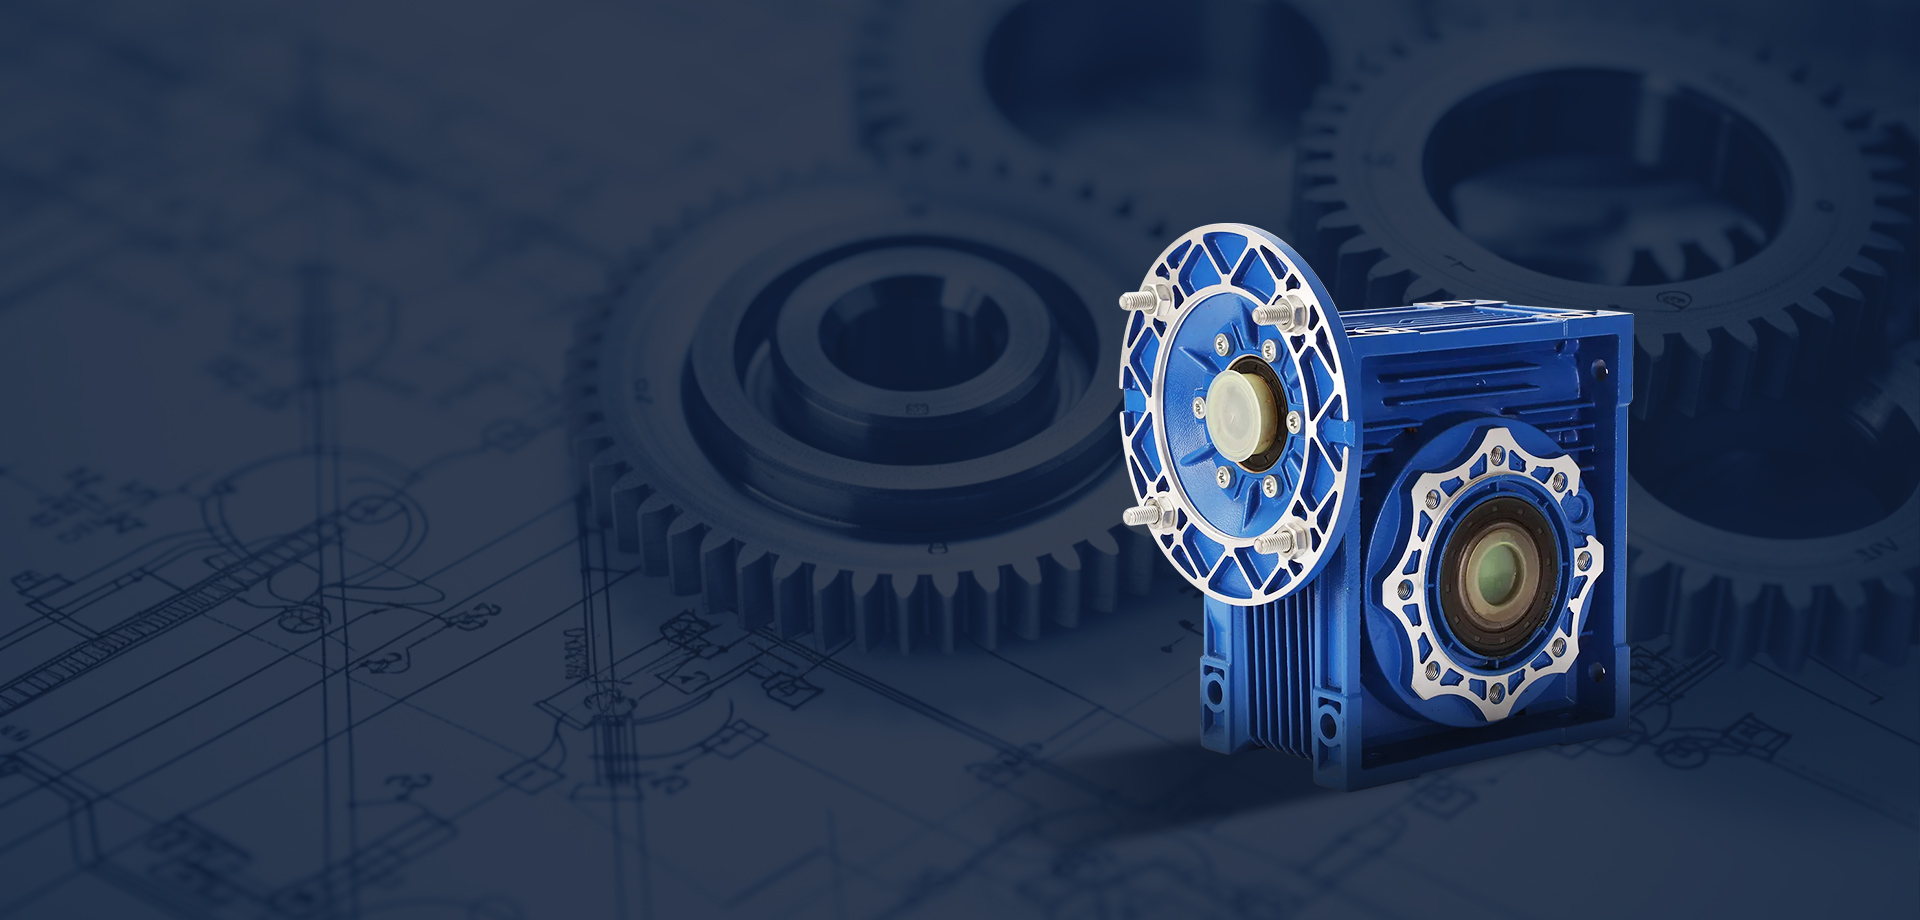
Quality is at the heart of everything we do — from raw material selection to after-sales technical support.
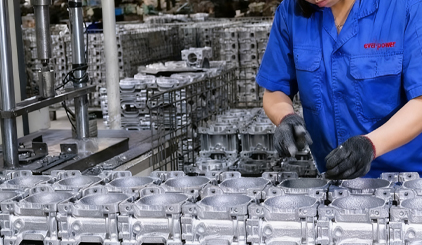
No diversions — just decades of refining helical, planetary, and parallel-shaft gearboxes for industrial applications including wastewater treatment and environmental systems.
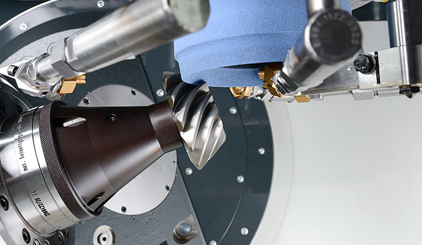
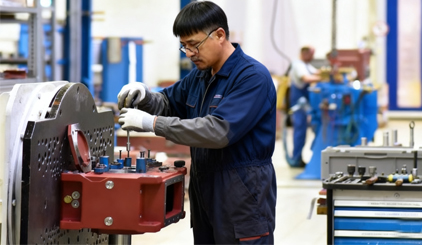
Critical processes like gear grinding, heat treatment, and housing machining are all done under one roof for consistent quality and faster lead times.
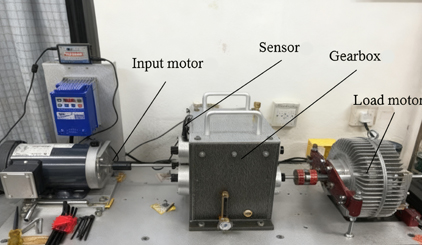
100% factory acceptance testing at rated torque with vibration, temperature, and leakage checks — test reports available on request for compliance documentation.
Our engineers provide prompt troubleshooting, installation advice, and maintenance recommendations in English or Chinese — because your uptime matters.
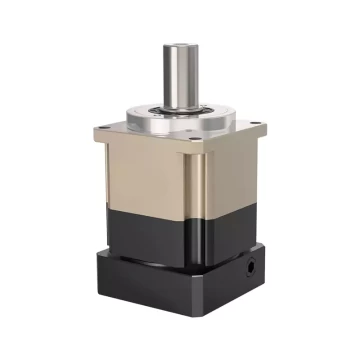
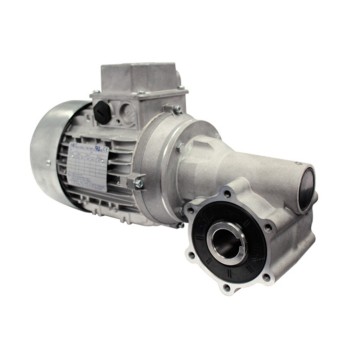
Explore our full range of industrial gearbox products engineered for wastewater treatment, environmental protection, and agricultural drive applications.
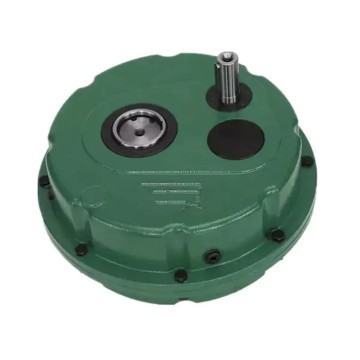
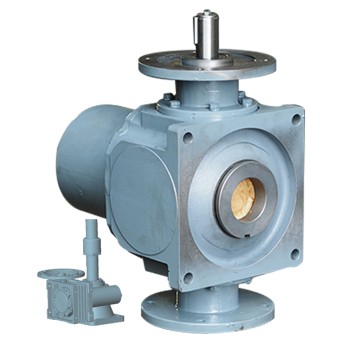
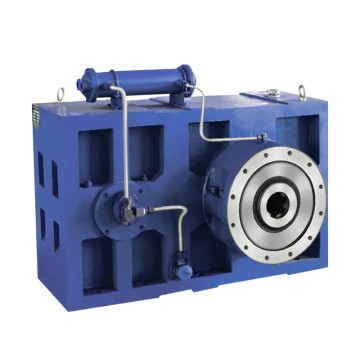
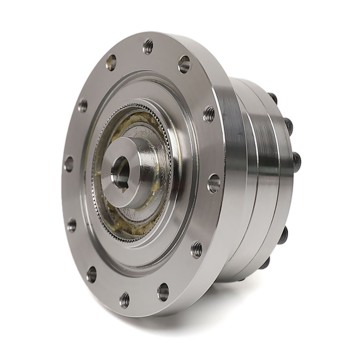
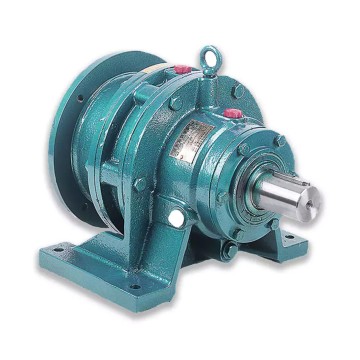
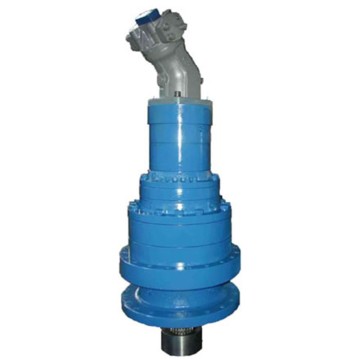
Contact our engineering team today for a customized gearbox solution tailored to your wastewater treatment or environmental system requirements.
Explore All Products →