Leave Your Message
Precision-engineered gearboxes built for demanding conveyor systems and agricultural material handling applications
An agricultural gearbox for conveyor systems and material handling is a specialized power transmission device engineered to transfer, reduce, and regulate rotational force from a motor to the mechanical components that move bulk agricultural materials — including grain, seeds, fertilizer, silage, compost, and harvested crops — across processing, storage, and distribution facilities.
Unlike standard industrial gearboxes, agricultural conveyor gearboxes are designed to withstand the unique operational demands of agri-environments: exposure to dust, moisture, organic debris, temperature fluctuations, and continuous heavy-load cycling. These units must deliver consistent torque output, low-noise operation, and extended service life with minimal maintenance intervention.
From horizontal belt conveyors and bucket elevators to screw augers and chain conveyors, every material handling line depends on a precisely matched gearbox to ensure smooth, reliable, and energy-efficient operation throughout the entire agricultural supply chain.
Trusted globally for agricultural and industrial gearbox excellence
The global agricultural gearbox market for conveyor and material handling is experiencing robust growth
The global market for agricultural gearboxes used in conveyor systems and material handling is projected to surpass USD 3.8 billion by 2030, driven by accelerating mechanization of farming operations, expansion of large-scale grain storage infrastructure, and the growing adoption of automated post-harvest processing lines across Asia-Pacific, North America, and Europe.
Key market drivers include:
Leading industrial economies are investing heavily in modernizing their agricultural supply chains, creating sustained demand for high-performance, long-life gearbox solutions that can operate continuously under heavy-load conditions.
The agricultural gearbox sector for conveyor applications is undergoing significant technological transformation, driven by four major trends:
How agricultural gearboxes power every stage of the conveyor and material handling chain
Grain elevators represent one of the most demanding applications for agricultural gearboxes. The gearbox must deliver high starting torque to overcome the inertia of fully-loaded buckets while maintaining stable speed under variable loads. HZPT's helical and planetary gearboxes provide the precise torque multiplication needed for bucket elevator drives handling wheat, corn, soybeans, and rice — with output torques ranging from 500 Nm to over 50,000 Nm depending on elevator capacity.
Key requirements: high shock-load resistance, IP65+ sealing against grain dust, continuous duty rating, and compatibility with variable frequency drives (VFDs) for soft-start operation.
Read More
In animal feed production facilities, screw conveyors and augers transport raw ingredients — including corn meal, soybean meal, fishmeal, and mineral premixes — between mixing, pelleting, and bagging stations. The gearbox must handle abrasive materials while maintaining precise speed ratios to ensure consistent feed formulation.
Worm gearboxes and helical-bevel units are widely deployed in feed mill conveyor applications due to their compact footprint, high reduction ratios (up to 100:1 in single stage), and ability to mount in multiple orientations to suit facility layouts. Stainless steel variants are available for hygiene-critical zones.
Read More
Modern post-harvest facilities employ multi-stage conveyor systems for cleaning, grading, drying, and packaging agricultural produce. Each conveyor segment requires a precisely matched gearbox to synchronize material flow and prevent bottlenecks. In optical sorting lines for fruits and vegetables, low-backlash planetary gearboxes ensure the precise belt speed control needed for accurate camera-based sorting at rates exceeding 10 tonnes per hour.
Variable-speed gearbox-motor combinations allow operators to adjust throughput in real time based on crop condition and downstream capacity — a critical capability during peak harvest periods when processing efficiency directly impacts profitability.
Read More
Large-scale agricultural commodity ports — handling millions of tonnes of grain, sugar, fertilizer, and oilseeds annually — rely on massive conveyor networks powered by heavy-duty gearboxes. Ship loaders, unloaders, stacker-reclaimers, and transfer towers all require gearboxes capable of delivering sustained high torque under continuous operation, often in marine environments with high humidity and salt exposure.
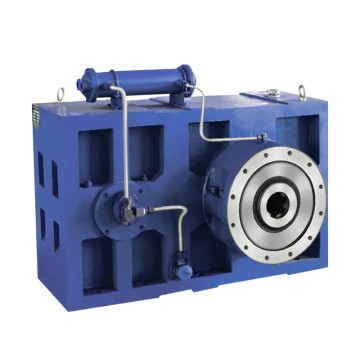
For these applications, HZPT supplies large-frame helical and planetary gearboxes with output torques exceeding 200,000 Nm, featuring advanced sealing systems, forced lubrication circuits, and integrated thermal management to ensure reliability in 24/7 port operations.
Read MoreEngineering excellence designed specifically for agricultural material handling demands
HANGZHOU EVER-POWER TRANSMISSION CO., LTD. (HZPT) is a leading manufacturer and global supplier of high-performance gearboxes, specializing in the design, development, and production of industrial and agricultural transmission systems. With over 15 years of experience in the power transmission industry, HZPT has grown into a modern enterprise integrating R&D, manufacturing, sales, and service, serving customers in more than 60 countries across Asia, Europe, North America, and Africa.
Our manufacturing base spans over 80,000 square meters, equipped with advanced CNC machining centers, precision gear grinding machines, automated assembly lines, and state-of-the-art testing facilities. We operate a fully integrated production system that ensures consistent quality from raw material sourcing to final product delivery.
For conveyor system integrators, agricultural machinery OEMs, and material handling engineers, HZPT offers comprehensive technical support — from initial application analysis and gear selection through to custom engineering, prototype validation, and after-sales service — ensuring your conveyor system performs at peak efficiency throughout its operational life.
DISCOVER OUR SUSTAINABILITY PROJECTSEngineering guidance for material handling system designers and agricultural equipment specifiers
Selecting the optimal gearbox type for an agricultural conveyor or material handling system requires careful analysis of the application's torque requirements, speed range, duty cycle, environmental conditions, and physical installation constraints. The four primary gearbox types used in agricultural conveyor applications each offer distinct advantages:
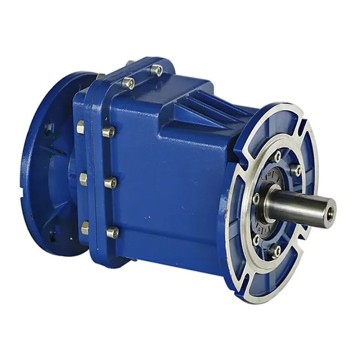
Helical gearboxes are the workhorse of agricultural conveyor systems, offering smooth, quiet operation with high efficiency. The helical tooth profile distributes load across multiple teeth simultaneously, resulting in lower noise levels and higher load capacity compared to spur gears. RC Series helical gearboxes are widely used in horizontal belt conveyors, chain conveyors, and slat conveyors handling grain, fertilizer, and processed agricultural products.
Key advantages for conveyor applications: high efficiency (96-98%), wide torque range, low operating noise suitable for indoor feed mills and processing facilities, and compatibility with direct motor coupling or belt-drive input.
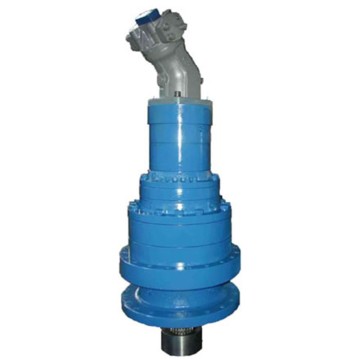
Planetary gearboxes deliver exceptional power density — achieving high torque output in a compact, concentric form factor ideal for space-constrained conveyor drive installations. In agricultural material handling, planetary units are preferred for high-torque, low-speed applications such as heavy-duty bucket elevator drives, paddle mixer conveyors, and large-diameter screw conveyors handling dense materials like wet grain or mineral fertilizers.
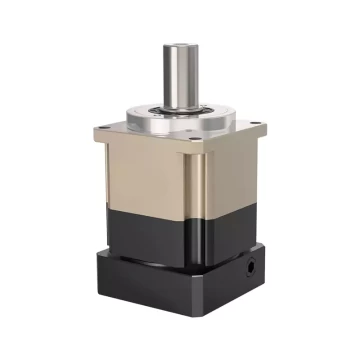
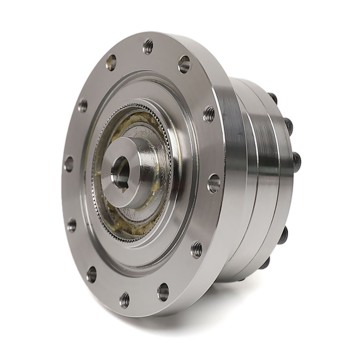
The TM042 Series high-precision planetary gearbox is particularly valued in automated sorting and processing conveyor lines where precise speed control and minimal backlash are essential for product quality and system synchronization.
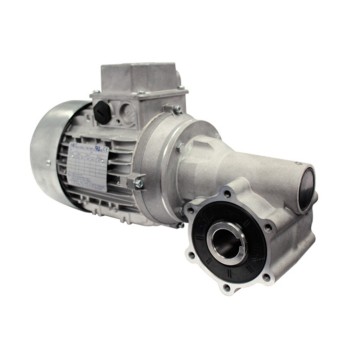
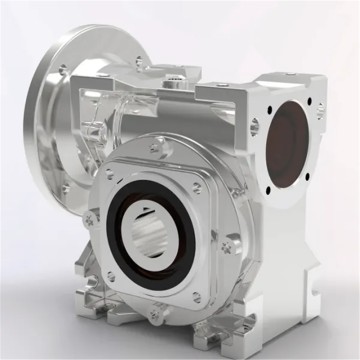
Worm gearboxes provide high reduction ratios in a single stage, self-locking capability (preventing back-driving), and right-angle power transmission — making them ideal for vertical screw conveyors, inclined auger systems, and agricultural elevator drives where load holding is required during motor-off conditions. The SSRV Series stainless steel worm gearboxes are specifically engineered for food-processing conveyor applications where hygiene standards demand corrosion-resistant housings and food-grade lubrication.
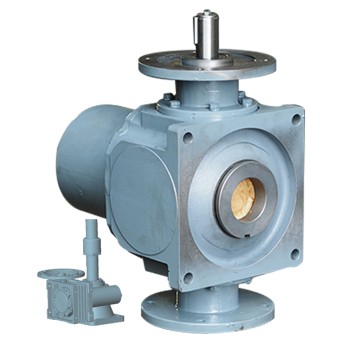
For applications requiring right-angle power transmission with higher efficiency than standard worm gears, helical-bevel gearboxes offer an optimal solution. These units combine the efficiency of helical gearing with the compact right-angle output of bevel gears, achieving efficiencies of 94-96% — significantly better than worm gearboxes in high-power conveyor applications. They are commonly specified for large-scale grain dryer conveyors, seed processing lines, and fertilizer blending conveyor systems.
Agricultural conveyor systems frequently experience shock loading — particularly during startup with a fully-loaded conveyor, or when handling materials with variable density and flow characteristics. Gearbox selection must account for an appropriate service factor (typically 1.5 to 2.5 for agricultural applications) to ensure the unit's rated torque capacity is not exceeded during peak load events. Thermal rating is equally important: continuous duty conveyor drives generate heat that must be dissipated through the gearbox housing, and thermal derating must be applied in high-ambient-temperature environments such as grain dryer facilities.
Conveyor drives impose significant radial loads on the gearbox output shaft, particularly in chain conveyor and belt conveyor applications where the drive sprocket or pulley is mounted directly on the output shaft. Gearboxes specified for conveyor applications must have adequate output shaft bearing capacity to handle these combined radial and axial loads over the required service life — typically 25,000 to 50,000 hours for agricultural processing facilities operating multiple shifts per day.
In agricultural environments, gearbox lubrication management is critical. Dust contamination, temperature cycling, and moisture ingress accelerate lubricant degradation. HZPT's agricultural conveyor gearboxes are factory-filled with premium synthetic gear oil and feature oil-level sight glasses, drain plugs, and breather vents designed to simplify field maintenance. Extended oil change intervals of 10,000+ hours are achievable with synthetic lubricants in properly sealed units — a significant operational advantage in remote agricultural facilities.
Contemporary agricultural conveyor systems increasingly employ variable frequency drives (VFDs) and programmable logic controllers (PLCs) to optimize material flow, reduce energy consumption, and enable automated operation. HZPT's gearboxes are fully compatible with VFD operation, with motor flange options (IEC B5/B14) that facilitate direct mounting of inverter-duty motors. The smooth torque characteristics of helical and planetary gearboxes make them ideal for VFD-controlled soft-start applications, eliminating mechanical shock during conveyor startup and significantly extending the service life of belts, chains, and structural components.
For smart conveyor systems incorporating condition monitoring, HZPT can supply gearboxes with integrated vibration monitoring ports and temperature sensor bosses, enabling facility managers to track gearbox health in real time and schedule preventive maintenance during planned downtime — rather than responding reactively to unexpected failures during critical harvest operations.
Explore our complete range of precision gearboxes for conveyor, material handling, and beyond